

Principles and Working Scene Characteristics of Aggregate Powder Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced aggregate powder conveying systems. These systems are engineered to efficiently transport bulk materials such as aggregates, powders, and granules, playing a critical role in various industrial applications. This article explores the fundamental principles behind these systems and highlights the key working scene characteristics that define their operational effectiveness.
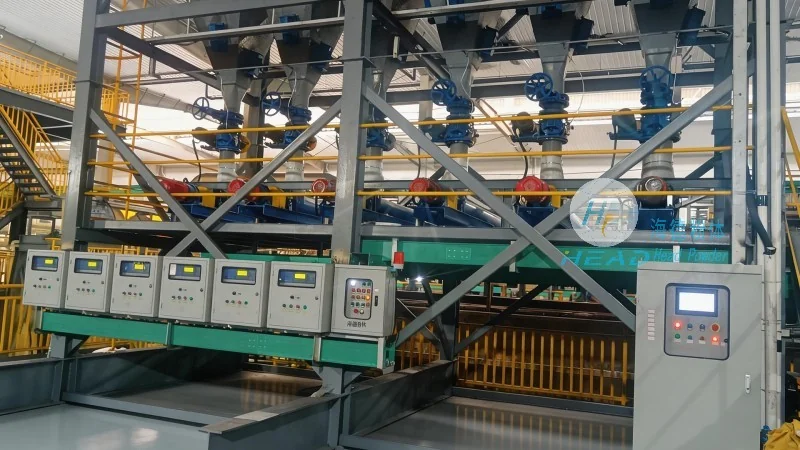
Understanding the Core Principles of Aggregate Powder Conveying Systems
The operation of aggregate powder conveying systems is grounded in several key principles that ensure reliable and efficient material transport. At the heart of these systems is the ability to handle diverse materials with varying properties, including different particle sizes, densities, and flow characteristics. The primary goal is to move bulk materials from a source to a destination without degradation or loss, while maintaining consistent flow rates and minimizing energy consumption.
One of the fundamental principles is the use of specialized equipment designed to handle the unique challenges of powder and granular materials. This includes components such as feeders, conveyors, and control systems that are engineered to prevent issues like blockages, segregation, and material degradation. The systems often incorporate features like variable speed drives, which allow for precise control over the flow rate, ensuring optimal performance under different operational conditions.
Key Working Scene Characteristics of Aggregate Powder Conveying Systems
The effectiveness of aggregate powder conveying systems is heavily influenced by the specific working scene characteristics in which they are deployed. These characteristics include the nature of the material being conveyed, the distance and elevation changes between the source and destination, and the required throughput capacity. Each of these factors plays a critical role in determining the most suitable system configuration and operational parameters.
For instance, in construction and mining applications, where large volumes of aggregates are needed for concrete production and other building materials, the system must be capable of handling high throughput rates. The working scene may involve long distances and significant vertical lifts, requiring robust conveyor designs with high power ratings and durable components to withstand heavy usage and harsh environmental conditions.
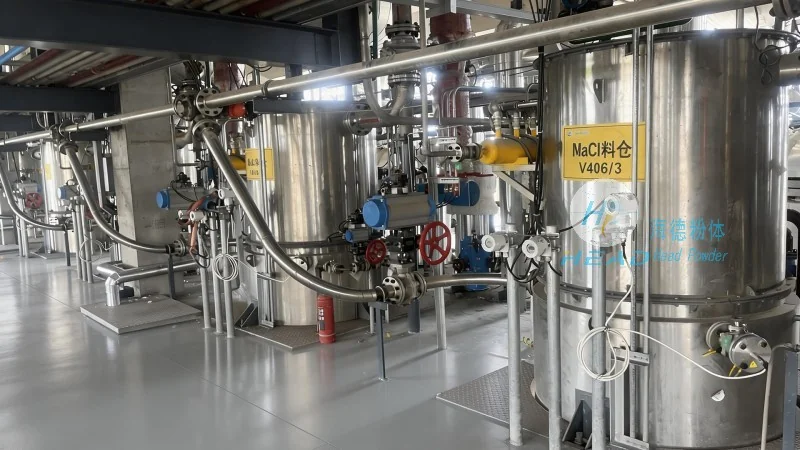
In contrast, applications in pharmaceutical or food processing industries demand a higher level of precision and cleanliness. The working scene here emphasizes the need for systems that prevent contamination, maintain material integrity, and comply with stringent regulatory standards. This often involves the use of enclosed, dust-tight conveyors and advanced control systems that ensure consistent and hygienic material handling.
Applications and Industry Integration
Aggregate powder conveying systems are widely integrated into various industries, each with distinct operational requirements. In the construction sector, these systems are essential for transporting raw materials like sand, gravel, and cement to construction sites, ensuring a steady supply for concrete mixing and other processes. The working scene in this industry typically involves large-scale operations with high material volumes and the need for reliable, continuous operation.
In the mining industry, the systems play a vital role in transporting ore and other minerals from extraction sites to processing facilities. The working scene here may involve challenging terrain and variable material compositions, requiring systems that can adapt to changing conditions and maintain consistent performance. The ability to handle abrasive materials and resist wear is crucial in these applications.
In the chemical and petrochemical industries, the systems are used to transport various powders and granules, such as raw materials for chemical synthesis or catalysts. The working scene in this sector emphasizes safety and efficiency, with systems designed to prevent dust explosions and ensure precise material control. Advanced monitoring and control technologies are often integrated to optimize performance and ensure compliance with safety regulations.
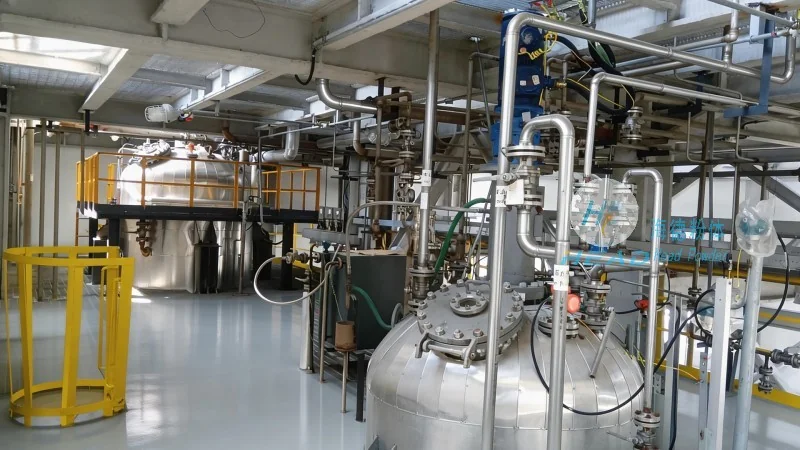
Advantages and Operational Benefits
The adoption of aggregate powder conveying systems offers numerous advantages that enhance operational efficiency and productivity. One of the primary benefits is the reduction in labor costs associated with manual material handling, as these systems can operate continuously with minimal human intervention. This not only improves safety by reducing the risk of accidents but also increases overall throughput.
Another significant advantage is the improvement in material quality and consistency. By eliminating manual handling, the systems minimize the risk of material segregation and degradation, ensuring that the transported materials meet the required specifications. This is particularly important in industries where material quality directly impacts product performance, such as in pharmaceuticals or food processing.
Energy efficiency is also a key consideration in modern conveying systems. Advanced designs incorporate energy-saving features, such as variable speed drives and optimized conveyor layouts, which reduce energy consumption while maintaining performance. This not only lowers operational costs but also contributes to environmental sustainability by minimizing the carbon footprint of material transport operations.
Conclusion
Aggregate powder conveying systems, as developed and implemented by HeadPowder, represent a sophisticated solution for efficient bulk material transport. By understanding the core principles and working scene characteristics, industries can select and operate these systems to meet their specific needs, ensuring reliable performance, high efficiency, and cost-effectiveness. The continued advancement of technology in this field ensures that these systems will remain a critical component in the future of industrial material handling.