

Principle and Working Scene Characteristics of Coal Sand Pneumatic Conveying Equipment
HeadPowder, officially known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer headquartered in Shandong, China. The company specializes in the design, development, and production of advanced pneumatic conveying systems, with a particular focus on equipment used for transporting coal and sand. HeadPowder has built a strong reputation in the material handling industry by delivering high-quality, reliable solutions that meet the unique demands of industrial applications. The company's commitment to innovation and customer-centric approaches has enabled it to serve a wide range of clients across various sectors.
Principle of Pneumatic Conveying Equipment
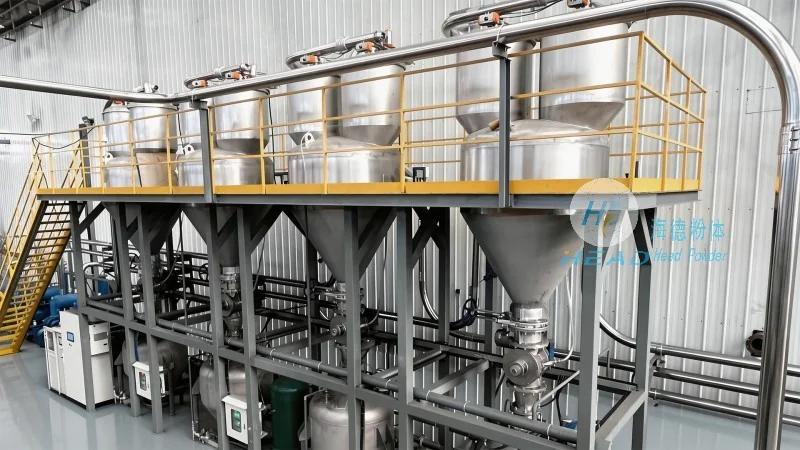
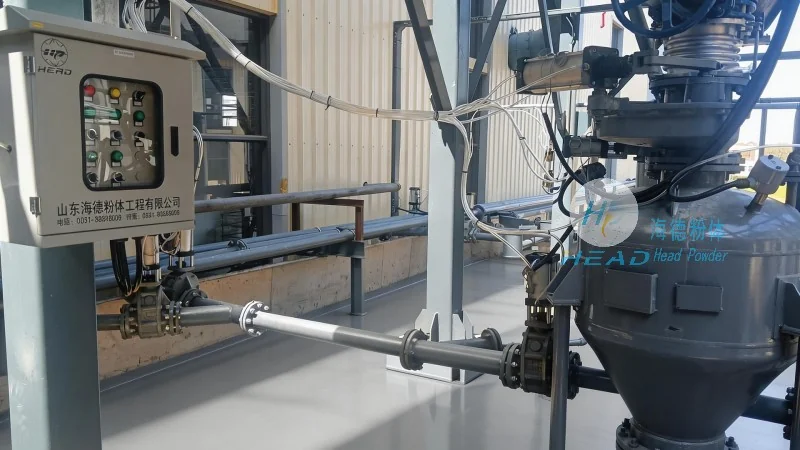
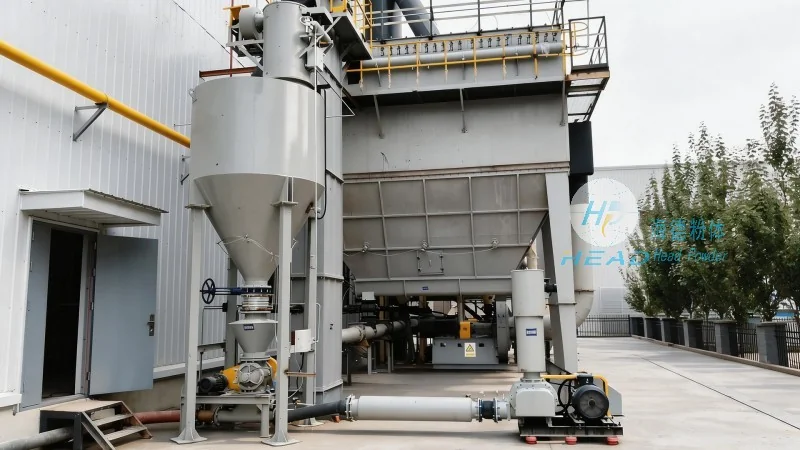
The fundamental principle of coal sand pneumatic conveying equipment is the utilization of air as a transport medium to move solid particles. The system operates by feeding coal or sand into a hopper, where a blower generates a high-pressure airflow. This airflow lifts and propels the particles through a pipeline network, delivering them to a receiver or processing unit. The process relies on the kinetic energy of the air to overcome the gravitational force acting on the solid material. Key components include the hopper for material storage, the blower for air generation, the pipeline system for material transport, and the receiver for final discharge. The design ensures efficient and continuous material transfer, with the ability to handle diverse particle sizes, moisture levels, and bulk densities typical of coal and sand. The system can operate under positive or negative pressure, depending on the specific application requirements, providing flexibility in material handling.
Working Scene Characteristics
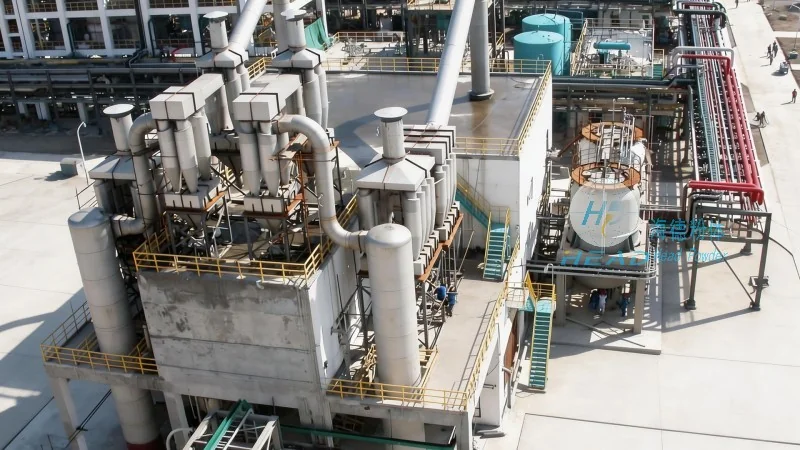
The working scene characteristics of coal sand pneumatic conveying equipment are closely aligned with the operational needs of industrial environments where coal and sand are processed. These systems are commonly employed in coal mines, thermal power plants, and construction material processing facilities. The equipment is engineered to operate in challenging conditions, such as high dust levels and varying ambient temperatures, with features like dust suppression and noise reduction to ensure safe and efficient operation. The flexibility of the system allows it to handle both short-distance and long-distance conveying tasks, adapting to different plant layouts and spatial constraints. Additionally, the equipment is built for durability and low maintenance, with robust components that can withstand the abrasive nature of coal and sand particles. The working scene also emphasizes operational efficiency, with integrated controls and monitoring systems that optimize airflow and material flow, reducing downtime and enhancing productivity. Safety is a top priority, with features like emergency shut-off valves and pressure relief mechanisms to prevent accidents and protect personnel.