

Working Principle and Features of Cement Dry Ash Powder Conveying System Equipment
Efficient and reliable transportation of cement dry ash powder is crucial in modern industrial applications, particularly in the construction and cement manufacturing sectors. The cement dry ash powder conveying system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., offers advanced solutions to meet these demands, ensuring optimal performance and safety in powder handling processes.
Working Principle of the Cement Dry Ash Powder Conveying System
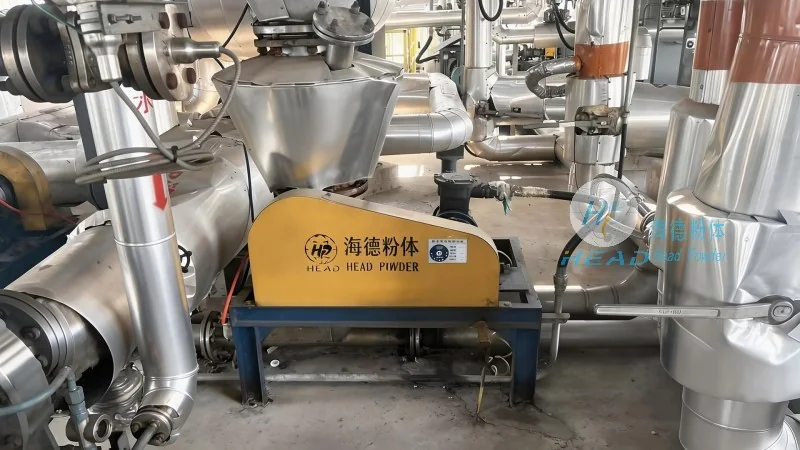
The working principle of the cement dry ash powder conveying system involves a series of coordinated steps to ensure the efficient movement of dry ash powder from the source to the destination. The process begins with the material being drawn from a storage silo or hopper by a feeding device, such as a rotary valve or a screw feeder. This initial step ensures a consistent and controlled supply of the powder into the system. The material then enters a conveyor section, which can be either pneumatic or mechanical. In pneumatic systems, the conveyor utilizes compressed air or a vacuum to create a pressure differential that propels the powder through the pipeline. The air flow is carefully regulated to maintain the desired velocity and prevent material deposition or blockages. In mechanical systems, such as screw or belt conveyors, rotating components push the powder along the pipeline, ensuring a continuous flow. The system also includes a series of control valves and sensors that monitor the flow rate, pressure, and temperature of the material. These components allow operators to adjust the system parameters in real-time, optimizing performance and preventing issues like overloading or underflow. The control panel provides a user-friendly interface for monitoring and managing the entire conveying process, enhancing operational efficiency and reducing the risk of human error. This integrated approach ensures that the cement dry ash powder is transported safely and efficiently, minimizing material loss and downtime.
Key Features and Advantages of the System
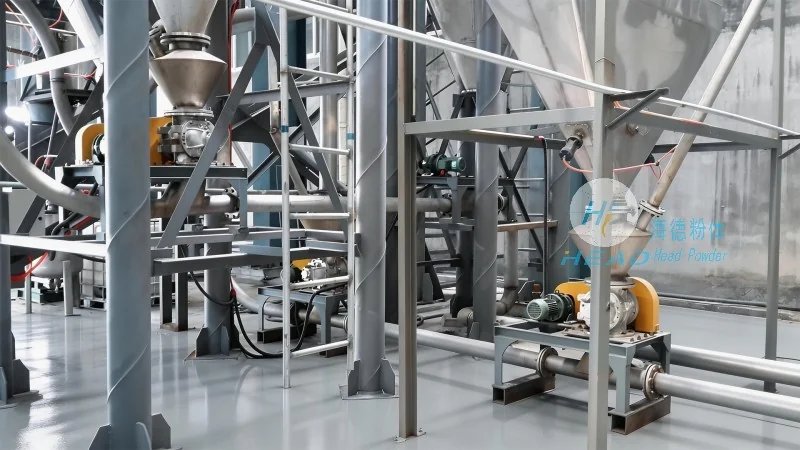
Key features of the cement dry ash powder conveying system include its high capacity and ability to handle fine powders without caking or segregation. The system incorporates advanced anti-caking mechanisms, such as agitators and vibrators, which maintain the powder's flowability by breaking up agglomerates and preventing clumping. This is particularly important for cement dry ash, which is prone to forming hard lumps under certain conditions. The adjustable speed and pressure controls allow operators to adapt the system to different material characteristics, ensuring consistent performance regardless of particle size or moisture content. Another notable feature is the system's energy efficiency, which reduces operational costs by minimizing the use of compressed air or power. The use of energy-saving components, such as variable frequency drives (VFDs), optimizes power consumption while maintaining the required flow rate. The system also features explosion-proof design elements, including flame arrestors and pressure relief valves, to comply with safety regulations and prevent accidents in hazardous environments. The compact and modular design of the equipment allows for easy installation and maintenance, with components that can be easily accessed and serviced. This reduces downtime and maintenance costs, making the system a cost-effective solution for long-term use. The durability of the system is enhanced by the use of high-quality materials, such as stainless steel and corrosion-resistant alloys, which resist wear and tear from abrasive powders. This ensures that the equipment has a long service life and requires minimal repairs or replacements over time.
About Shandong HeadPowder Engineering Co., Ltd.
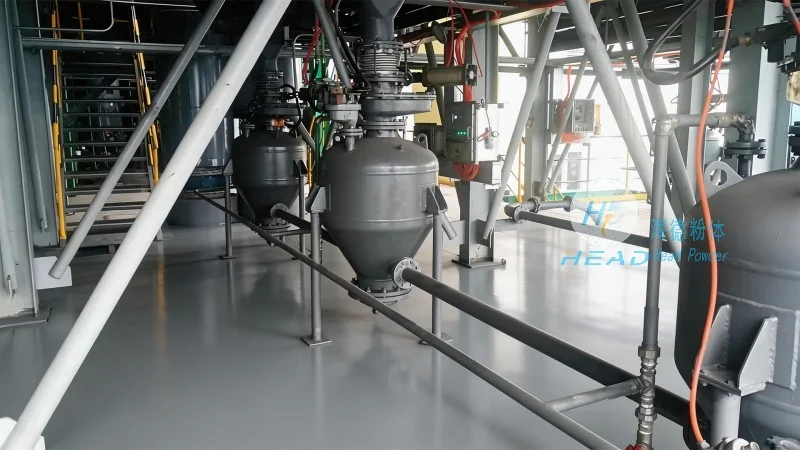
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer and supplier of specialized powder handling equipment, with a strong presence in the Chinese market. The company is headquartered in Shandong, China, and has established itself as a trusted partner for industries requiring reliable and efficient powder transport solutions. With years of experience in the field, HeadPowder has developed a comprehensive range of products tailored to meet the unique needs of various sectors, including cement, mining, and chemical industries. The company's commitment to innovation and quality has earned it a reputation for delivering high-performance equipment that meets international standards. By focusing on customer satisfaction and technological advancement, HeadPowder continues to provide cutting-edge solutions that enhance operational efficiency and safety in powder handling processes. The company's team of experts provides technical support and after-sales service to ensure that clients receive the best possible support throughout the lifecycle of their equipment. HeadPowder's dedication to research and development ensures that its products remain at the forefront of technology, offering solutions that address the evolving challenges of modern industrial applications. The company's customer-centric approach and strong technical expertise have made it a preferred choice for businesses seeking reliable and efficient powder handling systems.