

Working Principle and Characteristics of Straw Ash Powder Conveying
Straw ash powder conveying is a critical process in the handling and transportation of agricultural waste-derived materials. Understanding its working principle and key characteristics is essential for optimizing operations in industries such as biomass energy, environmental remediation, and agricultural processing. This article provides a detailed overview of how straw ash powder is conveyed, its operational mechanisms, and the advantages that make it a preferred solution for various applications.
Working Principle of Straw Ash Powder Conveying
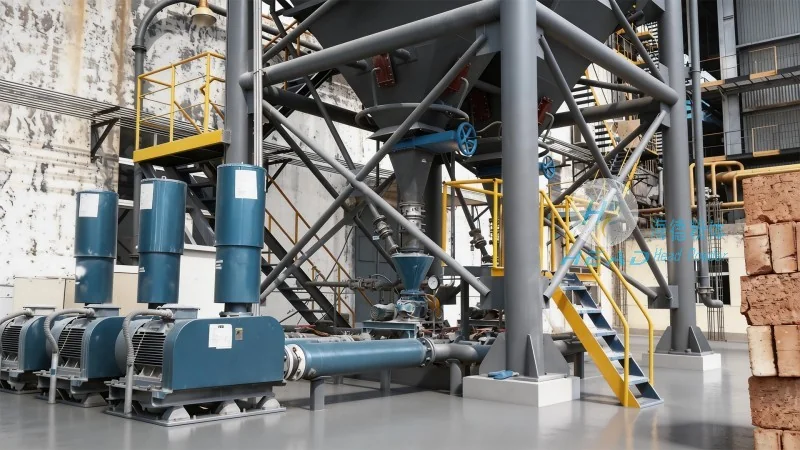
The working principle of straw ash powder conveying typically involves the use of specialized equipment designed to transport fine particulate materials like straw ash. The primary method is often pneumatic conveying, which utilizes air pressure to move the powder through a network of pipes. In this system, a fan or blower generates airflow that draws the straw ash powder into a hopper or collection point. The powder is then entrained by the air stream and transported to the destination point, such as a storage silo or processing unit. This process eliminates the need for mechanical components like belts or buckets, reducing friction and wear while ensuring a continuous flow of material.
Another common method is mechanical conveying, which may involve screw conveyors or belt systems for larger particle sizes or bulkier materials. However, for fine straw ash powders, pneumatic systems are generally more efficient due to their ability to handle low concentrations of material and minimize dust dispersion. The conveying system is typically equipped with control valves, filters, and dust collection units to maintain air quality and prevent environmental contamination. By integrating these components, the system ensures a stable and reliable operation, adapting to varying material flow rates and process demands.
Key Characteristics of Straw Ash Powder Conveying Systems
Straw ash powder conveying systems exhibit several distinct characteristics that make them suitable for diverse industrial applications. One of the most notable features is their high efficiency in material transport. Pneumatic conveying systems can move large volumes of fine powder over long distances with minimal energy consumption, compared to traditional mechanical methods. This efficiency is particularly valuable in large-scale operations where continuous material handling is required.

Environmental friendliness is another critical characteristic. Modern conveying systems are designed with dust suppression and filtration technologies to minimize air pollution and comply with environmental regulations. The use of enclosed pipelines and advanced filtration systems ensures that the powder is contained during transport, reducing the risk of airborne dust and protecting both personnel and the environment. This feature is especially important in regions with strict air quality standards, making straw ash powder conveying an environmentally responsible choice.
Operational safety is a key consideration in straw ash powder handling. The enclosed nature of pneumatic conveying systems prevents direct exposure to the powder, reducing the risk of respiratory issues or skin irritation associated with fine particulate materials. Additionally, the systems are equipped with safety sensors and emergency shut-off mechanisms to prevent accidents during operation. These safety features make the process secure for workers and ensure smooth, uninterrupted production.
Flexibility in system design is also a significant characteristic. Straw ash powder conveying systems can be customized to meet specific operational requirements, including varying material flow rates, pipe lengths, and destination points. The modular design allows for easy integration with existing processing facilities, minimizing downtime and installation costs. This adaptability makes the systems suitable for both new and retrofit applications, providing a versatile solution for different industrial needs.
About Shandong HeadPowder Engineering Co., Ltd.
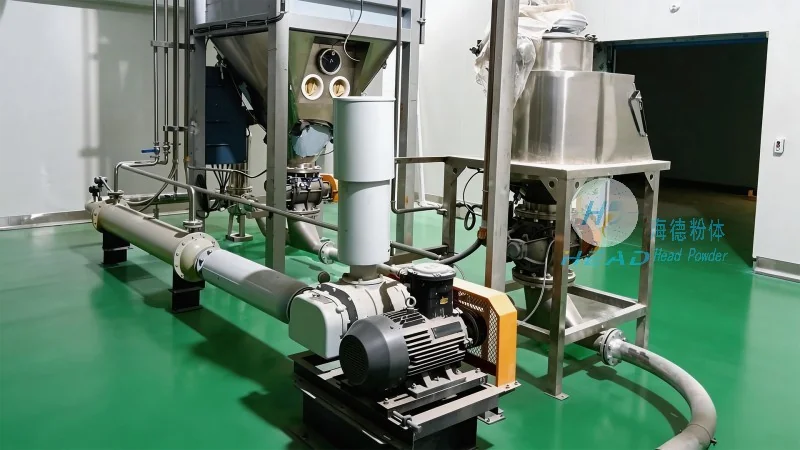
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of advanced powder handling solutions. With a focus on innovation and customer satisfaction, the company specializes in designing and manufacturing efficient conveying systems for various industrial applications. Headpowder's expertise lies in understanding the unique challenges of handling fine particulate materials like straw ash and developing tailored solutions that enhance operational efficiency and safety.
Headpowder's team of engineers and technicians work closely with clients to assess their specific needs and develop customized conveying systems. The company's products are engineered to meet international standards for quality and performance, ensuring reliable operation and long-term durability. With a commitment to sustainability and environmental responsibility, Headpowder integrates eco-friendly technologies into its systems, aligning with global trends in industrial efficiency and environmental protection.
Headquartered in Shandong, China, HeadPowder Engineering Co., Ltd. leverages its local expertise and resources to serve clients worldwide. The company's extensive experience in the field of powder handling has enabled it to develop a comprehensive portfolio of solutions, covering everything from basic conveying systems to complex, integrated processing facilities. By combining technical excellence with customer-centric service, Headpowder continues to be a trusted partner for industries seeking reliable and efficient straw ash powder conveying solutions.