

Working Principle and Features of Multi-Hopper Pneumatic Conveying Equipment
Multi-hopper pneumatic conveying equipment is a sophisticated system designed to efficiently transport bulk materials over extended distances with minimal manual intervention. This technology is integral to modern material handling operations across industries such as chemical processing, food manufacturing, and pharmaceutical production, offering advantages like enhanced cleanliness, reduced labor costs, and improved material integrity.
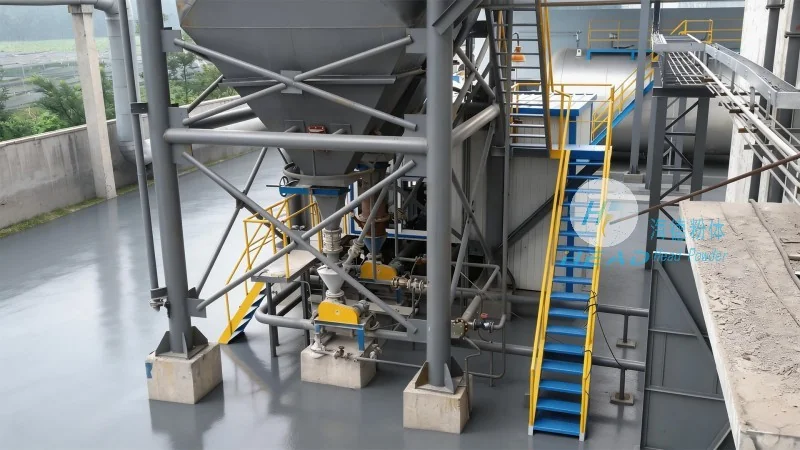
Working Principle of Multi-Hopper Pneumatic Conveying Equipment
The fundamental operation of multi-hopper pneumatic conveying systems revolves around the use of compressed air to create a pressure differential that moves material through a pipeline. The system typically comprises multiple hoppers, each equipped with a controlled valve that allows for sequential material release. As compressed air is introduced into the conveying line, it generates a low-pressure zone that draws material from the hoppers into the pipeline. The material is then carried by the air flow, which can operate under either positive or negative pressure, depending on the specific application and material characteristics.
Each hopper functions independently, enabling operators to manage the flow of different materials or switch between products without disrupting the entire system. This modularity enhances flexibility and allows for the simultaneous handling of multiple materials. The air compressor, a critical component, maintains the necessary pressure to ensure consistent material transport. The system also incorporates filters and moisture separators to maintain air quality and prevent contamination of the conveyed materials, ensuring product purity and system longevity.
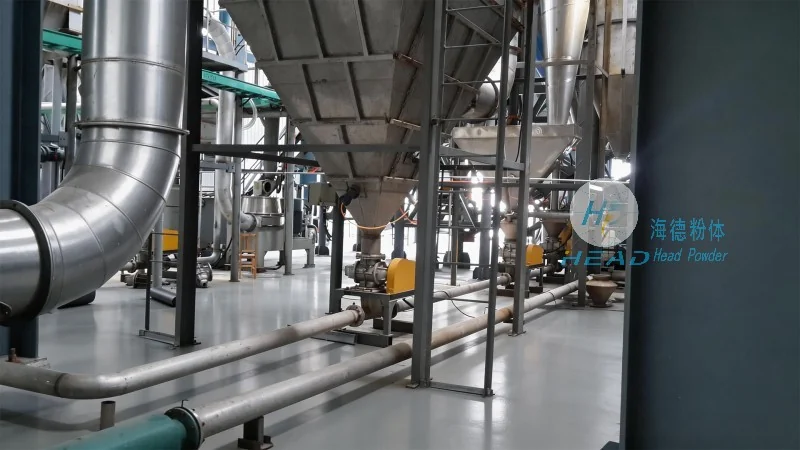
Key Features of Multi-Hopper Pneumatic Conveying Equipment
One of the most significant features of multi-hopper systems is their high efficiency in material transport. By leveraging compressed air, the equipment can move materials rapidly over considerable distances, reducing the need for manual handling and associated labor expenses. The modular design with multiple hoppers allows for the handling of diverse materials, including powders, granules, and bulk solids, making it versatile for various industrial applications.
Another critical feature is the system's ability to maintain material integrity and cleanliness. The enclosed design prevents external contamination and minimizes dust emissions, which is essential in industries where product purity is non-negotiable, such as food and pharmaceuticals. The equipment also offers precise control over flow rate and pressure, ensuring consistent and reliable material delivery to the target location, thereby reducing downtime and improving operational reliability.
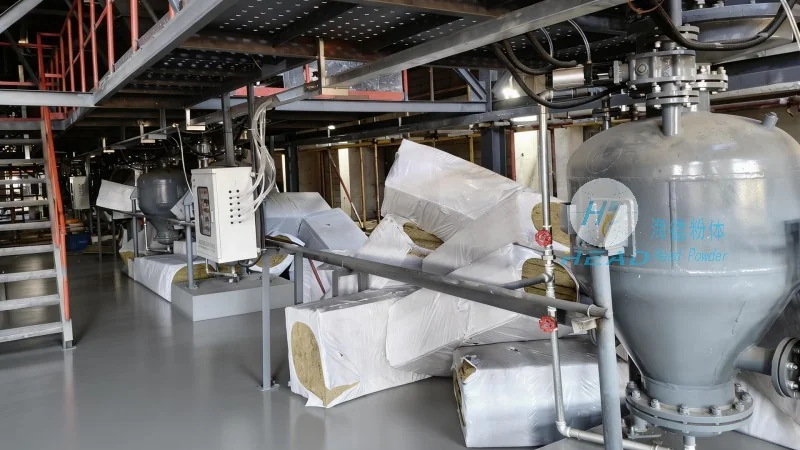
Flexibility is a standout characteristic. The ability to switch between hoppers or adjust air pressure allows for dynamic material handling, adapting to changing production schedules or material types. This adaptability makes the system suitable for both continuous and batch processing operations. Additionally, the system's low maintenance requirements and long service life contribute to its cost-effectiveness over time, providing a favorable return on investment for businesses.
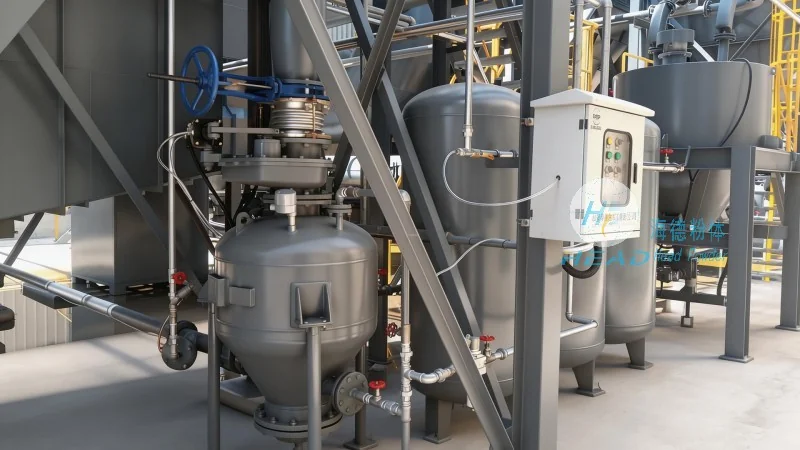
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., branded as headpowder, is a leading manufacturer specializing in advanced material handling solutions. The company focuses on innovation and quality, developing and producing multi-hopper pneumatic conveying equipment tailored to meet the diverse needs of various industries. HeadPowder's products are engineered to deliver superior performance, reliability, and efficiency, ensuring that clients achieve optimal material handling outcomes.
HeadPowder is committed to providing comprehensive support, including design, installation, and after-sales service, to ensure that its customers receive the best possible solutions for their material transport challenges. The company's headquarters and main operations are located in Shandong, China, where it leverages local expertise and resources to deliver high-quality products and services to a global market, reinforcing its position as a trusted partner in material handling technology.