

What is a Positive Pressure Dilute Phase Powder Handling Equipment? And What Are Its Design Principl
Positive pressure dilute phase powder handling equipment is a specialized system designed for the efficient and reliable transportation of bulk powders over long distances. This technology is widely used in various industrial sectors, including chemical, pharmaceutical, food, and mining, where the safe and effective movement of powders is critical to operational efficiency.
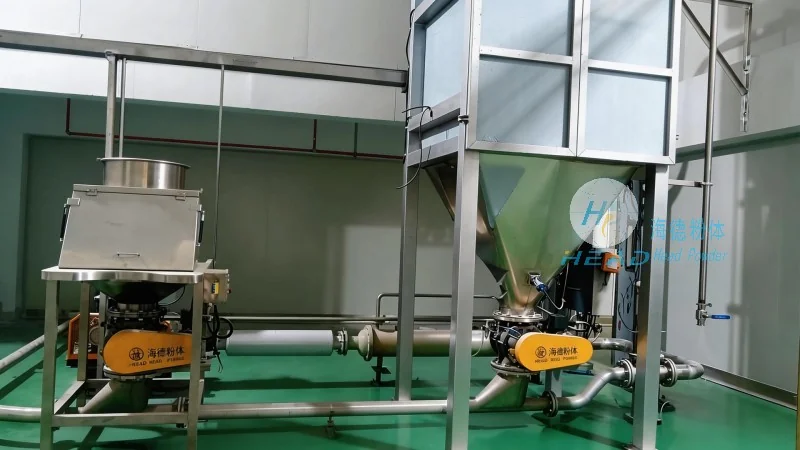
Understanding Positive Pressure Dilute Phase Powder Handling Equipment
At its core, a positive pressure dilute phase powder handling system operates by creating a positive pressure environment within the pipeline. This is achieved by using a high-pressure air or gas stream to transport the powder particles, which are suspended in the gas as a dilute phase. The key advantage of this method is its ability to handle a wide range of powder types, from fine powders to bulk materials, with minimal pressure drop and reduced risk of clogging compared to other powder handling techniques.
Design Principles of Positive Pressure Dilute Phase Powder Handling Equipment
The design of positive pressure dilute phase equipment is based on several fundamental principles that ensure optimal performance and reliability. These principles include maintaining a consistent air-to-powder ratio, controlling the velocity of the gas stream to prevent particle settling, and ensuring proper pipeline sizing to minimize pressure losses. The system typically consists of a powder feeder, a positive displacement blower or compressor, a pipeline network, and a receiver or discharge unit. Each component is carefully engineered to work in harmony, ensuring that the powder is transported smoothly and without degradation.
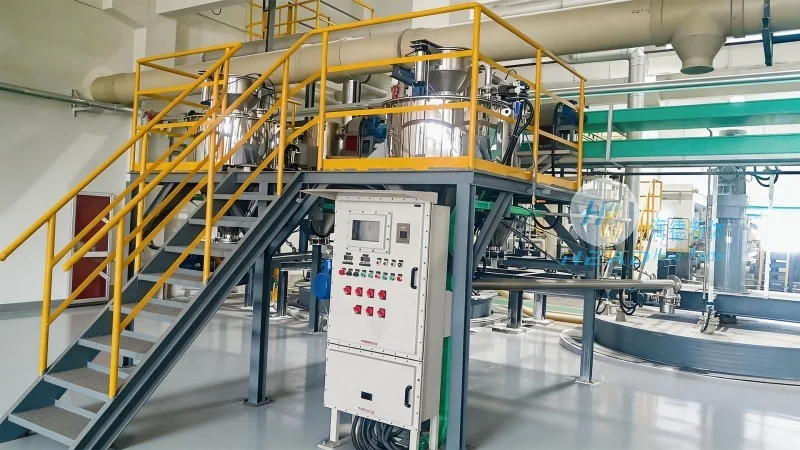
Key Components and Their Functions
Several critical components make up a positive pressure dilute phase powder handling system. The powder feeder is responsible for accurately metering the powder into the system, ensuring a consistent flow rate. The positive displacement blower or compressor provides the necessary pressure and airflow to transport the powder. The pipeline network, often made of materials such as stainless steel or plastic, conveys the powder mixture. The receiver or discharge unit collects the powder at the destination, allowing for controlled discharge. Each component is designed to withstand the abrasive nature of powders and the high-pressure environment, ensuring long-term durability and performance.
Applications and Benefits in Industrial Settings
Positive pressure dilute phase powder handling equipment is employed in numerous industrial applications where the transportation of bulk powders is essential. In the chemical industry, it is used for transporting raw materials and finished products, such as pigments and catalysts. In the pharmaceutical sector, it ensures the safe handling of active pharmaceutical ingredients (APIs) and excipients, maintaining product purity and preventing contamination. The food industry utilizes this technology for transporting ingredients like flour, sugar, and spices, while the mining industry uses it for conveying ore and other bulk materials from processing plants to storage or shipping facilities.
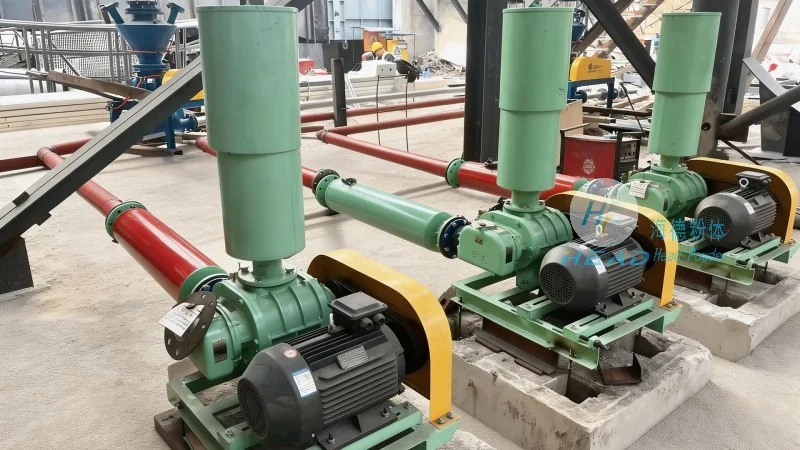
Advantages of Positive Pressure Dilute Phase Powder Handling
Compared to other powder handling methods, such as vacuum systems or dense phase conveying, positive pressure dilute phase equipment offers several advantages. These include higher transport velocities, which reduce overall system size and installation costs, and the ability to handle a wider range of powder characteristics. The system is also more energy-efficient, as it requires less power to achieve the same transport capacity. Additionally, the positive pressure environment helps prevent the ingress of external contaminants, ensuring the integrity of the powder being transported.
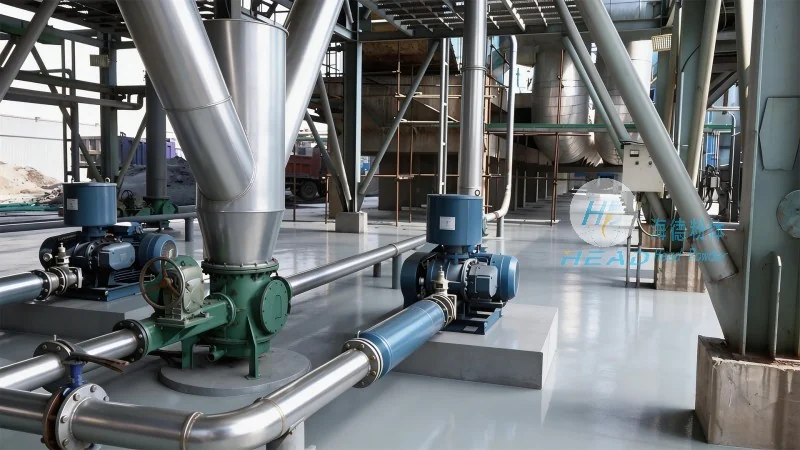
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced powder handling equipment. With a strong focus on innovation and quality, the company specializes in designing and manufacturing positive pressure dilute phase powder handling systems tailored to the specific needs of various industries. HeadPowder's products are engineered to meet international standards and are backed by a team of experienced engineers and technicians who provide comprehensive support, from system design and installation to maintenance and troubleshooting.
Conclusion
Positive pressure dilute phase powder handling equipment is a vital technology in modern industrial operations, offering efficient, reliable, and cost-effective solutions for bulk powder transportation. By understanding its design principles and components, industries can optimize their powder handling processes, improve operational efficiency, and ensure product quality. With the expertise and commitment of companies like Shandong HeadPowder Engineering Co., Ltd., the implementation and maintenance of these systems are made easier, enabling businesses to achieve their operational goals with confidence.