

What is a Tonne Bag Unpacking and Powder Conveying Equipment? And What Are Its Design Principles?
Understanding the Tonne Bag Unpacking and Powder Conveying Equipment is crucial for industries that rely on efficient handling of bulk powders. This equipment is specifically designed to streamline the process of unloading, conveying, and transferring materials from large tonne bags into processing systems. The design principles behind such equipment are centered on optimizing performance, ensuring safety, and maximizing operational efficiency.
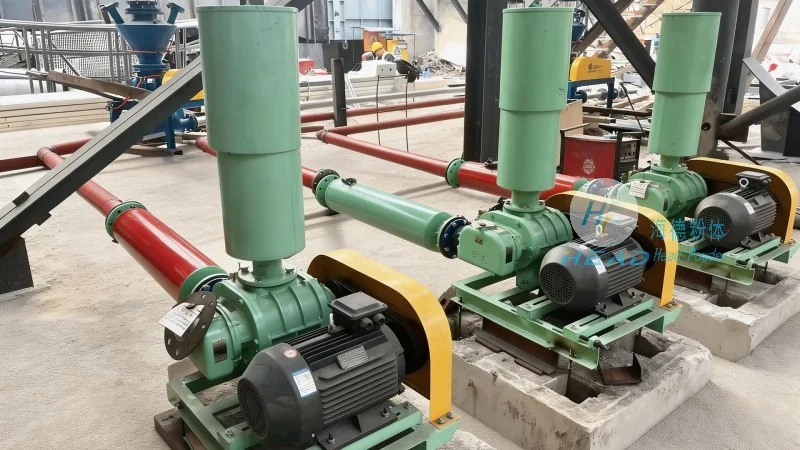
Introduction to Tonne Bag Unpacking and Powder Conveying Equipment
The Tonne Bag Unpacking and Powder Conveying Equipment, often referred to as a bulk bag discharger or bulk bag unloader, is a specialized system used in various industrial applications. Its primary function is to facilitate the transfer of bulk materials from large flexible containers, commonly known as tonne bags or super sacks, into processing equipment like mixers, hoppers, or storage silos. This equipment is essential for industries such as chemicals, food processing, pharmaceuticals, and mining, where handling large volumes of powders is a regular operation.

Key Components and Functional Design
The design of a tonne bag unloading system typically includes several critical components that work in tandem to ensure smooth operation. These components include a hopper or receiving chamber, a discharge valve or gate, a conveyor system (often a screw conveyor or pneumatic conveyor), and a dust collection system. The hopper is designed to hold the material from the tonne bag, allowing it to flow into the discharge mechanism. The discharge valve, which may be a rotary valve or a gate valve, controls the flow rate of the material into the conveyor. The conveyor then transports the material to the next stage of processing or storage. Additionally, a dust collection system is integrated to capture any airborne particles, ensuring a clean and safe working environment.
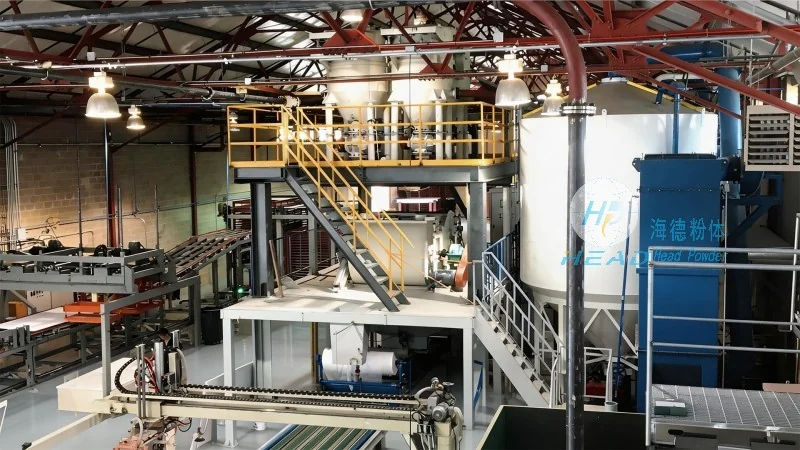
Design Principles for Efficient Operation
The design principles of tonne bag unloading equipment are focused on several key aspects to achieve optimal performance. First, the equipment must be able to handle a wide range of powder characteristics, including different densities, flowability, and moisture content. This requires a flexible design that can accommodate various material properties. Second, the system must ensure minimal product loss and contamination. The design includes features like airtight seals and cleanable components to maintain product integrity. Third, operational safety is a critical design consideration. The equipment incorporates safety features such as emergency stop buttons, overload protection, and proper ventilation to prevent dust explosions and ensure operator safety. Fourth, energy efficiency is also a key design principle. The system is engineered to minimize energy consumption while maintaining high throughput rates, reducing operational costs for the user.
Applications and Benefits in Industrial Settings
The Tonne Bag Unpacking and Powder Conveying Equipment offers numerous benefits to industrial operations. By automating the unloading process, it reduces labor costs and minimizes the risk of manual handling injuries. The equipment also improves process consistency and accuracy by ensuring a consistent flow rate of material into processing equipment. This leads to better product quality and reduced waste. Additionally, the dust collection system helps maintain a clean and safe workplace, complying with environmental regulations and improving overall operational conditions. The equipment's modular design allows for easy integration into existing production lines, making it a versatile solution for various industrial needs.
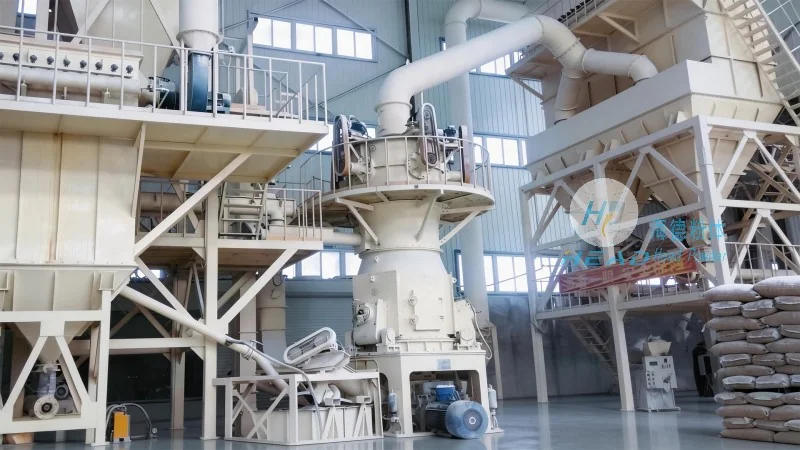
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of bulk material handling equipment, specializes in providing high-quality tonne bag unloading and powder conveying systems. With a focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's equipment is designed and manufactured to meet the specific needs of various industries, ensuring reliability, efficiency, and durability. The company's commitment to quality and customer support has made it a preferred choice for businesses seeking reliable bulk material handling solutions. Located in Shandong, China, HeadPowder leverages its expertise and advanced technology to deliver equipment that meets the highest standards of performance and safety.