

What is a Barley Pneumatic Conveying System? And What Are Its Design Principles?
For those in the agricultural and processing industries, understanding the technology behind efficient material handling is crucial. One such system that has gained prominence in handling bulk materials like barley is the pneumatic conveying system. This article aims to explore what a barley pneumatic conveying system is and delve into its fundamental design principles, providing insights into how such systems operate and their importance in modern processing operations.
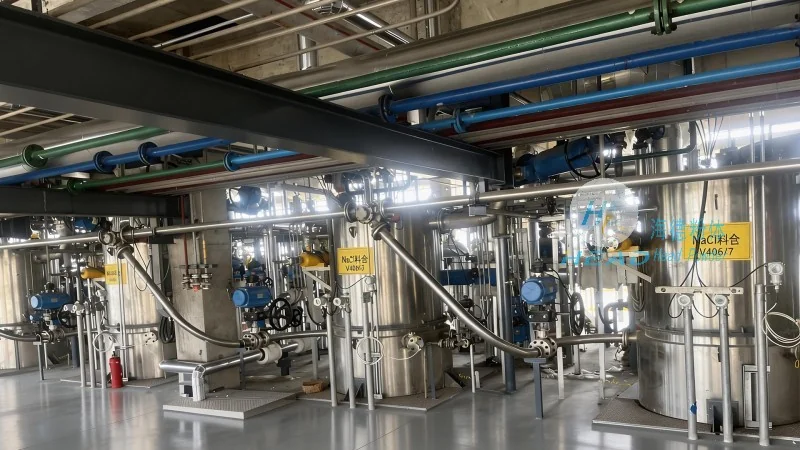
Understanding the Barley Pneumatic Conveying System
A barley pneumatic conveying system is a method of transporting barley and other bulk grains using a combination of air and pressure or vacuum. Unlike traditional mechanical conveyors, which rely on physical components like belts or buckets, pneumatic systems utilize air to move material through a pipeline. This technology is particularly advantageous for handling delicate or dusty materials like barley, as it minimizes product degradation and reduces the risk of contamination.
Key Components of a Barley Pneumatic Conveying System
At the core of any pneumatic conveying system are several key components that work in tandem to ensure efficient material transport. These components include the hopper or feed point, where the barley is loaded; the conveyor line, which is typically a series of pipes; the air mover, such as a blower or vacuum pump; and the control system that regulates the flow of air and material. Each component plays a critical role in the overall performance and reliability of the system.

The Design Principles Behind Pneumatic Conveying
The design of a barley pneumatic conveying system is based on several fundamental principles that ensure optimal performance. The first principle is the selection of the appropriate air velocity, which must be high enough to keep the material in suspension but not so high as to cause excessive wear on the system components. The second principle is the consideration of the material's properties, such as particle size, density, and moisture content, as these factors directly impact the system's efficiency and capacity. Additionally, the system's design must account for the need to minimize pressure drops along the conveyor line, which can affect the overall throughput and energy consumption.
Advantages of Using a Pneumatic Conveying System for Barley
Implementing a pneumatic conveying system for barley offers several advantages over traditional methods. One of the most significant benefits is the reduction in product damage, as the system uses air to move material rather than physical contact. This is particularly important for barley, which can be easily bruised or broken during handling. Another advantage is the improved hygiene and cleanliness, as the system can be designed to be fully enclosed, preventing dust and contamination from entering the processing environment. Furthermore, pneumatic systems are highly flexible and can be easily integrated into existing processing lines, allowing for adjustments in capacity and layout as needed.
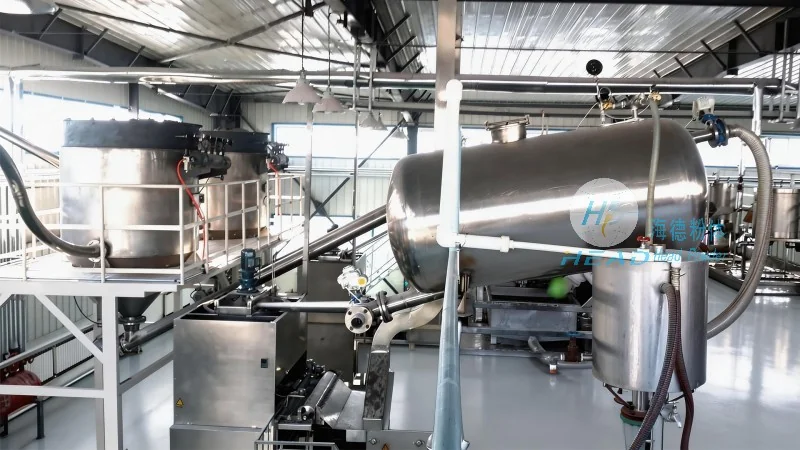
Application in Modern Processing Facilities
In modern agricultural and food processing facilities, the barley pneumatic conveying system is a vital component of the material handling process. These systems are commonly used in the storage, transportation, and processing of barley, from the initial reception of raw grain to the final packaging of finished products. The efficiency and reliability of these systems contribute significantly to the overall productivity and profitability of the facility. By understanding the design principles and advantages of pneumatic conveying, businesses can make informed decisions about implementing such systems to enhance their operations.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of pneumatic conveying systems, specializes in providing high-quality solutions for the agricultural and food processing industries. With years of experience and a commitment to innovation, the company has developed advanced systems tailored to the specific needs of barley and other bulk materials. HeadPowder's expertise lies in designing and manufacturing systems that are efficient, reliable, and cost-effective, ensuring that clients can achieve optimal performance in their processing operations. The company's facilities are located in Shandong, China, where it continues to lead the industry in providing cutting-edge pneumatic conveying solutions.