

Principle of Gelatin Pneumatic Conveying System
HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced pneumatic conveying systems tailored for the gelatin industry. This article delves into the fundamental principles and operational mechanics of such systems, highlighting their efficiency and reliability in handling gelatin materials.
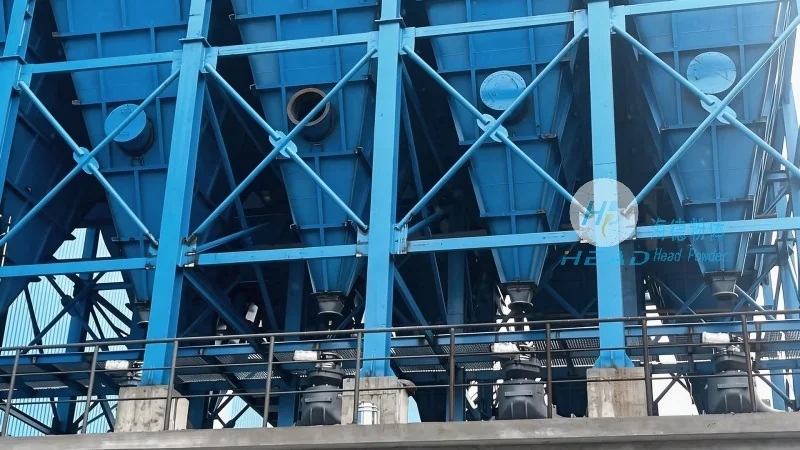
Understanding Pneumatic Conveying Systems
Pneumatic conveying systems utilize air or gas to transport bulk materials like gelatin through a network of pipes. This method offers a dust-free, hygienic, and efficient alternative to traditional mechanical conveying, making it ideal for food-grade applications where contamination and product degradation must be minimized.
Key Components of a Gelatin Pneumatic Conveying System
The core components of a typical gelatin pneumatic conveying system include a material hopper, a rotary valve or feeder, a conveying line, a dust collector, and a receiver or discharge point. Each component plays a critical role in ensuring smooth and controlled material flow.
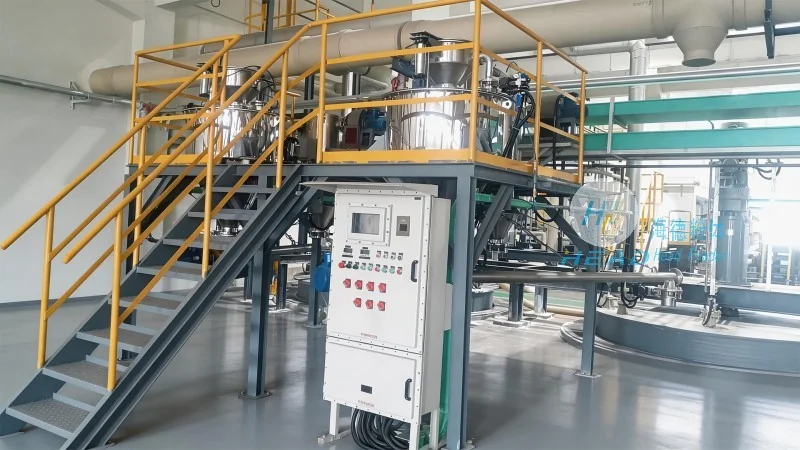
The material hopper stores the gelatin, providing a consistent feed to the system. The rotary valve or feeder regulates the flow of gelatin into the conveying line, preventing overloading and maintaining a steady pressure. The conveying line, often made of stainless steel to ensure hygiene and durability, transports the gelatin using compressed air or gas. The dust collector captures any fine particles or dust, ensuring the system operates in a clean environment. Finally, the receiver or discharge point collects the gelatin at the destination, completing the transport process.
How the System Works: The Pneumatic Conveying Process
The operation of a gelatin pneumatic conveying system involves several stages. Initially, the gelatin is fed from the hopper into the conveying line via the rotary valve. Compressed air is then introduced into the line, creating a low-pressure zone that draws the gelatin particles along with the air stream. As the gelatin travels through the pipe, it is suspended and transported to the receiver. The air, now carrying the gelatin, passes through the dust collector, where the gelatin is separated from the air and collected in the receiver. The cleaned air is then discharged back into the environment or recirculated if necessary.
Advantages of Using Pneumatic Conveying for Gelatin
Implementing a pneumatic conveying system for gelatin offers numerous advantages over traditional methods. Firstly, it provides a completely dust-free environment, which is crucial for maintaining the purity and quality of gelatin, especially in food and pharmaceutical applications. Secondly, the system is highly efficient, capable of transporting large volumes of material over long distances with minimal energy consumption. Thirdly, it reduces product degradation by minimizing friction and exposure to air, preserving the gelatin's texture and properties. Additionally, the system is easy to clean and maintain, ensuring compliance with hygiene standards and facilitating quick changeovers between different product batches.
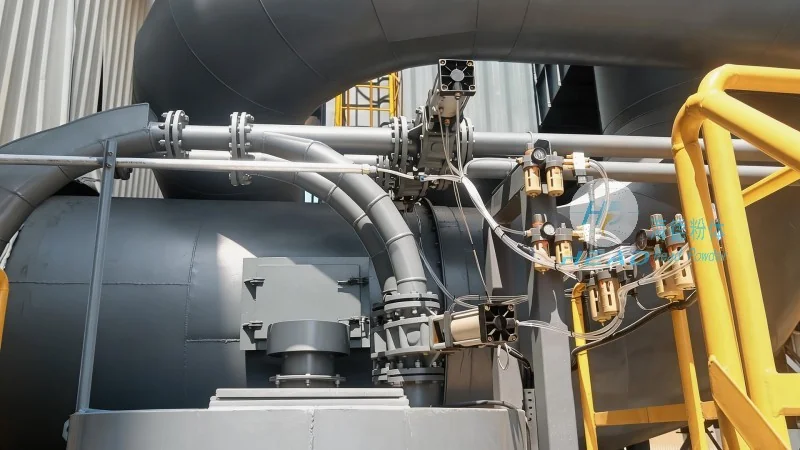
HeadPowder's Expertise in Gelatin Pneumatic Conveying
As a reputable company based in Shandong, China, HeadPowder Engineering Co., Ltd. has extensive experience in designing and manufacturing customized pneumatic conveying systems for the gelatin industry. Our systems are engineered to meet the specific requirements of gelatin processing, ensuring optimal performance, reliability, and compliance with industry standards. We utilize high-quality materials and advanced technology to deliver solutions that enhance productivity, reduce operational costs, and improve overall process efficiency.
Conclusion
Gelatin pneumatic conveying systems represent a sophisticated and effective solution for transporting gelatin materials. By understanding the fundamental principles and components of these systems, as well as the advantages they offer, businesses can make informed decisions about implementing such technology. HeadPowder remains committed to providing top-tier pneumatic conveying solutions that meet the evolving needs of the gelatin industry, ensuring high-quality, efficient, and hygienic material handling.