

Coke Powder Pneumatic Conveying Technology: In-Depth Analysis of Negative Pressure and Positive Pres
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems for coke powder. This article delves into the core principles of negative pressure and positive pressure conveying technologies, exploring their applications, advantages, and practical considerations in industrial settings.
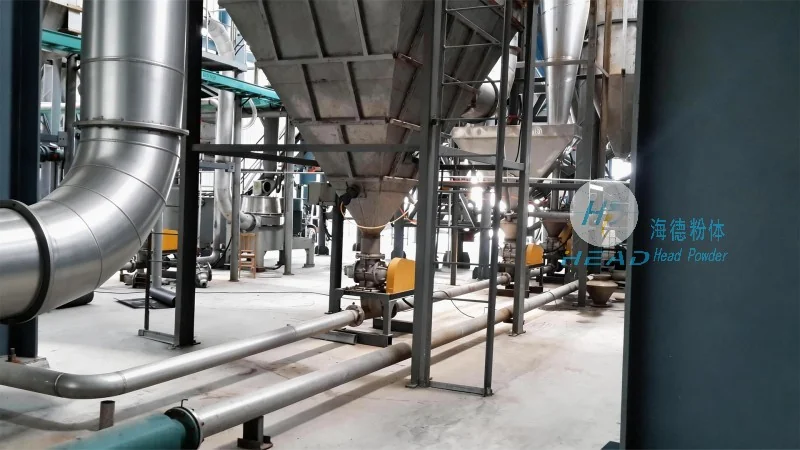
Understanding Negative Pressure Pneumatic Conveying
Negative pressure, or vacuum, pneumatic conveying systems operate by creating a lower pressure environment at the material inlet, drawing the coke powder into the conveying line. This method is particularly effective for transporting materials over moderate distances, typically up to several hundred meters, and is well-suited for applications where the material is sensitive to high pressure or where dust containment is critical. The system uses a vacuum pump to generate the suction force, ensuring a controlled and efficient flow of coke powder from the source to the destination.
Advantages of Negative Pressure Conveying
One of the key benefits of negative pressure systems is their ability to handle fine or dusty materials without causing excessive wear on the equipment. The enclosed pipeline design minimizes dust emissions, making it an ideal choice for environments where air quality regulations are stringent. Additionally, these systems can operate with lower air velocities compared to positive pressure systems, reducing energy consumption and extending the lifespan of components such as filters and valves.
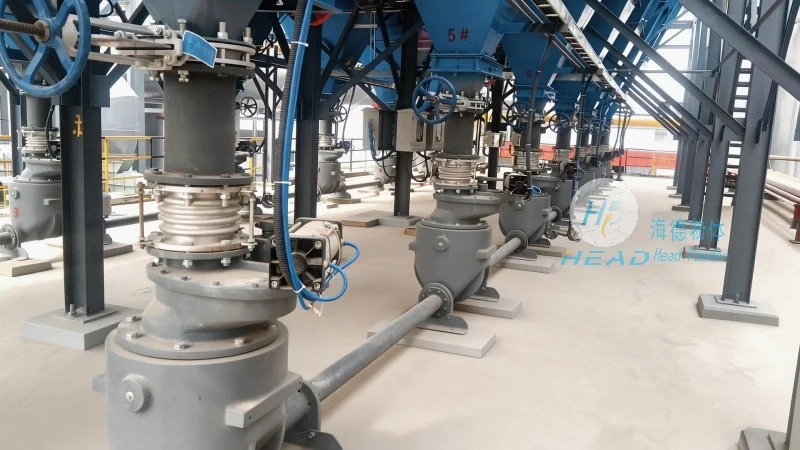
Positive Pressure Pneumatic Conveying
In contrast, positive pressure conveying systems generate higher pressure at the material inlet, pushing the coke powder through the conveying line. This approach is typically used for longer distances, often exceeding 500 meters, and is suitable for bulk material handling where high flow rates are required. The system employs a positive displacement blower or compressor to deliver the air, ensuring a consistent and powerful flow that can handle larger quantities of coke powder.
Advantages of Positive Pressure Conveying
Positive pressure systems excel in applications that demand high throughput and long-distance transport. They are particularly effective for transporting cohesive or abrasive materials, as the higher air pressure helps to break up agglomerates and maintain a consistent flow. Furthermore, these systems can be designed with multiple inlets and outlets, allowing for flexible material distribution to various destinations within a facility.
Key Considerations for Choosing the Right Conveying System
The selection between negative and positive pressure pneumatic conveying for coke powder depends on several factors, including the distance between the source and destination, the material's physical properties (such as particle size, moisture content, and dustiness), and the required flow rate. HeadPowder engineers conduct thorough assessments to evaluate these parameters and recommend the most suitable system configuration. For instance, in applications where the material is highly abrasive or prone to caking, a positive pressure system with robust components may be preferred to ensure long-term reliability.
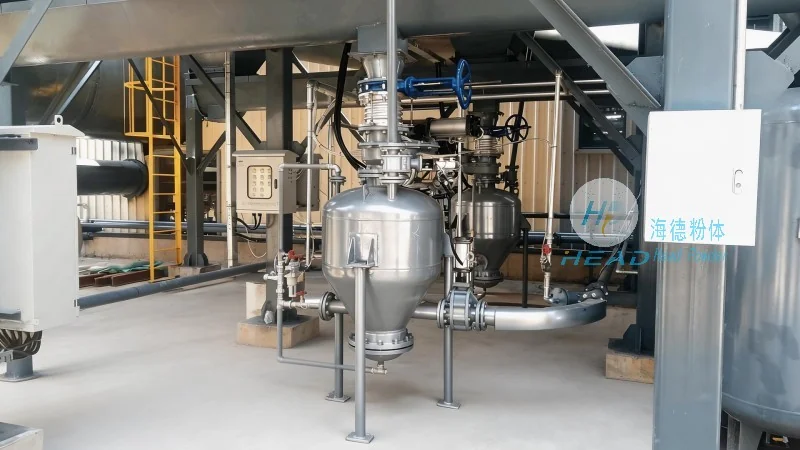
Application Examples in Industrial Settings
HeadPowder has successfully implemented both negative and positive pressure pneumatic conveying systems in various industrial sectors. In a steel plant, a negative pressure system was used to transport coke powder from storage silos to the blast furnace, ensuring a dust-free and efficient supply chain. In another case, a positive pressure system was deployed in a chemical plant to convey coke powder over a distance of 800 meters, supporting high-volume production processes. These examples highlight the versatility of pneumatic conveying technologies and their ability to adapt to diverse operational requirements.
Conclusion and Future Directions
As industrial processes continue to evolve, the demand for efficient and reliable material handling solutions remains high. HeadPowder's expertise in negative and positive pressure pneumatic conveying technologies positions the company as a trusted partner for coke powder handling projects. By leveraging advanced engineering principles and tailored system designs, HeadPowder ensures that clients achieve optimal performance, minimal downtime, and compliance with industry standards. The future of coke powder pneumatic conveying lies in the integration of smart technologies, such as real-time monitoring and predictive maintenance, which will further enhance system efficiency and longevity.