

Introduction to Cement Powder Conveying Systems and the Advantages of Cement Powder Pneumatic Convey
HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of advanced cement powder conveying systems. This article provides an overview of cement powder conveying systems and highlights the key advantages of pneumatic conveying technology for transporting cement powders efficiently and reliably.
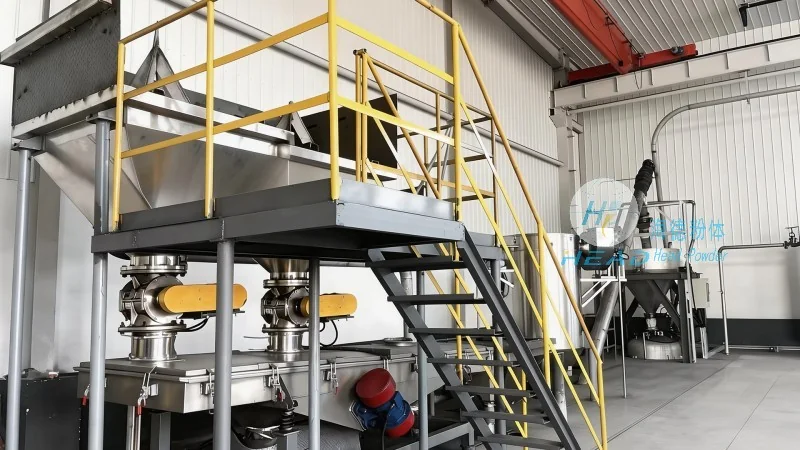
Cement Powder Conveying Systems: An Overview
Cement powder conveying systems are engineered to transport cement powders from storage silos or production lines to various processing or application points. These systems are crucial in cement manufacturing, construction, and related industries where the efficient movement of bulk cement powders is essential for maintaining production efficiency and product quality. The primary components of a typical cement powder conveying system include storage silos, conveying pipelines, air movers (such as blowers or fans), control systems, and discharge equipment. The system operates by creating a pressure differential that propels the cement powder through the pipeline using air, ensuring a continuous and controlled flow of material.
The Advantages of Pneumatic Conveying for Cement Powders
Pneumatic conveying, also known as air-pneumatic conveying, offers several significant advantages over traditional mechanical conveying methods for cement powders. One of the most notable benefits is its ability to handle fine, dusty materials like cement powder without the need for mechanical components that can cause wear and tear or blockages. The air-based system minimizes the risk of material degradation and contamination, which is critical for maintaining the quality of cement products. Additionally, pneumatic conveying systems are highly flexible, allowing for changes in the conveying route or capacity without major modifications to the infrastructure. This adaptability makes them suitable for both new installations and retrofitting existing facilities.
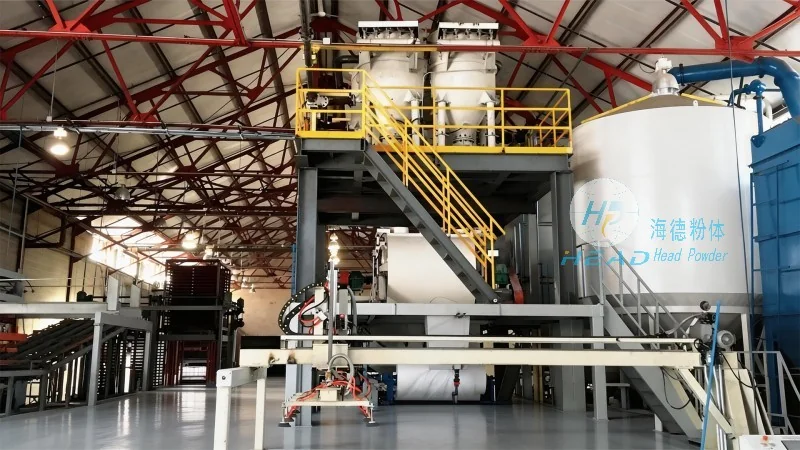
Efficiency and Cost-Effectiveness in Cement Powder Handling
Efficiency is a key factor in the selection of cement powder conveying systems, and pneumatic conveying excels in this area. By using compressed air to move the material, the system reduces energy consumption compared to mechanical systems that rely on motors and belts. The continuous flow of material minimizes downtime and ensures a steady supply of cement to downstream processes, such as mixing or packaging. Furthermore, the reduced need for maintenance due to fewer mechanical parts translates into lower operational costs over the system's lifespan. HeadPowder's expertise in designing customized pneumatic conveying solutions ensures that clients achieve optimal efficiency and cost savings tailored to their specific operational needs.
Environmental and Safety Benefits
Environmental considerations are increasingly important in industrial operations, and pneumatic conveying systems provide several environmental advantages. Unlike mechanical systems that may generate dust and noise, pneumatic conveying operates with enclosed pipelines, reducing dust emissions and minimizing the impact on the surrounding environment. This enclosed system also enhances workplace safety by preventing dust exposure to personnel and reducing the risk of fire hazards associated with fine powders. The controlled environment of pneumatic conveying contributes to a safer working atmosphere and compliance with environmental regulations. HeadPowder's systems are designed with these safety and environmental aspects in mind, ensuring that clients not only improve operational efficiency but also meet regulatory standards.
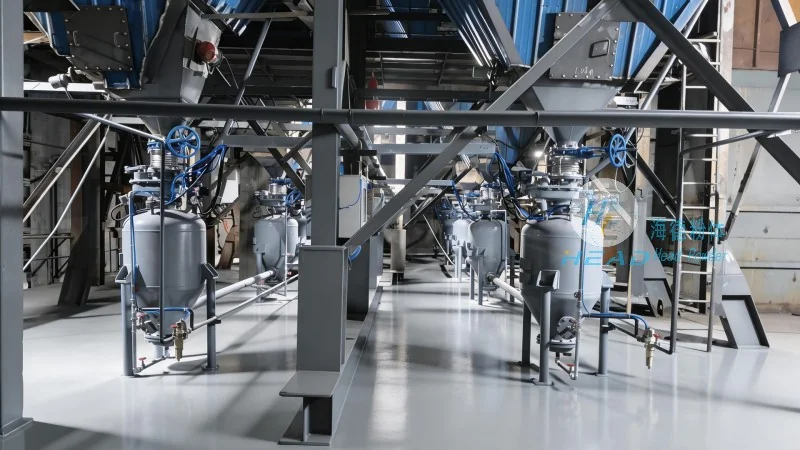
Customization and Scalability for Diverse Applications
Every cement production facility has unique requirements, and HeadPowder recognizes the importance of customization in delivering effective conveying solutions. Our team of engineers works closely with clients to assess their specific needs, including the volume of cement to be conveyed, the distance of the conveying route, and the existing infrastructure. Based on this assessment, we design and implement tailored pneumatic conveying systems that meet the exact specifications of the application. Whether it's a small-scale operation or a large industrial plant, our systems are scalable and can be expanded or modified as production needs evolve. This flexibility ensures that clients invest in a solution that grows with their business, providing long-term value and reliability.
Conclusion: Choosing the Right Conveying Solution for Cement Powders
In conclusion, cement powder conveying systems, particularly those utilizing pneumatic conveying technology, offer significant advantages in terms of efficiency, cost-effectiveness, environmental impact, and safety. HeadPowder, with its expertise and commitment to quality, provides comprehensive solutions that address the specific challenges of cement powder handling. By investing in a well-designed pneumatic conveying system, cement manufacturers can enhance their operational performance, reduce costs, and ensure compliance with industry standards. For businesses seeking reliable and efficient cement powder conveying solutions, HeadPowder stands as a trusted partner, delivering tailored systems that meet the highest industry standards.