

Introduction to Pharmaceutical Conveying Systems and the Advantages of Pneumatic Conveying Technolog
Pharmaceutical manufacturing demands precision, efficiency, and compliance with stringent regulatory standards. The seamless transfer of raw materials and finished products is a critical component of this process, and advanced conveying systems play a pivotal role in meeting these requirements. This article introduces pharmaceutical conveying systems, with a focus on the benefits and features of pneumatic conveying technology, as offered by Shandong HeadPowder Engineering Co., Ltd., a leading provider based in China.
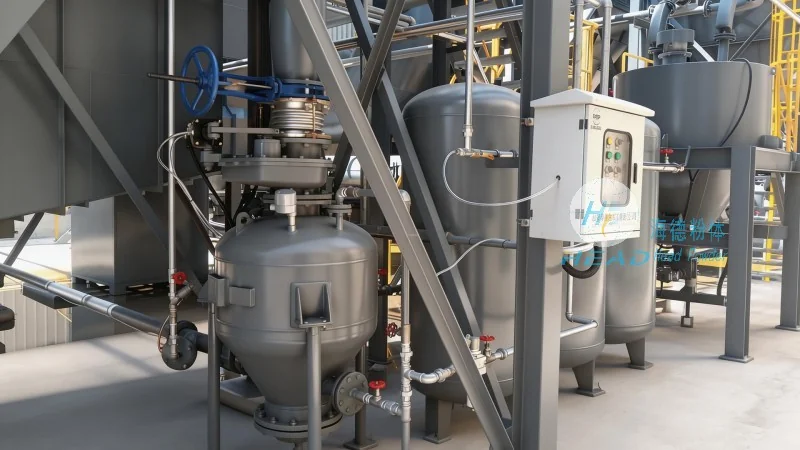
Understanding Pharmaceutical Conveying Systems
Pharmaceutical conveying systems are engineered to handle the unique challenges of the pharmaceutical industry, including the need for contamination control, material integrity, and adherence to Good Manufacturing Practices (GMP). These systems are designed to transport powders, granules, and other bulk materials safely and efficiently from one stage of production to another. The choice of conveying technology is crucial, as it directly impacts product quality, operational costs, and overall process reliability.
Pneumatic Conveying Technology: A Preferred Solution
Among the various conveying methods available, pneumatic conveying stands out as a versatile and effective solution for pharmaceutical applications. This technology uses air or other gases to move materials through a pipeline system, eliminating the need for mechanical components like belts or buckets that could introduce contaminants or cause material degradation. Pneumatic conveying systems are particularly well-suited for handling sensitive pharmaceutical powders, as they provide a closed, dust-free environment that minimizes the risk of cross-contamination and product degradation.
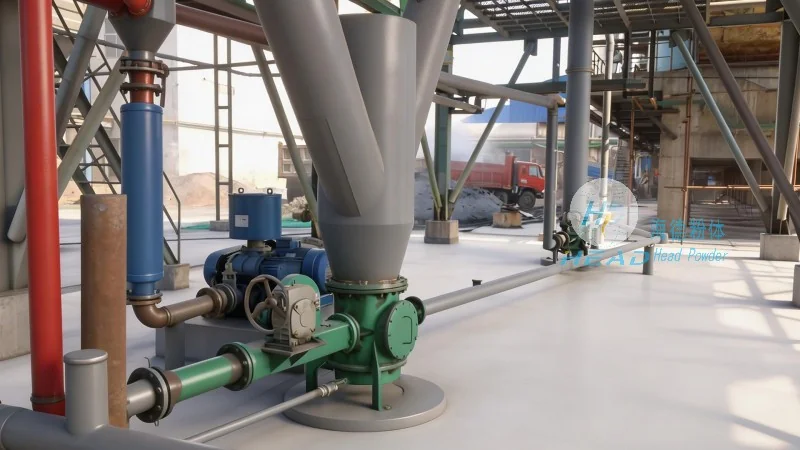
Key Advantages of Pneumatic Conveying in Pharmaceuticals
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing pneumatic conveying systems tailored to the specific needs of the pharmaceutical sector. The advantages of this technology include:
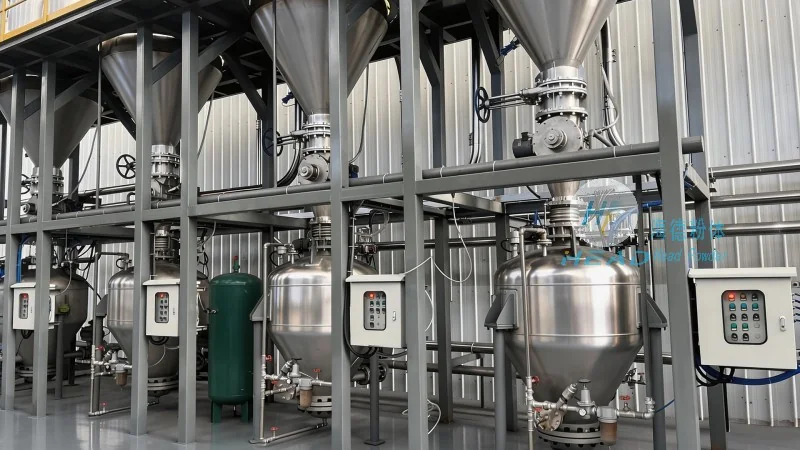
- Hygienic and Contamination-Free Operation: Pneumatic systems are fully enclosed, ensuring that materials remain protected from external contaminants and preventing cross-contamination between different product batches. This is essential for maintaining product purity and meeting regulatory requirements.
- Flexibility and Scalability: These systems can be easily adapted to accommodate changes in production volume or product types, making them suitable for both small-scale and large-scale pharmaceutical operations. The modular design allows for expansion or reconfiguration as business needs evolve.
- Energy Efficiency: Compared to traditional mechanical conveying methods, pneumatic systems often consume less energy while delivering comparable or superior performance. This contributes to lower operational costs and reduced environmental impact.
- Reduced Downtime and Maintenance: With fewer moving parts, pneumatic conveying systems experience less wear and tear, leading to lower maintenance requirements and extended equipment lifespan. This translates to fewer interruptions in production and lower long-term costs.
- Enhanced Product Integrity: The gentle handling of materials in a pneumatic system minimizes particle breakage and agglomeration, preserving the physical and chemical properties of the pharmaceutical product. This is critical for maintaining product efficacy and stability.
Customized Solutions for Pharmaceutical Manufacturers
Shandong HeadPowder Engineering Co., Ltd. understands that each pharmaceutical facility has unique operational requirements. The company offers customized pneumatic conveying solutions that are tailored to specific product characteristics, production volumes, and facility layouts. From initial system design and engineering to installation and ongoing support, HeadPowder provides comprehensive services to ensure that clients achieve optimal performance and compliance.
Conclusion
In conclusion, pharmaceutical conveying systems, particularly those utilizing pneumatic technology, are indispensable for modern pharmaceutical manufacturing. The advantages of hygienic operation, flexibility, energy efficiency, and product integrity make pneumatic conveying a preferred choice for pharmaceutical companies seeking to enhance their production processes. With its headquarters in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. continues to lead the industry in delivering high-quality, reliable conveying solutions that meet the demanding standards of the pharmaceutical sector.