

Operation Process and Working Principle of Bicarbonate of Soda Material Pneumatic Conveying Equipmen
HeadPowder, a renowned engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for various industrial applications. The company's expertise lies in delivering efficient and reliable solutions for material handling, particularly for bulk powders like bicarbonate of soda. This article delves into the operation process and working principle of their specialized equipment, providing a comprehensive understanding of how such systems function to meet industrial demands.
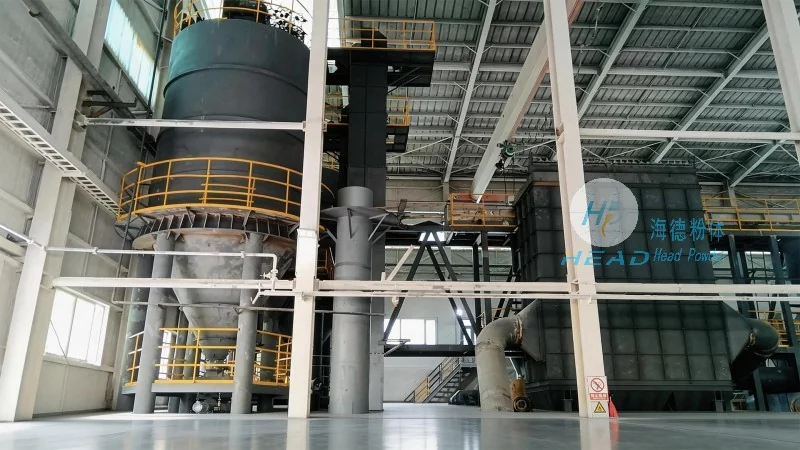
About HeadPowder: Leading Pneumatic Conveying Solutions Provider
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a prominent player in the field of material handling technology. With a strong presence in Shandong, China, the company has built a reputation for its innovative and durable pneumatic conveying equipment. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for industries requiring efficient bulk material transport solutions. The company's engineering team leverages years of experience to develop systems that optimize performance, reduce operational costs, and enhance safety in material handling processes.
Bicarbonate of Soda Pneumatic Conveying Equipment Overview
The bicarbonate of soda pneumatic conveying equipment developed by HeadPowder is engineered to handle the unique characteristics of this material. Bicarbonate of soda, commonly used in food, pharmaceutical, and chemical industries, presents challenges such as low bulk density and tendency to agglomerate. The equipment is designed to address these challenges through a combination of high-pressure air systems and specialized components that ensure smooth and efficient transport. Key features include adjustable air pressure controls, anti-clogging mechanisms, and material separation systems to maintain product integrity throughout the conveying process.
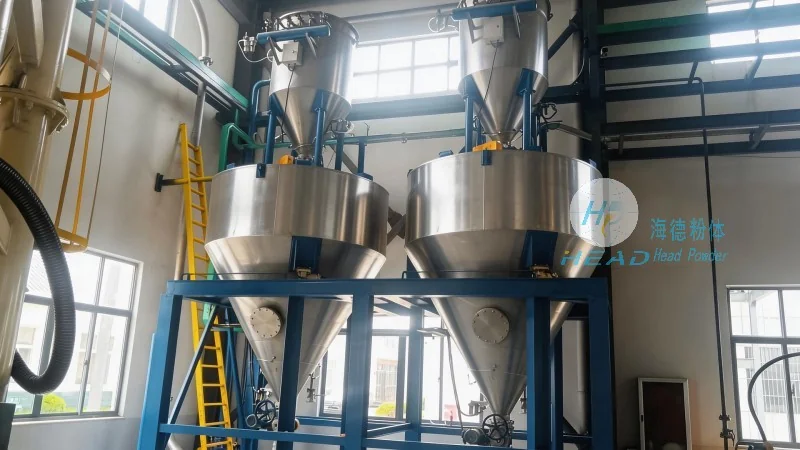
Operation Process of Bicarbonate of Soda Pneumatic Conveying Equipment
The operation of the bicarbonate of soda pneumatic conveying system involves several sequential steps that ensure seamless material transport from the source to the destination. Initially, the material is loaded into the hopper or storage tank. The system then uses a positive pressure or negative pressure air source to create a flow of air through the pipeline. As the air moves through the system, it carries the bicarbonate of soda particles along the pipeline. The equipment includes a series of components such as air compressors, filters, and control valves that regulate the air flow and pressure to maintain optimal conveying conditions. The process is automated, with sensors and control systems monitoring the flow rate and pressure to prevent overloading or system failures. The material is then discharged at the receiving end, where it is collected in a container or further processed as needed.
Working Principle of the Pneumatic Conveying System
The working principle of the bicarbonate of soda pneumatic conveying equipment is based on the fundamental concept of pneumatic transport, where air is used as the medium to move solid particles. The system operates under positive pressure, where compressed air is introduced into the conveying line, creating a high-pressure environment that propels the material forward. The air flow is controlled by the air compressor, which adjusts the pressure and volume to match the material's characteristics and the required conveying distance. The equipment includes a hopper with a feeder that ensures a consistent flow of material into the pipeline. As the material is drawn into the air stream, it is suspended and transported through the pipeline. The system may include a cyclone separator or other filtration components at the receiving end to separate the material from the air, ensuring that the product remains clean and free from contamination. The entire process is designed to minimize material degradation, maintain product quality, and reduce operational downtime.
Key Features and Advantages of the Equipment
HeadPowder's bicarbonate of soda pneumatic conveying equipment offers several advantages that make it suitable for industrial applications. The system is designed for high efficiency, with minimal energy consumption and low maintenance requirements. The adjustable air pressure and flow controls allow for customization to suit different material types and conveying distances. The equipment is also equipped with safety features, such as pressure relief valves and emergency shut-off systems, to prevent accidents and ensure operator safety. Additionally, the system's compact design and modular components make it easy to install and integrate into existing production lines. The use of high-quality materials and advanced manufacturing techniques ensures long-term durability and reliability, reducing the need for frequent repairs and replacements.
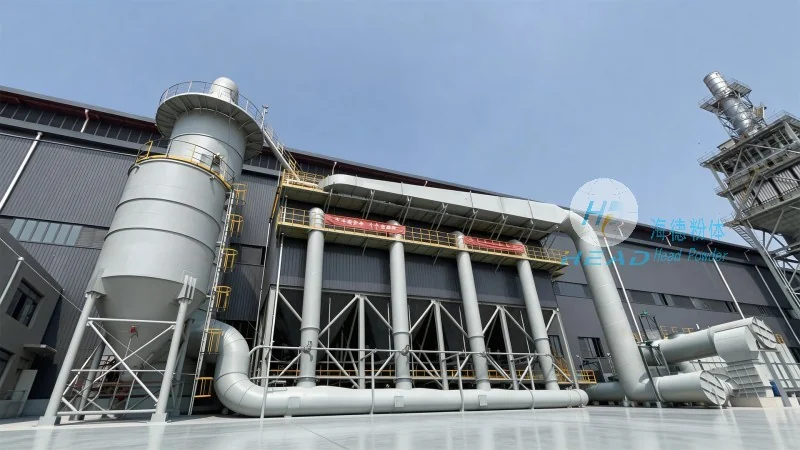
Application Scenarios and Industry Use Cases
The bicarbonate of soda pneumatic conveying equipment is widely used in various industries that require the transport of bulk powders. In the food industry, it is used for the transport of baking soda in food processing plants, ensuring that the material is handled hygienically and efficiently. In the pharmaceutical industry, the equipment is used to transport raw materials for the production of medications, maintaining strict quality control standards. The chemical industry also utilizes this system for the transport of bicarbonate of soda in chemical processing facilities, where precise control over material flow is critical. Additionally, the equipment is suitable for use in environmental and waste management applications, where the transport of bulk materials is necessary for treatment and disposal processes.
Conclusion: Enhancing Material Handling Efficiency with HeadPowder's Solutions
HeadPowder's bicarbonate of soda pneumatic conveying equipment represents a significant advancement in material handling technology. By combining advanced engineering, innovative design, and rigorous quality control, the company has developed a system that addresses the unique challenges of transporting bicarbonate of soda while ensuring high efficiency, product integrity, and operational safety. The operation process and working principle of the equipment are optimized to meet the demands of modern industrial applications, providing a reliable and cost-effective solution for bulk material transport. With its headquarters in Shandong, China, HeadPowder continues to lead the way in providing cutting-edge pneumatic conveying solutions that enhance productivity and sustainability in various industries.