

Operation Process and Working Principle of Wheat Starch Material Handling System
Wheat starch material handling systems are critical components in the food processing industry, particularly for manufacturers dealing with the production of wheat starch. These systems are designed to efficiently transport, process, and manage the flow of wheat starch from raw material reception to final product packaging. The operation process and working principle of such systems are intricate, involving multiple stages and specialized equipment to ensure optimal performance and product quality.
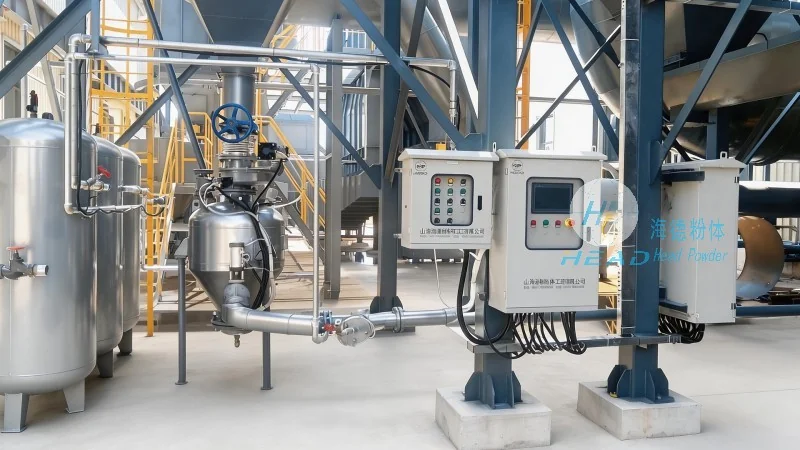
Overview of the Wheat Starch Material Handling System
The wheat starch material handling system typically consists of several interconnected components, including feeders, conveyors, storage silos, and processing units. Each component plays a vital role in the overall workflow, ensuring that the material is handled safely and efficiently. The system is engineered to handle the unique characteristics of wheat starch, such as its granular texture and moisture content, which can affect flow properties and processing efficiency.
Key Components and Their Functions
1. Feeders: Feeders are the initial components that receive raw wheat starch from storage bins or trucks. They are responsible for controlling the flow rate of the material into the system, ensuring a consistent and uniform feed to subsequent equipment. Different types of feeders, such as rotary or vibratory feeders, may be used depending on the material's characteristics and the required flow rate.
2. Conveyors: Conveyors are used to transport the wheat starch from the feeders to the processing units or storage areas. Various types of conveyors, including belt conveyors, screw conveyors, and pneumatic conveyors, are employed based on the system's requirements. Belt conveyors are commonly used for horizontal or slight incline transport, while screw conveyors are ideal for vertical or inclined transport due to their ability to handle bulk materials with minimal maintenance.
3. Storage Silos: Storage silos are used to store the wheat starch before it is processed or shipped. These silos are designed to maintain the material's quality by controlling moisture levels and preventing contamination. The silos are typically made of stainless steel or other corrosion-resistant materials to ensure durability and hygiene.
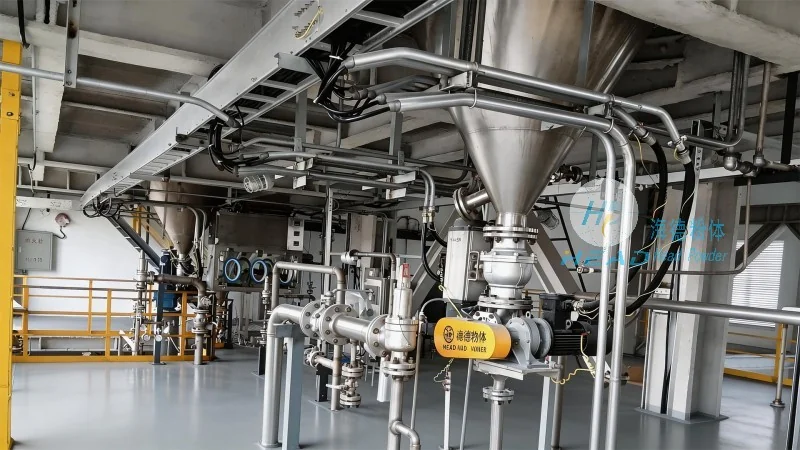
4. Processing Units: Processing units, such as grinding or milling equipment, are used to refine the wheat starch into the desired product specifications. These units are integrated with the material handling system to ensure a smooth flow of material from storage to processing and back to storage if needed.
Operation Process Flow
The operation process of a wheat starch material handling system begins with the reception of raw wheat starch. The material is first transferred from storage bins or trucks to the feeders using loading equipment. The feeders then regulate the flow rate, ensuring a consistent feed to the conveyors. The conveyors transport the material to the storage silos or directly to the processing units.
During the processing stage, the wheat starch is subjected to grinding or milling to achieve the desired particle size. The processed material is then conveyed to the final storage or packaging area. The system may also include quality control checkpoints to ensure that the product meets the required specifications before it is released for use.
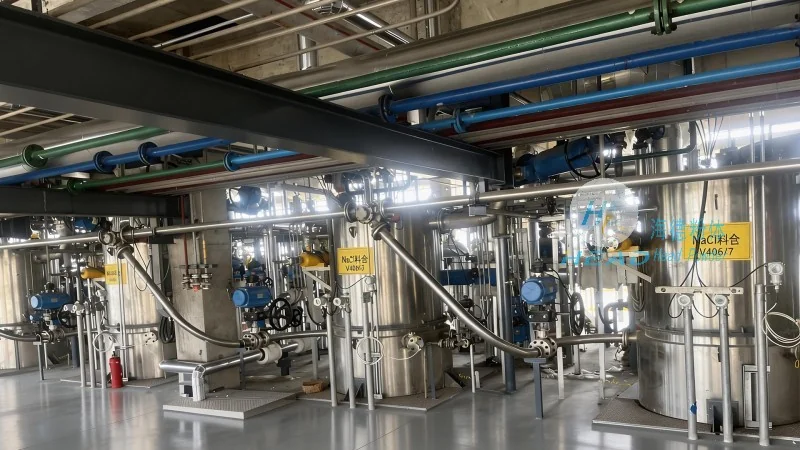
Working Principle of the System
The working principle of the wheat starch material handling system is based on the principles of material flow and mechanical handling. The system uses a combination of gravity, mechanical force, and pneumatic pressure to move the material through the various stages. The feeders control the initial flow, while the conveyors use mechanical means to transport the material. The storage silos use gravity to maintain the material's position, and the processing units use mechanical energy to refine the material.
The system is designed to be automated, with sensors and control systems monitoring the flow rate, level, and quality of the material at each stage. This automation ensures that the system operates efficiently and safely, minimizing downtime and maximizing productivity. The control systems also allow for adjustments to be made in real-time, ensuring that the system can adapt to changes in production demand or material characteristics.
Importance of Efficient Material Handling
Efficient material handling is crucial for the success of wheat starch production. A well-designed material handling system can significantly improve production efficiency, reduce labor costs, and enhance product quality. By ensuring a consistent flow of material, the system minimizes the risk of material buildup or blockages, which can lead to equipment damage or product contamination.
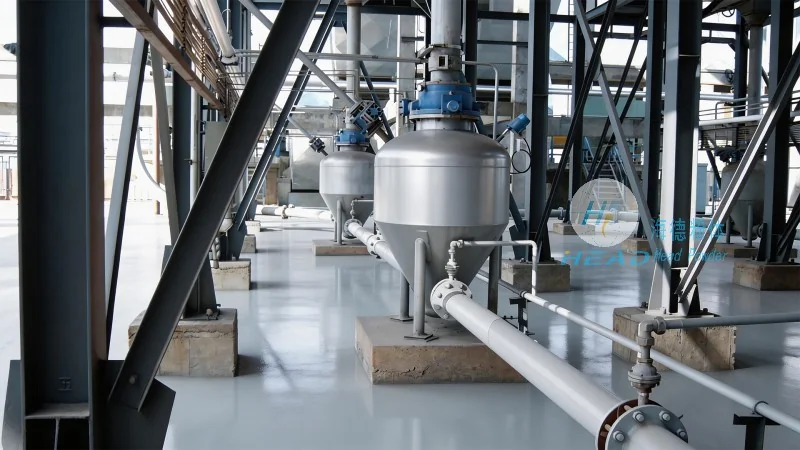
Additionally, an efficient system can help reduce energy consumption and operating costs. By optimizing the flow rate and transport methods, the system can minimize the use of energy and reduce maintenance requirements. This not only improves the economic viability of the production process but also contributes to environmental sustainability.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of material handling systems for the food processing industry. With years of experience and expertise, HeadPowder specializes in designing and manufacturing customized solutions for wheat starch and other food products. The company is committed to providing high-quality, reliable, and efficient systems that meet the specific needs of its clients.
HeadPowder's team of engineers and technicians work closely with clients to understand their production requirements and develop tailored material handling solutions. The company uses advanced technology and materials to ensure that its systems are durable, hygienic, and compliant with industry standards. HeadPowder's products are widely used in various food processing facilities, contributing to the efficiency and success of their operations.
With a strong focus on quality and customer satisfaction, HeadPowder has established itself as a trusted partner in the food processing industry. The company's commitment to innovation and excellence has enabled it to deliver solutions that meet the evolving needs of the market. HeadPowder's material handling systems are designed to enhance productivity, reduce costs, and improve product quality, making them an essential component of modern food processing operations.