

Operation Process and Working Principle of an Intelligent Tonne Bag Loading Station for Powder Mater
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and installation of advanced powder conveying systems. HeadPowder, as the company's abbreviation, has been committed to providing efficient and reliable solutions for the transportation of bulk powders. The company is headquartered in Shandong, China, where it leverages local industrial resources and expertise to develop cutting-edge equipment for various industries, including chemical, pharmaceutical, food, and more.
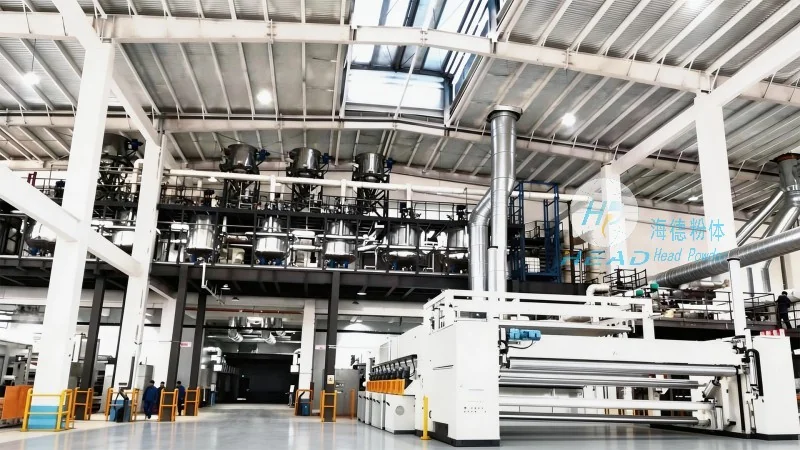
Introduction to the Intelligent Tonne Bag Loading Station
The intelligent tonne bag loading station is a sophisticated piece of equipment designed to automate the process of loading bulk powders from tonne bags into processing equipment or storage silos. This system integrates advanced sensors, control systems, and mechanical components to ensure precise and safe material handling. By eliminating manual labor and reducing human error, the station enhances operational efficiency and improves product quality. The system is engineered to handle a wide range of powder characteristics, from fine powders to bulkier materials, making it versatile for diverse industrial applications.
Key Components of the Powder Conveying System
The intelligent tonne bag loading station comprises several critical components that work in tandem to achieve seamless material transfer. These include the tonne bag support frame, which securely holds the bag during the loading process; the hopper and feeding mechanism, responsible for transferring the powder from the bag into the conveying system; and the control panel, which manages the entire operation through user-friendly interfaces. Additionally, the system may incorporate features such as level sensors to monitor the powder level in the hopper, pressure sensors to ensure safe operation, and automatic shut-off valves to prevent overfilling or blockages. Each component is meticulously designed to withstand the rigors of continuous operation and maintain high performance over time.
Operation Process of the Tonne Bag Loading Station
The operation of the intelligent tonne bag loading station follows a systematic sequence to ensure efficient and safe material handling. The process begins with the placement of a tonne bag onto the support frame. Once the bag is secured, the system initiates the feeding mechanism, which gradually empties the bag's contents into the hopper. As the powder flows, level sensors continuously monitor the hopper's fill level, providing real-time data to the control panel. The control system then adjusts the feeding rate to maintain a consistent flow, preventing clogging or overloading. When the hopper reaches the desired fill level, the system automatically stops the feeding process and signals the operator. The entire operation is typically automated, with minimal human intervention required, reducing labor costs and enhancing safety. The system also includes safety features such as emergency stop buttons and interlocks to prevent accidents during operation.
Working Principle of the Powder Conveying System
The working principle of the intelligent tonne bag loading station is based on the principles of mechanical and pneumatic conveying. The system utilizes a combination of gravity and controlled airflow to move the powder from the tonne bag to the processing equipment. Initially, the powder is discharged from the bag into the hopper through a controlled opening. The hopper then feeds the powder into a conveyor system, which may include screw conveyors, pneumatic ducts, or other types of transport mechanisms. The control panel regulates the speed and direction of the conveyor, ensuring that the powder is transported at the optimal rate. The system may also incorporate features such as vibration or agitation to prevent material bridging or caking, which can occur in certain powder types. By maintaining consistent flow and pressure, the system minimizes the risk of blockages and ensures smooth operation. The entire process is monitored and controlled by the system's software, which provides real-time feedback and allows for adjustments as needed. This integrated approach ensures that the powder is handled safely and efficiently, meeting the demands of modern industrial applications.
Advantages of the Intelligent Tonne Bag Loading Station
The intelligent tonne bag loading station offers numerous advantages over traditional manual loading methods. Firstly, it significantly reduces labor costs by automating the entire process, eliminating the need for manual handling of heavy tonne bags. This not only saves time but also minimizes the risk of workplace injuries, such as back strains or falls from height. Secondly, the system enhances operational efficiency by maintaining consistent flow rates and reducing downtime caused by manual adjustments. The automated control system ensures that the powder is transferred at the optimal rate, preventing overfilling or underfilling of the processing equipment. Thirdly, the system improves product quality by minimizing contamination and ensuring uniform material handling. The precise control of the feeding process reduces the risk of material segregation or degradation, which can occur during manual loading. Additionally, the system provides real-time monitoring and data logging, allowing operators to track performance and identify areas for improvement. This data-driven approach helps in optimizing the operation and reducing maintenance costs over time.
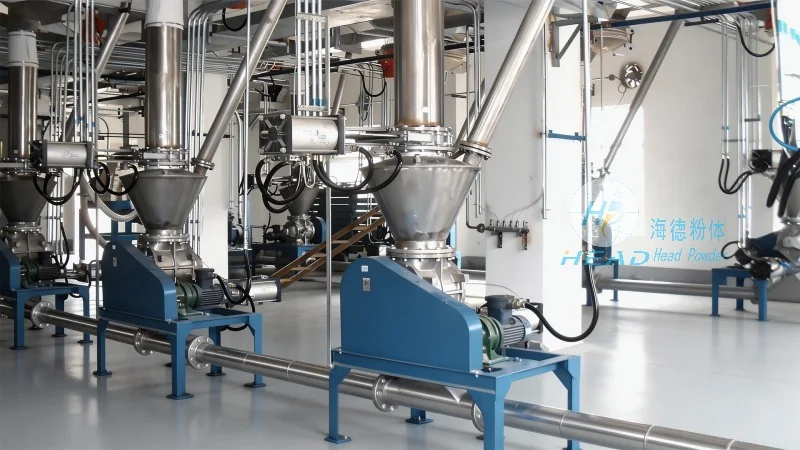
Applications and Industries
The intelligent tonne bag loading station is widely used in various industries that require the handling of bulk powders. In the chemical industry, it is used for loading raw materials such as chemicals, pigments, and additives into reactors or storage tanks. The pharmaceutical industry utilizes the system for handling active pharmaceutical ingredients (APIs) and excipients, ensuring strict adherence to quality and safety standards. The food industry applies the station for processing ingredients like flour, sugar, and spices, maintaining hygiene and preventing contamination. Additionally, the system is used in the agricultural sector for handling fertilizers and pesticides, and in the mining industry for transporting ore powders. The versatility of the system makes it suitable for a wide range of applications, making it a valuable asset for any industrial operation that deals with bulk powders.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. has developed the intelligent tonne bag loading station as a state-of-the-art solution for efficient powder material conveying. By integrating advanced technology and robust design, the system ensures safe, reliable, and automated handling of bulk powders. The operation process and working principle are meticulously engineered to meet the demands of modern industrial applications, providing significant advantages over traditional methods. With its headquarters in Shandong, China, HeadPowder continues to innovate and provide high-quality solutions that enhance operational efficiency and product quality across various industries. The intelligent tonne bag loading station represents a significant advancement in powder handling technology, offering a reliable and efficient solution for businesses seeking to optimize their material handling processes.