

Principle and Working Scene Characteristics of Bin Pump Material Pneumatic Conveying Equipment
Bin pump material pneumatic conveying equipment is a critical component in modern material handling systems, engineered to efficiently transport bulk materials through a pressurized or vacuum system. This equipment serves as a vital solution for moving powders, granules, and other particulate materials over extended distances or within complex processing environments. The core of this technology is the bin pump, which functions as a storage and feeding unit, enabling controlled and consistent material discharge into the conveying pipeline. By integrating advanced fluid dynamics and material flow control, the bin pump ensures reliable and efficient material transport, addressing the diverse needs of industrial applications.
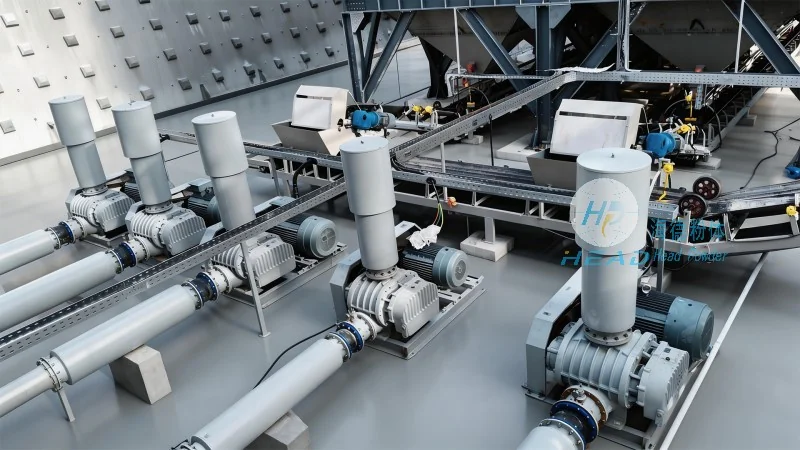
Working Principle of Bin Pump Material Pneumatic Conveying Equipment
The operation of bin pump material pneumatic conveying equipment is grounded in the principles of fluid dynamics and material flow management. The system typically comprises a hopper or bin for material storage, a pump that generates the necessary pressure or vacuum to move the material, and a conveying pipeline that transports the material to the destination. The bin pump, often referred to as a pressure bin or pneumatic bin, utilizes compressed air or a vacuum source to create the force required to propel or draw the material through the pipeline. The material is first fed into the bin pump, where it is mixed with the conveying medium (air or gas). As the pump operates, the material is accelerated and directed through the pipeline, reaching the discharge point at the receiving end. This process ensures that the material is transported in a controlled manner, minimizing segregation and maintaining consistent flow rates. The sealed design of the bin pump prevents material contamination and maintains its integrity throughout the conveying process.
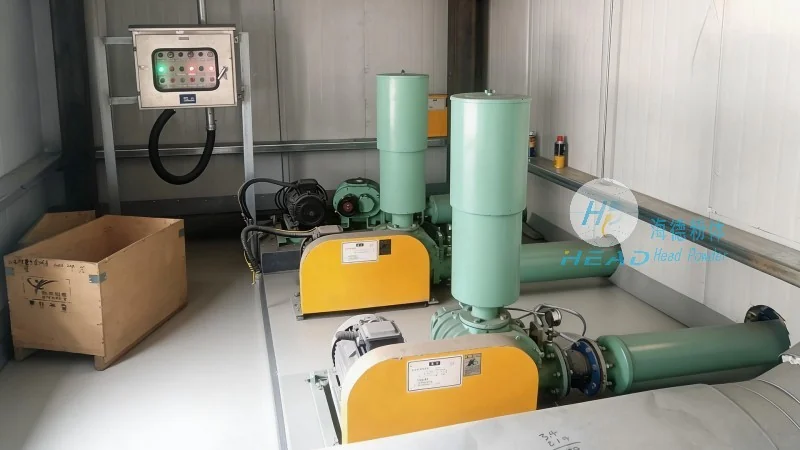
Key Working Scene Characteristics
Bin pump material pneumatic conveying equipment is widely utilized across diverse industrial scenarios, each highlighting its unique advantages. A common application is in the chemical and pharmaceutical industries, where the equipment is employed to transport sensitive materials such as powders and granules without causing degradation or contamination. The sealed system of the bin pump ensures that the material remains protected from external factors, preserving its quality and adhering to stringent regulatory standards. Another prominent application is in the food processing industry, where the equipment handles food-grade powders and ingredients while maintaining strict hygiene protocols. The design of the bin pump, with its easy-to-clean components and sealed construction, makes it suitable for these applications, ensuring compliance with food safety regulations. Additionally, the equipment is used in mining operations to transport ore and other bulk materials from storage bins to processing plants, enhancing operational efficiency and reducing handling time.
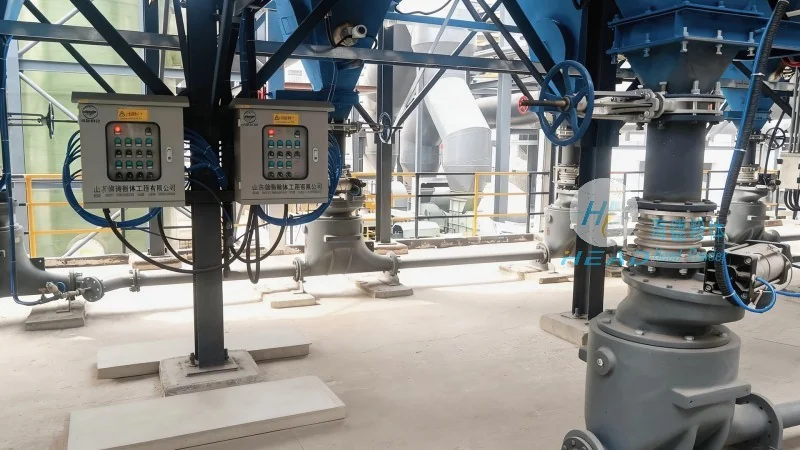
Industrial Applications and Performance
The versatility of bin pump material pneumatic conveying equipment makes it applicable across multiple sectors, including mining, cement production, and agricultural processing. In mining operations, the equipment is used to convey ore and other bulk materials over significant distances, contributing to streamlined production processes. The high capacity and long-distance conveying capabilities of the system make it ideal for such applications, where large volumes of material need to be moved efficiently. In cement production, the equipment is utilized to transport raw materials and finished products, optimizing production schedules and reducing downtime. The consistent flow and low maintenance requirements of the bin pump help to enhance operational efficiency. Furthermore, in agricultural processing, the equipment is employed to handle grain and other agricultural products, facilitating the movement of these materials from storage to processing facilities or distribution centers.
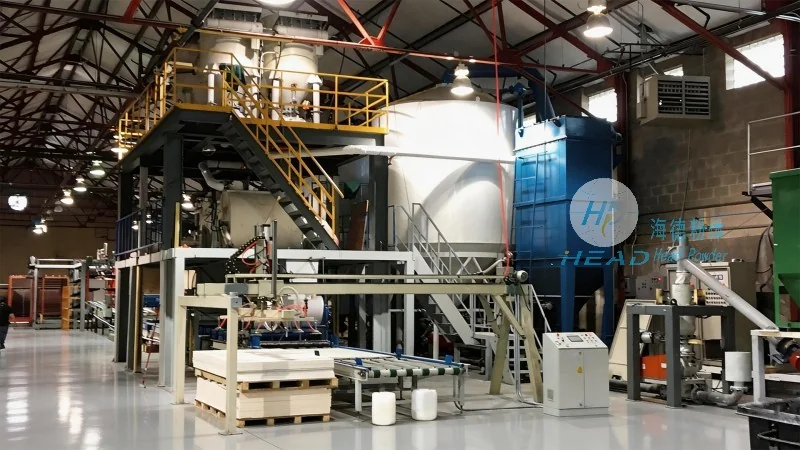
Advantages and Benefits
Bin pump material pneumatic conveying equipment offers several advantages that make it a preferred choice in industrial settings. One primary benefit is its ability to handle a wide range of materials, from fine powders to coarse granules, without causing degradation or segregation. The sealed system prevents contamination, ensuring the material remains pure and free from external particles. Another advantage is the flexibility of the conveying system, allowing for changes in material flow rates and direction without significant modifications. This adaptability makes the bin pump suitable for various production scenarios, from continuous operation to intermittent use. The equipment also provides a clean and safe working environment, as the material is transported through a sealed pipeline, reducing dust and minimizing exposure to hazardous materials. Furthermore, the low maintenance requirements of the bin pump contribute to cost savings and increased operational efficiency, as less time is spent on maintenance and repairs.