

Principles and Working Scene Characteristics of Cement Raw Material Handling Equipment
Efficient and reliable handling of raw materials is a critical component in the cement production process. The equipment used to transport these materials, such as limestone, clay, and iron ore, directly impacts the overall productivity and quality of cement manufacturing. Understanding the principles and operational characteristics of cement raw material handling equipment is essential for optimizing industrial operations.
Introduction to HeadPowder and Their Expertise
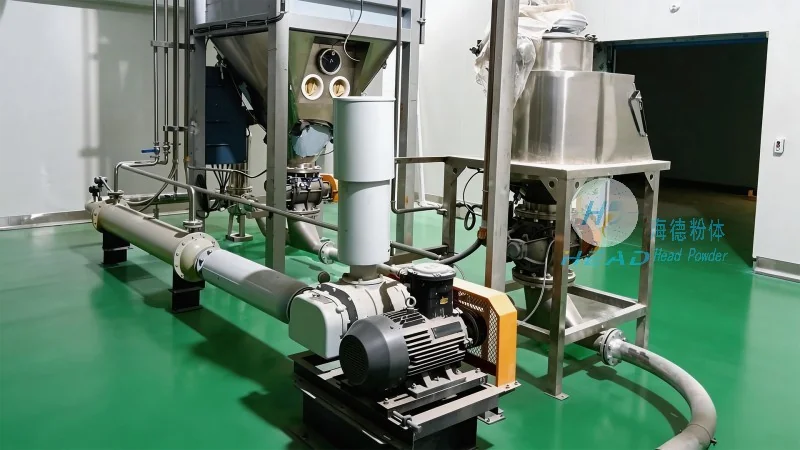
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer based in Shandong, China. With a strong commitment to engineering excellence and customer satisfaction, HeadPowder specializes in the design, development, and supply of advanced material handling solutions tailored for the cement industry. The company's team of experienced engineers and technicians leverages cutting-edge technology to create equipment that meets the demanding requirements of modern cement production facilities.
Principles of Cement Raw Material Handling Equipment
The core principle of cement raw material handling equipment is to transport bulk materials from storage silos or quarries to the grinding and mixing stages of the cement production line. These systems typically include components such as conveyors, feeders, and storage silos, all working in harmony to ensure a continuous flow of raw materials. The equipment is designed to handle various types of raw materials, each with different physical properties, ensuring efficient and safe material transfer. Key principles include material flow optimization, energy efficiency, and minimal material loss during transport. Advanced control systems are integrated to monitor and adjust the flow rate, pressure, and other parameters in real-time, ensuring optimal performance under varying operational conditions.
Working Scene Characteristics of Cement Raw Material Handling Equipment
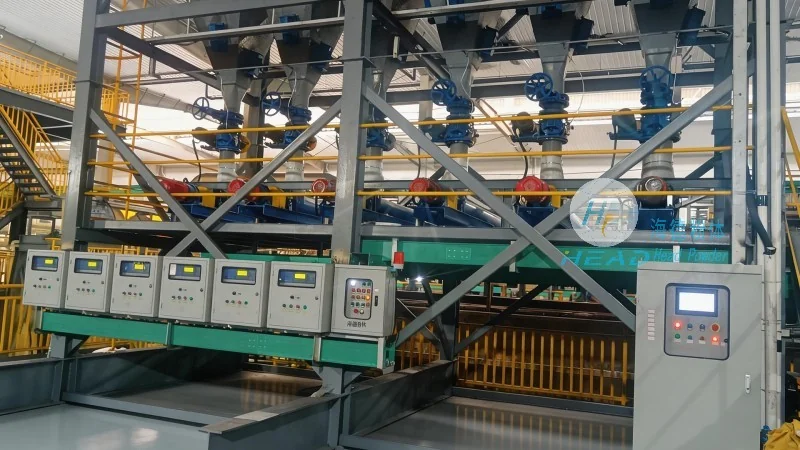
The operational environment of cement raw material handling equipment is characterized by high capacity, continuous operation, and the need for durability in harsh conditions. These systems are designed to operate 24/7, supporting the continuous production cycle of cement plants. The equipment must withstand exposure to dust, moisture, and temperature fluctuations, which are common in cement manufacturing facilities. Additionally, the design emphasizes safety features, such as enclosed structures and emergency stop mechanisms, to protect operators and prevent accidents. The working scene also involves integration with other production equipment, requiring seamless coordination to maintain the production line's efficiency. The equipment's layout and configuration are tailored to the specific site conditions, including available space, material storage locations, and processing requirements. This adaptability ensures that the handling system can be optimized for each individual cement plant, maximizing its effectiveness and reducing operational costs.
Key Features and Advantages of HeadPowder's Solutions
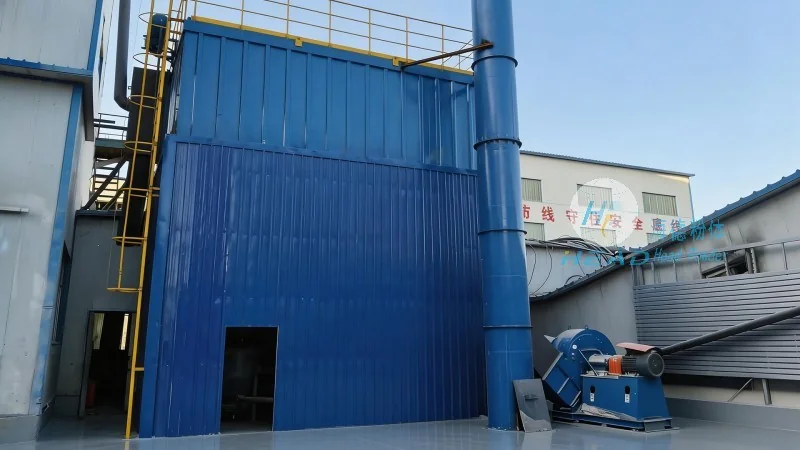
HeadPowder's cement raw material handling equipment is distinguished by several key features that enhance performance and reliability. The use of high-quality materials, such as stainless steel and corrosion-resistant alloys, ensures long-term durability and resistance to wear and tear. Advanced control systems, including PLC (Programmable Logic Controller) and SCADA (Supervisory Control and Data Acquisition) technology, provide precise monitoring and automation of the handling process. This allows for real-time adjustments and predictive maintenance, reducing downtime and maintenance costs. The equipment is also designed for easy maintenance and accessibility, with components that can be quickly inspected and serviced. Additionally, HeadPowder's solutions are energy-efficient, incorporating features like variable speed drives to optimize power consumption and reduce operational costs. The company's focus on customization ensures that each handling system is tailored to the specific needs of the client, whether it's a new plant or an upgrade to an existing facility.
Application and Integration in Cement Production
Cement raw material handling equipment plays a vital role in the overall cement production process. The system is typically integrated with the raw material storage silos, which are used to store limestone, clay, and other raw materials before they are processed. The conveyor system transports these materials from the silos to the grinding mills, where they are reduced to a fine powder. The feeders and other components ensure a consistent flow of material to the grinding mills, preventing blockages and ensuring uniform grinding. The handling equipment also contributes to the overall efficiency of the cement plant by reducing the time and labor required for material transport. By optimizing the flow of raw materials, the equipment helps to maintain a steady production rate, which is crucial for meeting market demand. The integration of HeadPowder's handling solutions with other production equipment, such as grinding mills and kilns, ensures a smooth and continuous operation of the entire production line.