

Principles and Working Scene Characteristics of Feed Material Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of feed processing technology, specializes in the design, manufacturing, and installation of advanced feed material conveying systems. Based in Shandong, China, the company has established itself as a trusted provider of efficient and reliable solutions for the agricultural and animal feed industries. This article delves into the fundamental principles of these systems and highlights the key characteristics of their operational environments, offering insights into how such systems enhance productivity and operational efficiency in feed production facilities.
Understanding the Core Principles of Feed Material Conveying Systems
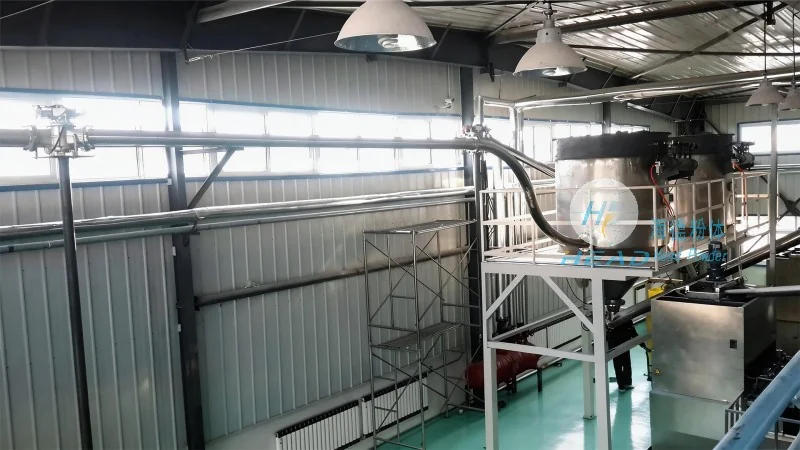
At the heart of any feed material conveying system lies a sophisticated integration of mechanical components and control mechanisms designed to transport bulk materials like grains, pellets, and other feed ingredients from storage silos or processing units to the point of use. The primary principles revolve around the efficient movement of materials with minimal loss, ensuring consistent flow rates and maintaining the integrity of the feed components. Key elements include conveyor belts, screw conveyors, pneumatic systems, and vertical lift mechanisms, each tailored to handle different types of feed materials and operational demands. The system's design typically involves a combination of these components to create a seamless workflow, from raw material intake to the final product distribution.
Key Working Scene Characteristics of Feed Material Conveying Systems
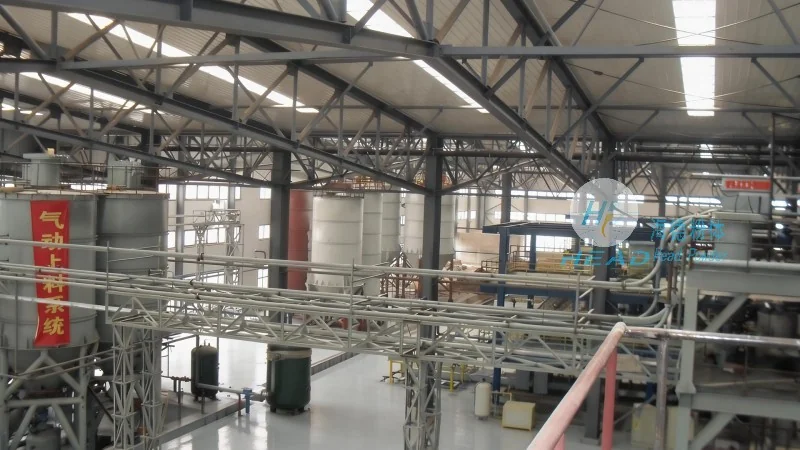
The operational environment of feed material conveying systems is characterized by several critical factors that influence their performance and effectiveness. Firstly, the systems are designed to operate in high-volume production settings, where continuous and uninterrupted material flow is essential to meet the demands of feed mills and animal feed plants. This requires robust construction and durable materials capable of withstanding heavy usage and potential abrasion from the feed components. Secondly, the systems must be adaptable to various feed types, including different particle sizes, moisture contents, and bulk densities. This adaptability is achieved through adjustable speed controls, variable pitch screw conveyors, and flexible hose or tube configurations in pneumatic systems. Thirdly, the working environment often involves stringent hygiene and sanitation requirements, especially in facilities producing animal feed. Therefore, many conveying systems incorporate features such as easy-to-clean surfaces, sealed components, and non-stick coatings to prevent contamination and ensure compliance with industry standards. Additionally, the systems are engineered for energy efficiency, utilizing advanced motor controls and optimized conveyor designs to minimize power consumption while maximizing throughput.
Application-Specific Features and Benefits
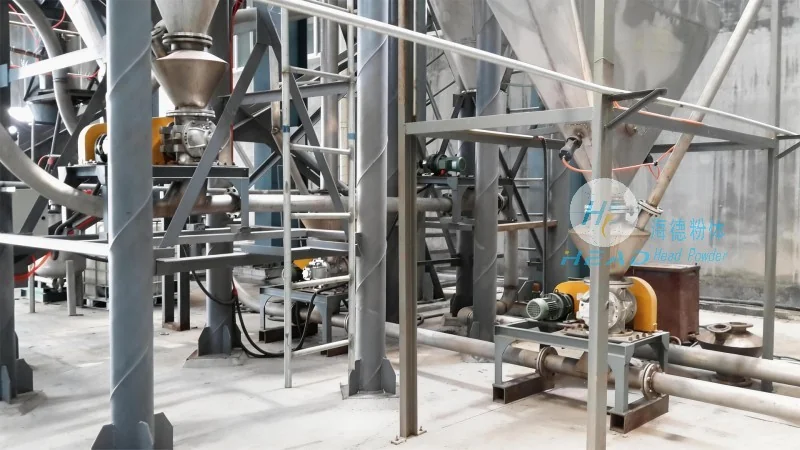
Feed material conveying systems from Shandong HeadPowder Engineering Co., Ltd. are tailored to meet the specific needs of diverse applications within the feed industry. For instance, in large-scale feed mills, the systems may include multiple parallel conveyor lines to handle different raw materials simultaneously, ensuring a smooth transition from raw material storage to the mixing and pelleting stages. In smaller feed production facilities, compact and modular conveying systems are preferred, allowing for easy installation and integration with existing equipment. The company's expertise lies in customizing these systems to fit the unique layout and operational requirements of each client, ensuring optimal performance and cost-effectiveness. Moreover, the systems are designed to enhance safety in the workplace, with features such as emergency stop buttons, protective guards, and automated monitoring systems that alert operators to any deviations in the material flow or system performance.
Conclusion and Operational Excellence
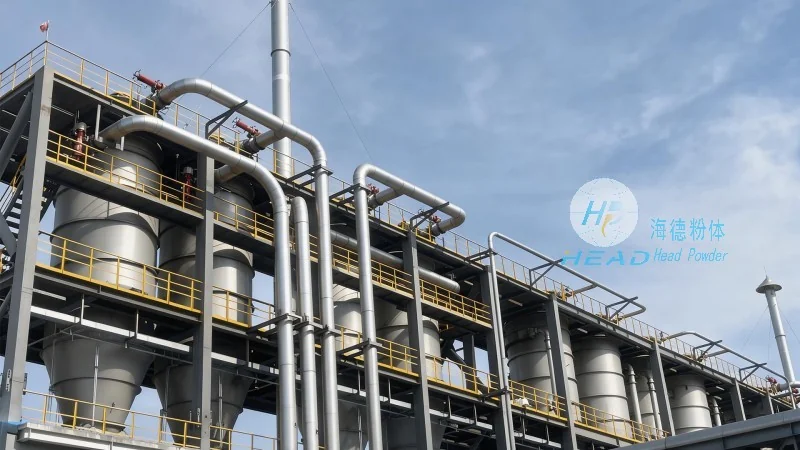
In conclusion, feed material conveying systems are integral to the efficient operation of feed production facilities, and their design and implementation are critical to achieving high productivity and product quality. Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in mechanical engineering and material handling to provide systems that adhere to the highest standards of performance, reliability, and safety. By understanding the core principles and working scene characteristics of these systems, feed manufacturers can make informed decisions to enhance their operational efficiency and meet the evolving demands of the animal feed market. The company's commitment to innovation and customer-centric solutions ensures that its feed material conveying systems remain at the forefront of the industry, delivering sustainable and effective solutions for the future of feed processing.