

Principle and Working Scene Characteristics of Cement Dry Ash Powder Conveying System
Cement dry ash powder conveying systems are critical components in industrial processes, particularly in facilities dealing with the handling and transportation of dry powders such as cement ash. These systems are designed to efficiently move bulk materials from one location to another while maintaining the integrity and quality of the material. The core principle behind these systems involves the use of specialized equipment that can handle the unique properties of dry cement ash, ensuring minimal dust generation and optimal material flow. By understanding the underlying principles and typical working scenarios, users can better appreciate the importance and functionality of such systems in modern industrial applications. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality conveying systems tailored to meet the specific needs of industrial clients.
Core Principles of Dry Ash Powder Conveying
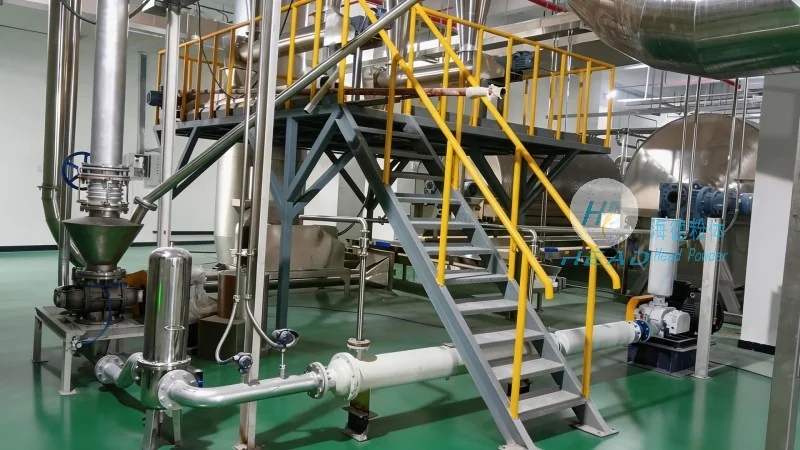
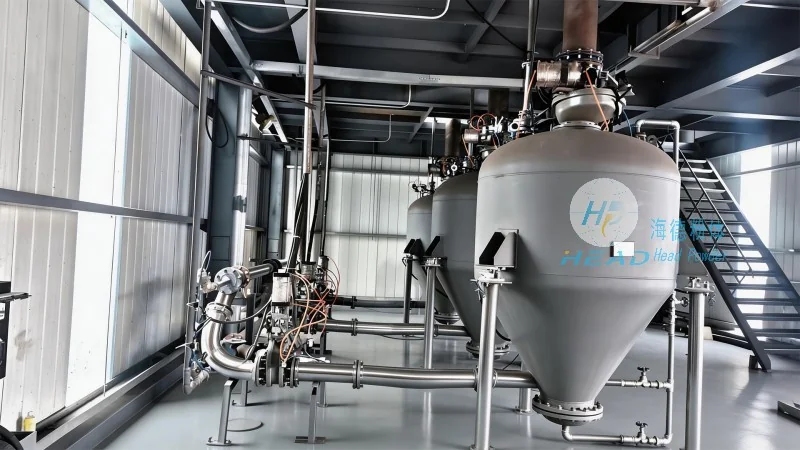
The fundamental principle of cement dry ash powder conveying systems revolves around the use of pneumatic or mechanical methods to transport dry powders. Pneumatic conveying systems utilize air pressure to move the material through a pipeline, while mechanical systems rely on positive displacement or screw conveyors. For cement ash, which is often fine and abrasive, pneumatic systems are commonly preferred due to their ability to handle high volumes and minimize material degradation. The system typically includes a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the destination. The air flow is carefully regulated to ensure consistent material transport without causing excessive pressure drops or particle separation. Key components like rotary valves, filters, and pressure vessels are integral to maintaining system efficiency and safety. Shandong HeadPowder Engineering Co., Ltd. incorporates advanced control technologies to optimize the performance of these components, ensuring reliable operation in demanding environments.
Working Scene Characteristics
The working scene characteristics of cement dry ash powder conveying systems vary based on the specific industrial application. In power plants, for example, these systems are used to transport fly ash from the boiler to storage silos or for reuse in cement production. The environment in such settings is often characterized by high temperatures and dust, requiring robust equipment that can withstand harsh conditions. The conveying distance and material flow rate are critical factors that influence the system design, with longer distances necessitating higher air pressure and more powerful fans. In construction material plants, the systems may be used to blend cement ash with other raw materials, where precise control over the material flow is essential for maintaining the quality of the final product. The working scene also includes considerations for space constraints, as these systems are often installed in existing facilities with limited room for expansion. Additionally, the need for dust control and environmental compliance is a major factor, as modern systems are equipped with advanced filtration and emission control measures to meet regulatory standards. Shandong HeadPowder Engineering Co., Ltd. designs systems that comply with international environmental regulations, ensuring clients operate within legal and sustainable frameworks.
Applications and Industry Impact
Cement dry ash powder conveying systems have a significant impact on various industries, particularly in the cement and power sectors. By efficiently handling large volumes of dry ash, these systems contribute to improved operational efficiency and reduced downtime. The ability to transport material over long distances without the need for manual handling reduces labor costs and enhances workplace safety. Moreover, the systems help in reducing the environmental impact by minimizing the release of dust and particulate matter into the atmosphere. In the context of sustainable development, the reuse of cement ash in construction materials is becoming increasingly important, and these conveying systems play a vital role in facilitating this process. Shandong HeadPowder Engineering Co., Ltd. has been at the forefront of developing advanced conveying solutions that support these sustainable practices, ensuring that clients can achieve both operational excellence and environmental compliance. The company’s expertise in material handling technology has enabled the integration of cement ash into concrete production, leading to cost savings and reduced reliance on virgin raw materials.
Conclusion
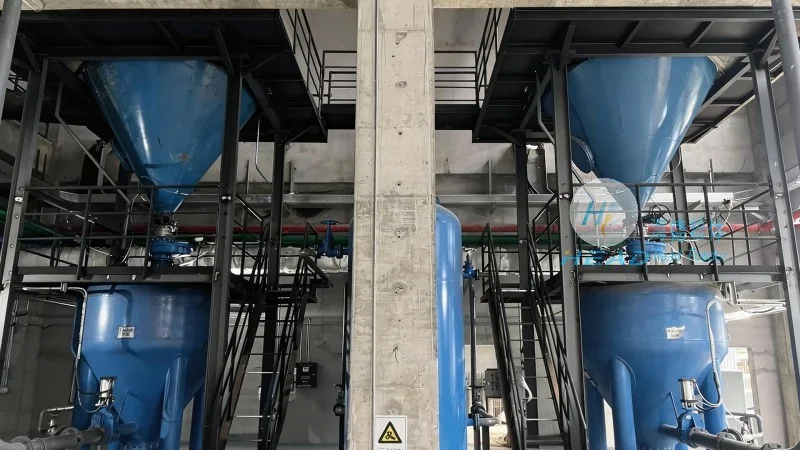
In conclusion, cement dry ash powder conveying systems are essential for the efficient and safe handling of dry powders in industrial settings. The principles of pneumatic and mechanical conveying, combined with specialized components, enable the reliable transport of cement ash. The working scene characteristics, influenced by factors such as application, distance, and environmental requirements, dictate the system design and operational parameters. As industries continue to prioritize efficiency, sustainability, and safety, the importance of efficient dry ash powder conveying systems will only grow. The continued development and optimization of cement dry ash powder conveying systems will undoubtedly contribute to the advancement of related industries and the broader goals of sustainable industrial practices. Shandong HeadPowder Engineering Co., Ltd. remains committed to delivering innovative solutions that meet the evolving needs of its clients, ensuring that the principles of effective dry ash powder conveying are applied across diverse industrial applications.