

Principle and Working Scene Characteristics of Fine Sand and Stone Powder Conveying Systems
HeadPowder, a leading enterprise based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced powder conveying systems tailored for fine sand and stone materials. The company's expertise lies in developing efficient solutions that address the unique challenges of transporting fine particulate materials, ensuring optimal performance in various industrial applications.
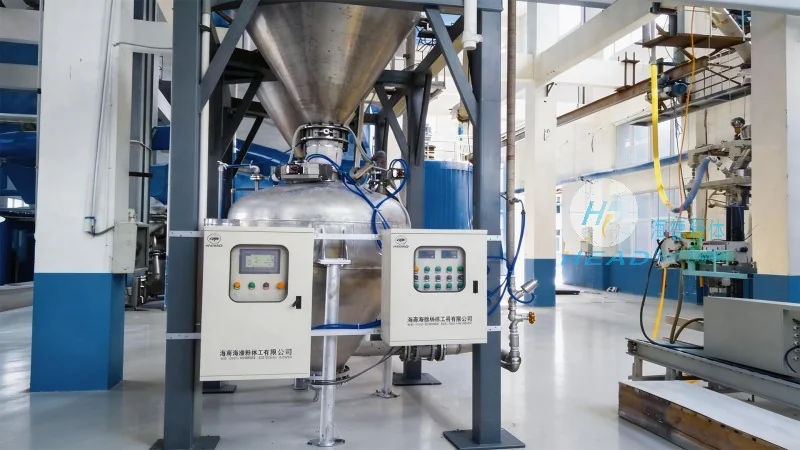
System Principle: How Fine Sand and Stone Powder Conveying Systems Operate
The core principle of fine sand and stone powder conveying systems revolves around the efficient movement of fine particulate materials from a source to a destination. These systems typically employ a combination of mechanical and pneumatic technologies to achieve reliable and continuous material transport. For instance, in pneumatic conveying systems, compressed air is used to create a flow that carries the fine sand and stone particles through a pipeline. This method is particularly effective for materials that are prone to dusting or require low contamination levels. Mechanical conveying systems, on the other hand, utilize components such as screw conveyors, belt conveyors, or bucket elevators to move the material. The choice of system depends on factors like material properties, distance, and required throughput. The system's design ensures that the material is handled gently, minimizing breakage and degradation, which is crucial for maintaining the quality of fine sand and stone products.
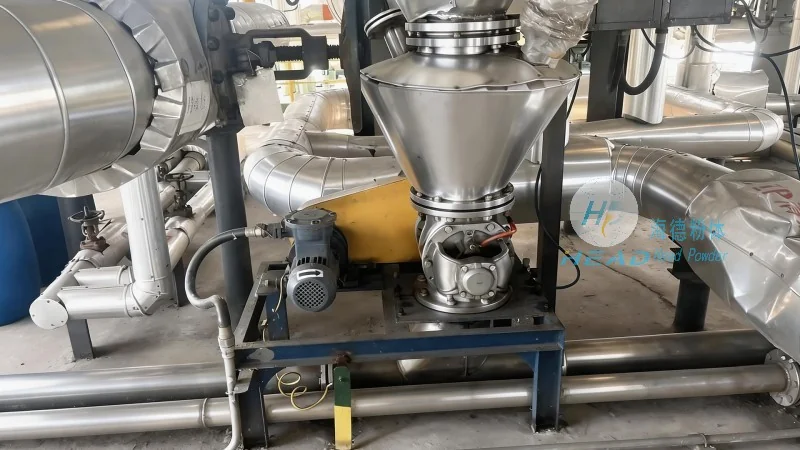
Working Scene Characteristics: Applications and Operational Environments
Fine sand and stone powder conveying systems are widely utilized across multiple industrial sectors, each presenting distinct operational environments and requirements. In the construction industry, these systems are essential for transporting sand, gravel, and other fine aggregates from storage silos to mixing plants or batching stations. The systems must operate reliably under high throughput conditions, often handling large volumes of material with minimal downtime. In mining operations, the conveying of fine ore particles is critical for processing and refining. Here, the systems need to handle abrasive materials and maintain consistent flow rates to support downstream processing equipment. Additionally, in the chemical and pharmaceutical industries, where fine powders are used for manufacturing, the conveying systems must adhere to strict hygiene and contamination control standards. The working scene characteristics also include considerations of space constraints, as many industrial facilities have limited room for large conveying equipment. Advanced systems are designed to be compact and modular, allowing for installation in confined areas while still delivering high performance. Environmental factors, such as temperature and humidity, also play a role in system design, as they can affect the material's properties and the system's efficiency. For example, in outdoor applications, systems may include weather-resistant components to ensure continuous operation under varying conditions.
Key Advantages and Technical Features
HeadPowder's fine sand and stone powder conveying systems offer several key advantages that make them ideal for demanding industrial applications. One of the primary benefits is the high efficiency in material transport, with minimal energy consumption compared to traditional methods. The systems are designed to handle a wide range of particle sizes, from very fine powders to coarse sand, ensuring versatility in application. Another advantage is the low maintenance requirements, as advanced materials and components are used to reduce wear and tear. This leads to lower operational costs and increased system longevity. The systems also provide precise control over material flow, allowing for accurate dosing and batching, which is critical in processes like concrete mixing or chemical formulation. In terms of safety, the systems are equipped with safety features such as overpressure relief valves and material flow indicators, ensuring safe operation and preventing accidents. The modular design of the systems allows for easy integration into existing production lines, with minimal disruption to ongoing operations. This flexibility is particularly valuable for companies undergoing expansion or upgrading their facilities. Furthermore, the systems are designed with scalability in mind, enabling them to be expanded or modified as production needs change over time. This adaptability ensures long-term value and investment protection for the end-user.
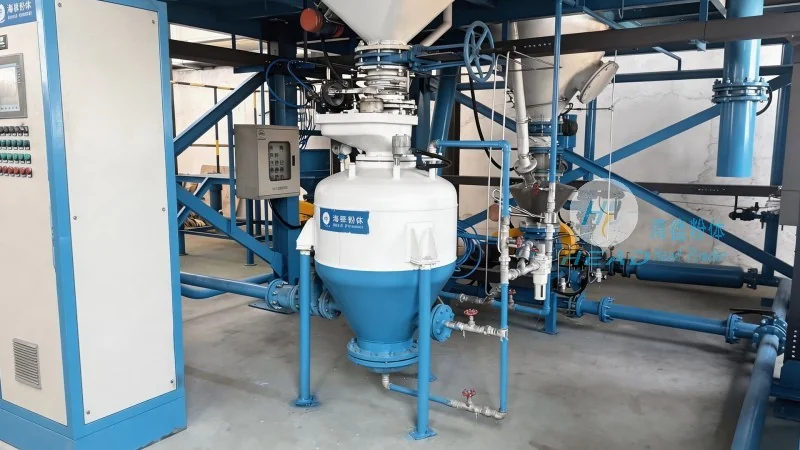
Application Examples and Case Studies
Real-world applications of fine sand and stone powder conveying systems demonstrate their effectiveness in various industrial settings. For instance, in a large-scale concrete production plant, HeadPowder's system was installed to transport fine sand from a storage silo to a batching plant. The system was designed to handle 500 tons per hour of material, with a conveying distance of 200 meters. The pneumatic conveying system used in this case ensured that the fine sand was transported without any dusting or degradation, maintaining the quality of the material. The system's performance was monitored continuously, with real-time data on flow rates and pressure, allowing for immediate adjustments if any issues arose. In another application, a mining company utilized a mechanical screw conveyor system to transport fine ore particles from a crusher to a processing plant. The system was designed to handle abrasive materials, with heavy-duty components that could withstand the wear and tear. The system's efficiency was evident in the consistent flow rates and minimal downtime, contributing to increased productivity in the mining operation. These case studies highlight the reliability and performance of HeadPowder's conveying systems, which are tailored to meet the specific needs of each application.