

Working Principle and Features of Potassium Fertilizer Powder Conveyors
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced powder handling solutions. This article delves into the working principle and key features of our potassium fertilizer powder conveyors, highlighting how these systems enhance efficiency and reliability in fertilizer processing operations.
Company Background and Expertise
Shandong HeadPowder Engineering Co., Ltd. is a reputable company dedicated to engineering and manufacturing high-quality powder conveying equipment. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the fertilizer industry. Our headquarters is located in Shandong, China, where we leverage local resources and expertise to develop cutting-edge solutions tailored to the unique demands of fertilizer processing.
Understanding the Working Principle of Potassium Fertilizer Powder Conveyors
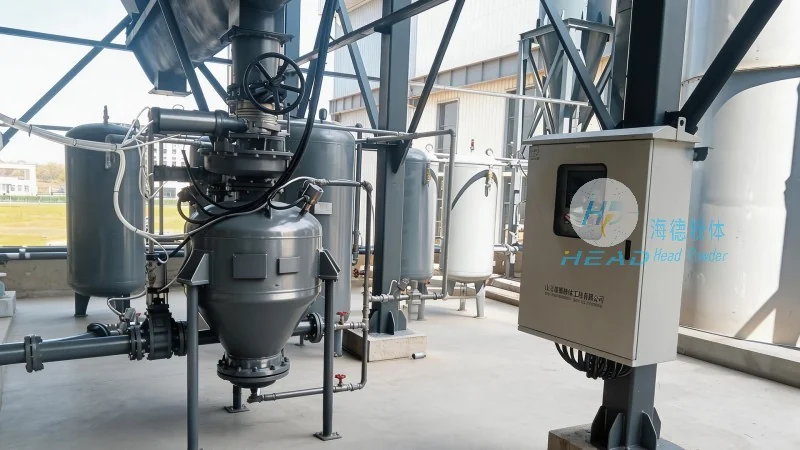
The working principle of a potassium fertilizer powder conveyor involves the efficient transport of bulk powder materials, such as potassium-based fertilizers, from one location to another within a processing facility. These systems typically utilize mechanical components like screw conveyors, pneumatic conveyors, or bucket elevators to move the powder. The conveyor mechanism is designed to handle the specific properties of potassium fertilizers, including their particle size, density, and flow characteristics. By understanding the internal mechanisms, users can better appreciate how these systems ensure consistent and reliable material transfer.
Key Features of Potassium Fertilizer Powder Conveyors
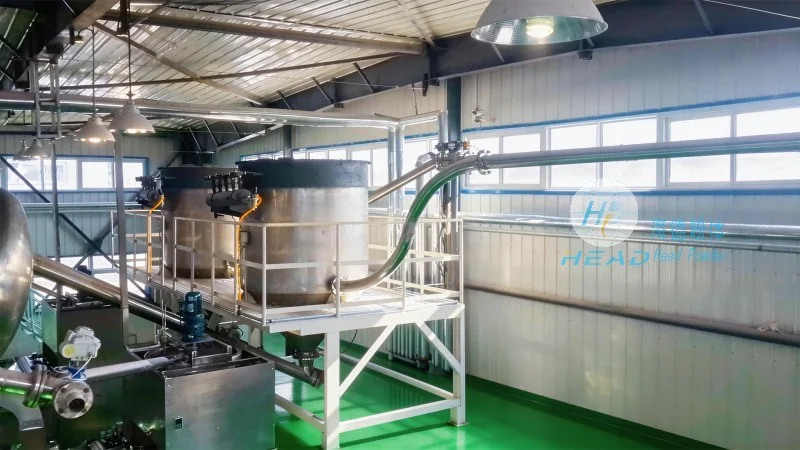
HeadPowder's potassium fertilizer powder conveyors are equipped with several advanced features that set them apart in the industry. One notable feature is the robust construction, which is built to withstand the abrasive nature of potassium fertilizers and the demanding conditions of continuous operation. The conveyors are also designed with adjustable speed controls, allowing operators to optimize the flow rate based on production needs. Additionally, these systems incorporate safety mechanisms, such as overload protection and emergency stop buttons, to ensure operational safety. Another key feature is the integration of cleaning and maintenance systems, which help maintain the conveyor's performance and extend its service life. The conveyors are also designed for easy integration with existing processing lines, minimizing downtime during installation and operation.
Benefits of Using Potassium Fertilizer Powder Conveyors
Implementing a potassium fertilizer powder conveyor offers numerous benefits for fertilizer processing facilities. Firstly, these systems significantly improve operational efficiency by reducing manual handling and labor costs. The automated transport of bulk materials streamlines the production process, allowing for higher throughput and better resource utilization. Secondly, the conveyors enhance product quality by minimizing material degradation and contamination during transport. The controlled environment and gentle handling of the powder help preserve the nutrient content and physical properties of the fertilizer. Thirdly, the systems contribute to workplace safety by eliminating the need for manual lifting and moving of heavy bags or containers. This reduces the risk of injuries and improves overall safety in the facility. Finally, the conveyors provide cost savings through reduced energy consumption and lower maintenance requirements compared to traditional manual handling methods.
Application Scenarios and Industry Use Cases
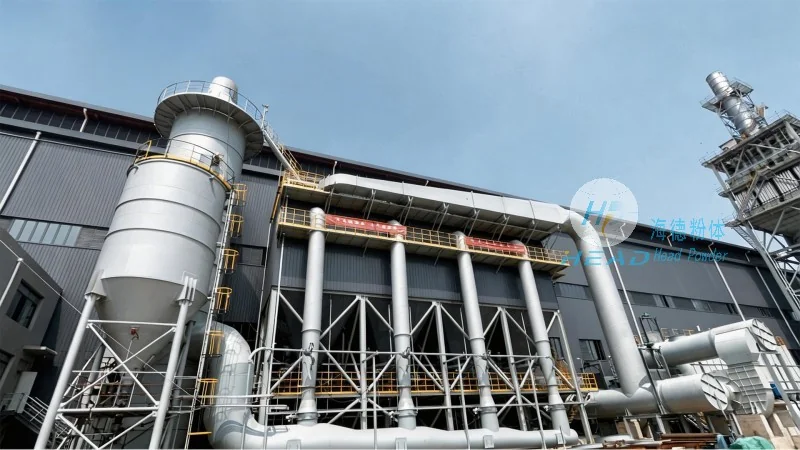
Potassium fertilizer powder conveyors are widely used in various stages of fertilizer production and distribution. In the manufacturing process, these systems are employed to transport raw materials, such as potassium chloride or sulfate, from storage silos to mixing and granulation units. During the packaging stage, the conveyors efficiently move finished fertilizer products from the production line to storage silos or loading areas. Additionally, they are used in bulk handling operations, such as loading trucks or ships with fertilizer, ensuring a smooth and continuous supply chain. The versatility of these conveyors makes them suitable for both large-scale industrial operations and smaller processing facilities, adapting to the specific needs of each application.
Conclusion and Contact Information
HeadPowder's potassium fertilizer powder conveyors represent a reliable and efficient solution for the transportation of potassium-based fertilizers. By leveraging advanced engineering and robust design, these systems enhance productivity, improve product quality, and ensure operational safety. For more information or to explore how our conveyors can benefit your fertilizer processing operations, please contact us at our headquarters in Shandong, China. HeadPowder is committed to providing tailored solutions that meet the evolving needs of the fertilizer industry.