

[WOKING PRINCIPLE AND FEATURES OF DUST COLLECTION POWDER CONVEYING SYSTEMS]
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design and manufacturing of dust collection powder conveying systems. Based in Shandong, China, the company provides advanced solutions for handling and transporting fine powders, including dust collection applications. This article explores the working principle and key features of their powder conveying lines.
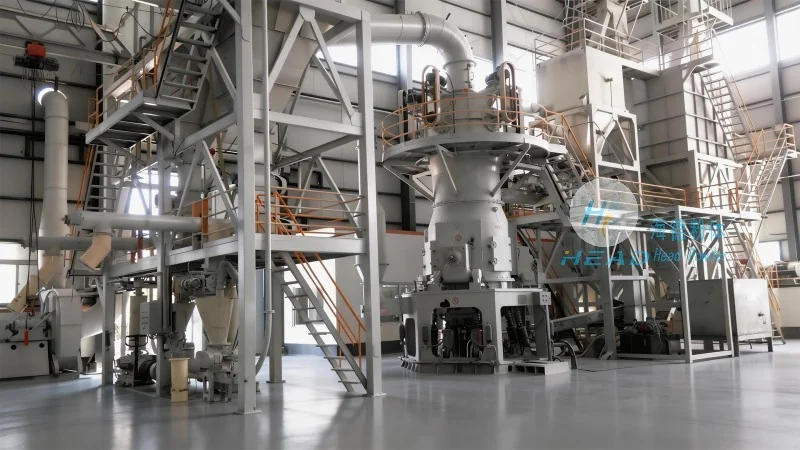
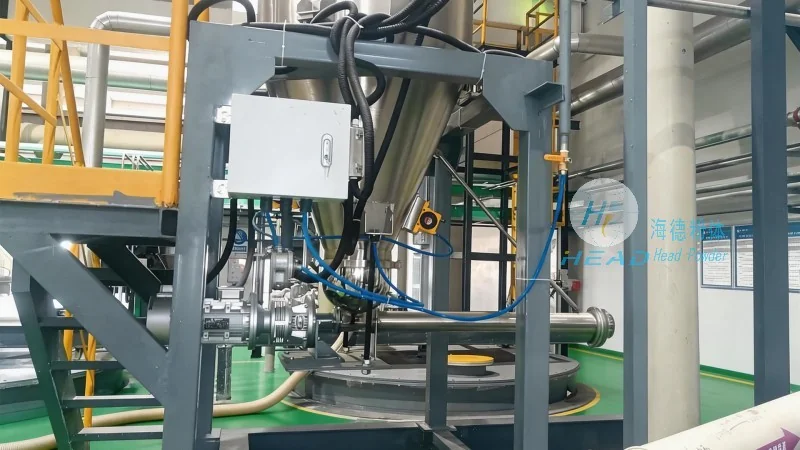
Working Principle of Dust Collection Powder Conveying Lines
The dust collection powder conveying line typically operates through a combination of components that ensure efficient material transport while maintaining dust control. The system begins with the collection of fine powders, often from industrial processes such as grinding or crushing. These powders are then transferred through a network of pipes or hoses, utilizing various methods like pneumatic conveying or mechanical screw conveyors. The core mechanism involves the use of air or mechanical force to move the powder from the source to the destination, ensuring minimal loss and contamination. The process is designed to maintain a consistent flow rate, which is critical for maintaining system efficiency and preventing blockages. Additionally, the system incorporates dust filtration and separation components to ensure that the transported material remains clean and free from impurities. The control system, often integrated with sensors and automation, monitors the flow and adjusts parameters as needed to optimize performance.
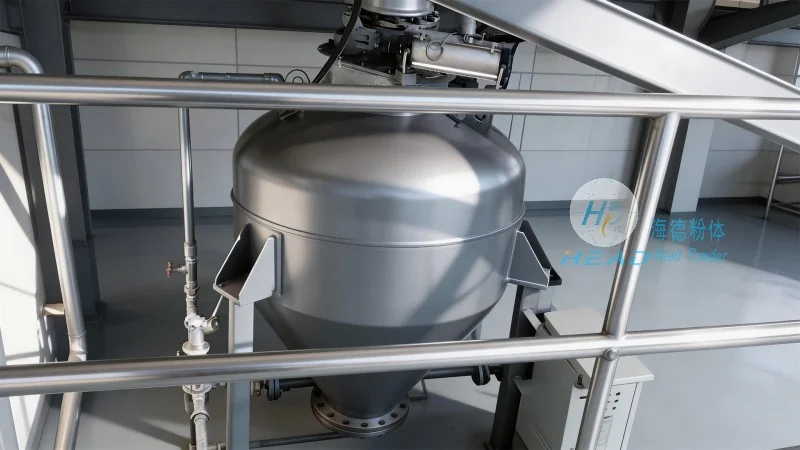
Key Features of Dust Collection Powder Conveying Systems
HeadPowder's dust collection powder conveying lines are characterized by several distinct features that enhance their functionality and reliability. One of the primary features is the integration of dust collection technology, which ensures that the entire process is dust-tight and compliant with environmental regulations. The systems are designed to handle a wide range of powder types, from fine to coarse, with varying moisture content and particle sizes. This versatility makes them suitable for diverse industrial applications, including pharmaceuticals, food processing, and chemical manufacturing. Another notable feature is the energy efficiency of the conveying process. By optimizing air pressure and flow rates, the systems minimize energy consumption while maintaining high throughput. The modular design of the lines allows for easy installation and maintenance, reducing downtime and operational costs. Furthermore, the systems are equipped with advanced monitoring and control capabilities, enabling real-time tracking of material flow and system performance. This allows for quick identification and resolution of any issues, ensuring continuous operation. The durability of the components, such as high-quality materials and robust construction, contributes to the long service life of the equipment, providing a reliable solution for long-term use.
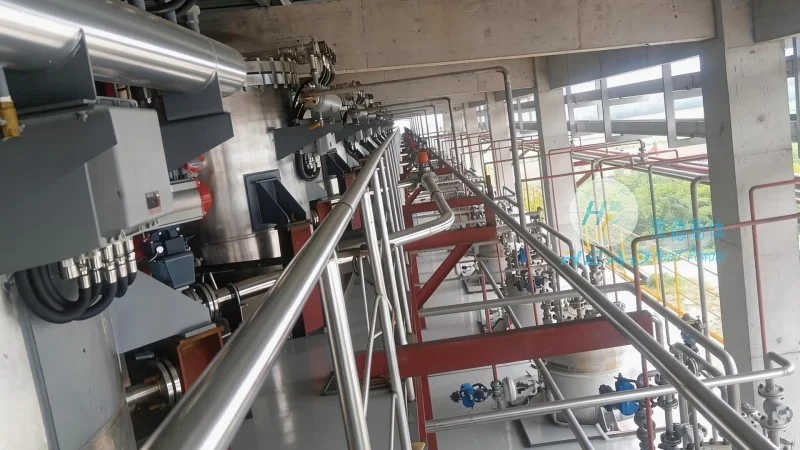
Application and Performance Benefits
The dust collection powder conveying systems from headpowder offer significant advantages in terms of operational efficiency and safety. By integrating dust collection directly into the conveying process, the systems reduce the risk of airborne contamination, improving workplace safety and meeting regulatory standards. The consistent and reliable transport of powders ensures that downstream processes, such as mixing or packaging, operate smoothly without interruptions. The energy-efficient design helps reduce operational costs over time, making the systems a cost-effective choice for industrial operations. Additionally, the modular and scalable nature of the systems allows for easy expansion or integration with existing facilities, providing flexibility for growing businesses. The advanced control and monitoring features enhance operational transparency, allowing for data-driven decisions to optimize performance and reduce maintenance needs. Overall, these systems provide a comprehensive solution for handling fine powders while maintaining environmental and safety standards.