

Working Principle and Features of Wheat Starch Pneumatic Conveying Equipment
Wheat starch pneumatic conveying equipment is a specialized system designed for the efficient and safe transport of wheat starch and related powders. This equipment is widely used in the food processing and starch production industries, where reliable material handling is crucial for maintaining product quality and operational efficiency.
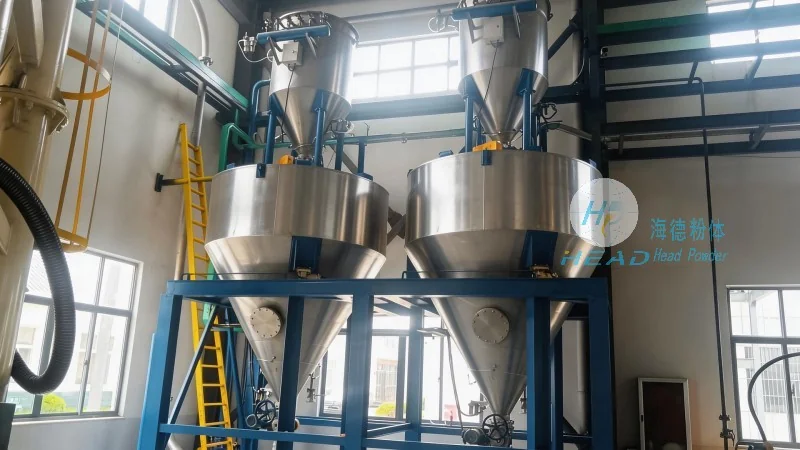
Introduction to Wheat Starch Pneumatic Conveying Equipment
Wheat starch pneumatic conveying equipment, as the name suggests, utilizes air pressure to move wheat starch and other fine powders through a pipeline system. This method offers several advantages over traditional mechanical conveying systems, such as reduced product contamination, lower maintenance requirements, and the ability to handle sensitive materials without damage.
Working Principle of Wheat Starch Pneumatic Conveying Equipment
The core mechanism of wheat starch pneumatic conveying equipment involves the creation of a pressure differential between the inlet and outlet of the conveying line. A fan or blower generates a high-velocity air stream that draws the wheat starch particles into the pipeline. The air stream then transports the material to the destination point, where a separator or cyclone separates the starch from the air before it is released into the atmosphere or recirculated. The system typically operates under either positive pressure (pressure conveying) or negative pressure (suction conveying), depending on the specific application and material characteristics.
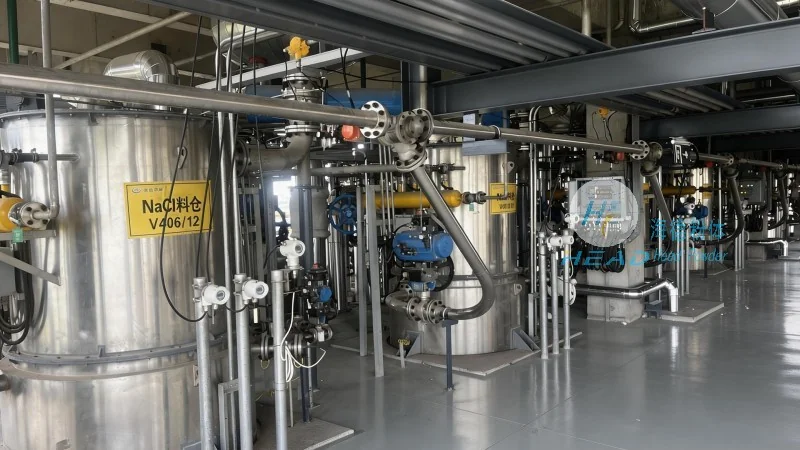
Key Features of Wheat Starch Pneumatic Conveying Equipment
Several key features make wheat starch pneumatic conveying equipment an ideal choice for starch processing facilities. First, it provides a hygienic and clean conveying method, which is essential for food-grade products like wheat starch. The enclosed pipeline system prevents dust and contamination from entering the environment, ensuring compliance with food safety regulations. Second, the equipment offers high efficiency in material transport, with the ability to move large volumes of starch over long distances with minimal energy consumption. Third, it is highly flexible, allowing for easy integration into existing production lines and adaptation to varying production rates. Additionally, the system is relatively low in maintenance, as it has fewer moving parts compared to mechanical conveyors, reducing downtime and operational costs.
Technical Specifications and Design Considerations
When selecting a wheat starch pneumatic conveying system, several technical specifications and design factors must be considered. The system's capacity, determined by the air flow rate and pipeline diameter, should match the production requirements of the starch facility. The material of construction is critical, as it must be compatible with the starch and any cleaning agents used. Common materials include stainless steel, which offers corrosion resistance and easy cleaning. The design also includes features such as air filters to prevent dust from entering the system and moisture separators to remove excess water from the starch, ensuring the final product remains dry and free from clumping. The control system, often equipped with sensors and automation, allows for precise monitoring and adjustment of the conveying process, enhancing operational control and safety.
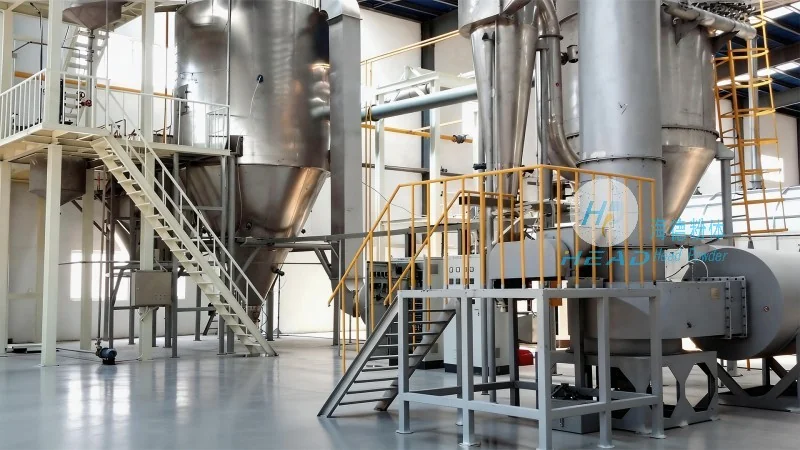
Applications and Benefits in Starch Production
Wheat starch pneumatic conveying equipment is extensively used in various stages of starch production, from raw material handling to final product packaging. In the initial stages, it efficiently transports wheat flour or other raw materials into the processing plant. During the starch extraction process, the equipment moves the extracted starch slurry or powder through the production line. The system's ability to handle fine powders without clogging or damaging the particles is particularly valuable in these applications. The benefits extend beyond material transport; the equipment contributes to overall production efficiency by reducing labor costs associated with manual handling and minimizing product loss due to spillage or contamination.
Conclusion and Company Information
Wheat starch pneumatic conveying equipment is a vital component in modern starch production facilities, offering a reliable, efficient, and hygienic method for material handling. The working principle, which relies on air pressure to transport fine powders, combined with its key features such as low contamination risk and high flexibility, makes it an indispensable tool for maintaining high product quality and operational standards. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of starch producers. With a focus on quality and customer satisfaction, the company ensures that its equipment meets the highest industry standards, supporting the success of starch processing operations worldwide.