

Working Principle and Features of Coke Particle Pneumatic Conveyors
For industrial applications involving the transport of coke particles, efficient and reliable equipment is essential. The coke particle pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., offers a sophisticated solution for material handling. This equipment is designed to handle coke granules with precision, ensuring minimal loss and optimal performance in various industrial settings.
Working Principle of Coke Particle Pneumatic Conveyors
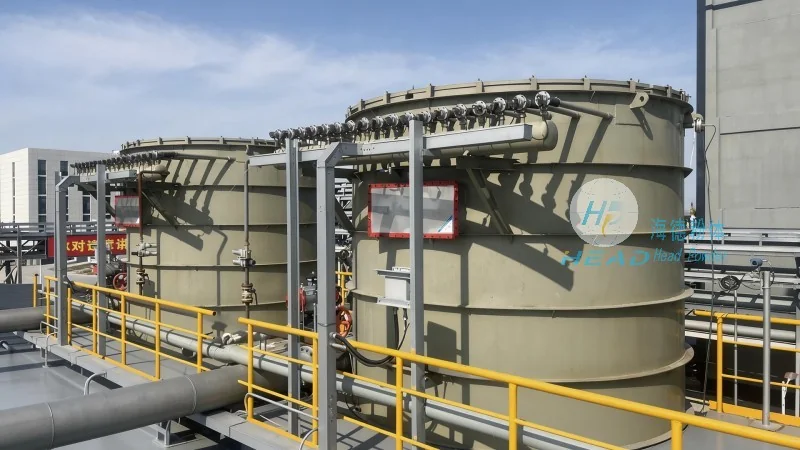
The operation of coke particle pneumatic conveyors is based on the principle of pneumatic transport, where material is moved through a pipeline using a pressurized or vacuum air stream. In the system, coke particles are introduced into a hopper or feeder, where they are then drawn or pushed into the conveying line by the air flow. The air stream, typically generated by a blower or fan, creates a pressure differential that propels the particles through the pipeline. The system may utilize either positive pressure (where air is forced into the line) or negative pressure (where air is drawn out), depending on the specific application requirements. The design of the conveying line, including the diameter, length, and bends, is carefully engineered to minimize pressure drop and ensure smooth particle movement. Additionally, the system incorporates components such as cyclones or filters to separate the coke particles from the air stream at the discharge end, allowing for clean material collection.
Key Features of Coke Particle Pneumatic Conveying Equipment
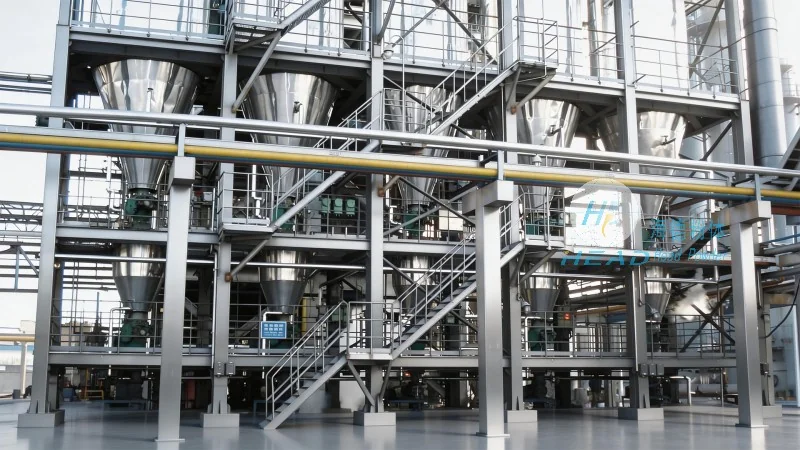
Shandong HeadPowder Engineering Co., Ltd. has integrated several advanced features into their coke particle pneumatic conveying systems to enhance performance and reliability. One of the primary features is the ability to handle a wide range of coke particle sizes and densities, making it suitable for various industrial processes. The equipment is also designed for low maintenance, with components that are easy to access and replace, reducing downtime and operational costs. Another notable feature is the energy efficiency of the system, which utilizes optimized air flow and pressure control to minimize energy consumption while maintaining high conveying rates. The system also includes safety features such as pressure relief valves and overheat protection, ensuring safe operation in industrial environments. Furthermore, the equipment is constructed from durable materials, such as stainless steel or corrosion-resistant alloys, to withstand the harsh conditions associated with coke handling and prevent material degradation.
Application Benefits and Performance
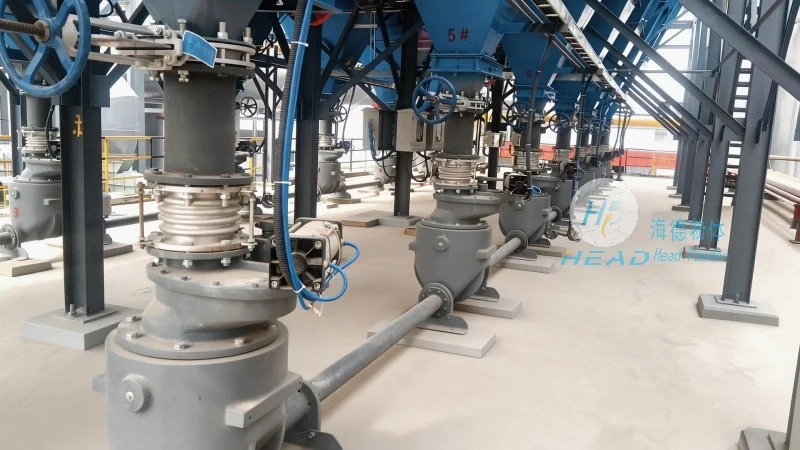
The coke particle pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers several benefits for industrial operations. By eliminating the need for mechanical components like belts or chains, the system reduces the risk of mechanical failure and maintenance requirements. The pneumatic transport method also minimizes product contamination, as the particles are not in direct contact with moving parts. Additionally, the system provides flexibility in material handling, allowing for horizontal, vertical, or mixed-direction conveying, depending on the layout of the industrial facility. The high conveying capacity of the equipment enables efficient material transfer over long distances, improving overall production efficiency. The system's ability to handle abrasive materials like coke particles is enhanced by the use of wear-resistant liners and components, extending the lifespan of the equipment and reducing replacement costs.
Conclusion and Company Information
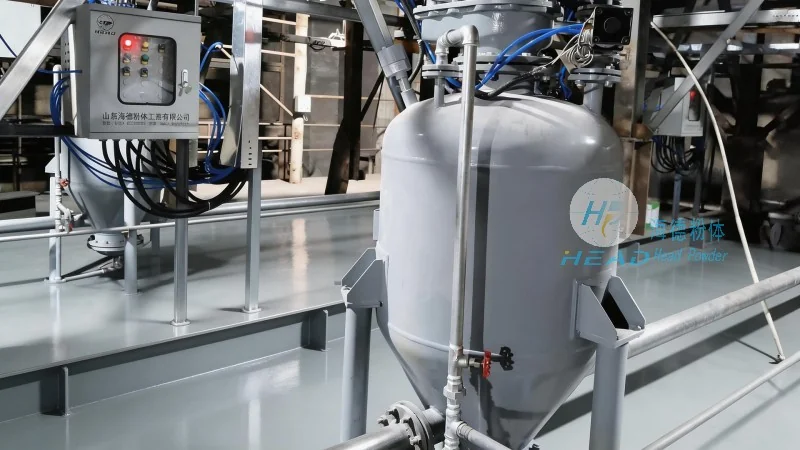
Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of coke particle pneumatic conveying equipment, providing industrial clients with reliable and efficient solutions for material handling. The company, based in Shandong, China, leverages advanced engineering and manufacturing processes to deliver high-quality equipment that meets the demanding requirements of modern industrial applications. The coke particle pneumatic conveying system exemplifies the company's commitment to innovation and performance, offering a cost-effective and sustainable solution for coke particle transport. By integrating advanced features and robust construction, the equipment ensures long-term reliability and minimal operational costs, making it an ideal choice for industrial operations seeking efficient material handling solutions.