

What is Gray Bin Material Handling? What are the Design Principles?
Gray bin material handling is a specialized method of transporting bulk materials using a hopper or bin system. This approach is widely used in industrial settings to efficiently move powders, granules, and other bulk solids from one location to another. The system typically involves a hopper or bin that collects the material, which is then transferred through a conveyor or other transport mechanism to the desired destination. Understanding the fundamentals of gray bin material handling and its design principles is crucial for optimizing material flow in various industrial applications.
Understanding Gray Bin Material Handling
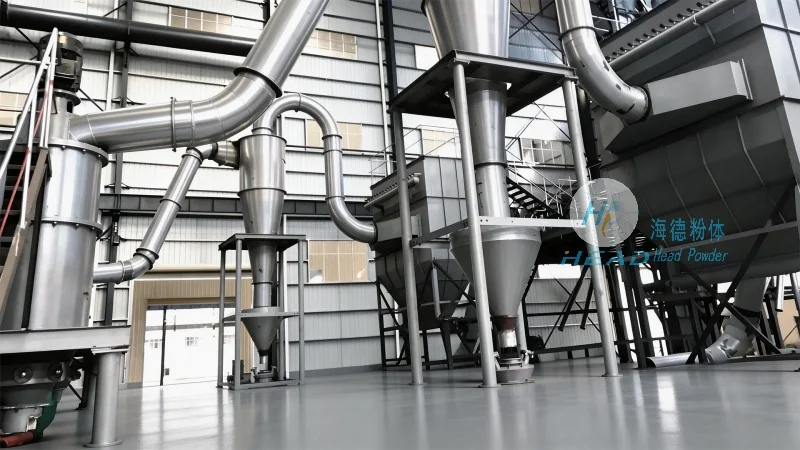
At its core, gray bin material handling refers to the process of moving bulk materials using a container, often referred to as a gray bin or hopper, which serves as the primary storage and transport unit. These bins are designed to hold large quantities of materials, such as powders, granules, or other bulk solids, and are equipped with mechanisms to facilitate the transfer of the material to a conveyor system or other processing equipment. The primary goal of this method is to ensure efficient, continuous, and controlled movement of materials, minimizing downtime and maximizing productivity in industrial operations. Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of such material handling systems, ensuring that clients receive high-quality solutions tailored to their specific needs.
Key Components of Gray Bin Material Handling Systems
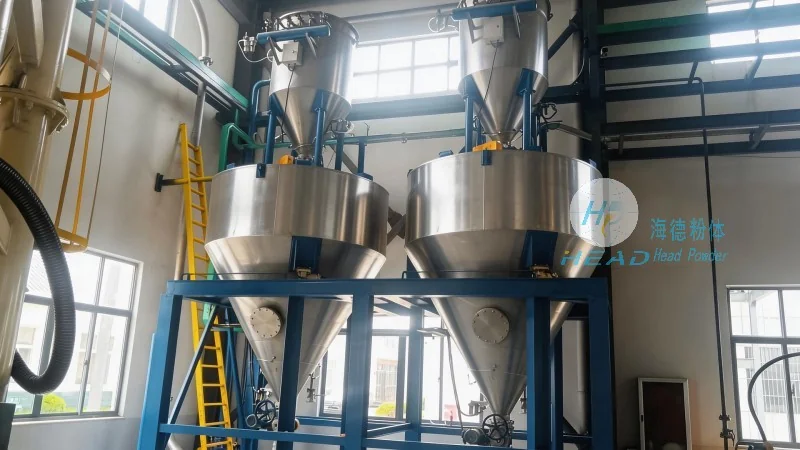
A typical gray bin material handling system consists of several key components that work together to ensure smooth operation. The main components include the gray bin itself, which is usually made of durable materials like metal or plastic to withstand the weight and abrasion of the materials being handled. The bin is often equipped with a discharge mechanism, such as a gate or valve, that controls the flow of material from the bin to the conveyor or other transport equipment. Additionally, the system may include a hopper or feeder that helps to regulate the flow of material, preventing clogging and ensuring a consistent feed rate. The conveyor system, which can be a belt conveyor, screw conveyor, or other type of transport mechanism, is responsible for moving the material from the bin to the processing or storage area. Finally, the control system, which may include sensors and automation equipment, monitors the operation of the system and adjusts the flow of material as needed to maintain optimal performance.
Design Principles for Gray Bin Material Handling
The design of gray bin material handling systems follows several key principles to ensure efficiency, safety, and reliability. One of the primary principles is the use of appropriate bin geometry to minimize material bridging and caking, which can occur when the material is stored in a hopper or bin. The bin is typically designed with a conical or hopper shape to facilitate the flow of material, with a slope that allows the material to move smoothly from the bin to the discharge point. Another important principle is the selection of appropriate materials for the bin and discharge mechanism to prevent wear and tear from the abrasive nature of the materials being handled. The bin is often made of stainless steel or other corrosion-resistant materials to ensure durability and longevity. Additionally, the system is designed to minimize the risk of material spillage or contamination, with features such as sealed discharge mechanisms and proper containment systems. The control system is also designed to ensure safe operation, with sensors that detect blockages or other issues and automatically shut down the system to prevent accidents.
Applications of Gray Bin Material Handling
Gray bin material handling systems are used in a wide range of industrial applications, including pharmaceutical manufacturing, food processing, chemical processing, and mining. In pharmaceutical manufacturing, for example, gray bins are used to transport powders and granules for drug production, ensuring that the materials are handled in a clean and controlled environment. In food processing, gray bins are used to transport ingredients such as flour, sugar, and other bulk foods, maintaining the quality and safety of the products. In chemical processing, gray bins are used to transport chemicals and other hazardous materials, with appropriate safety features to prevent accidents and protect workers. In mining, gray bins are used to transport ore and other bulk materials from the mine to processing facilities, ensuring efficient and safe operation.
Benefits of Gray Bin Material Handling
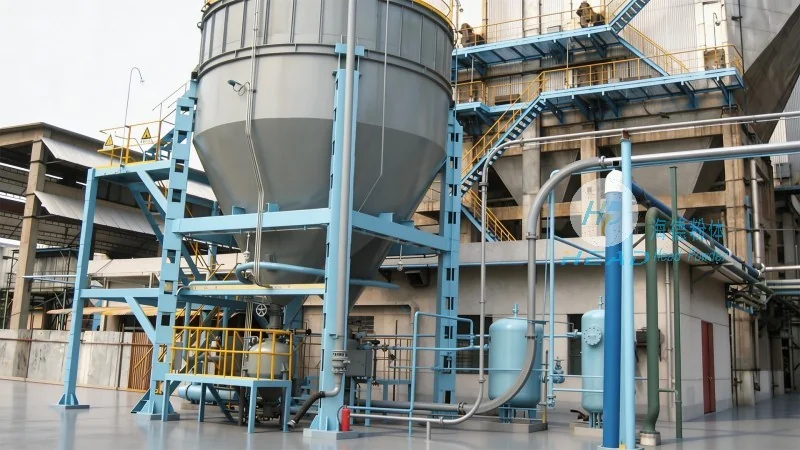
There are several benefits to using gray bin material handling systems in industrial operations. One of the primary benefits is the efficiency of the system, which allows for continuous and controlled movement of materials, minimizing downtime and maximizing productivity. The system is also designed to be safe and reliable, with features that prevent accidents and ensure the quality of the materials being handled. Additionally, the system is flexible and can be customized to meet the specific needs of different industrial applications, allowing for adaptation to changing production requirements. The use of gray bin material handling systems can also reduce labor costs, as the system can operate with minimal human intervention, and can improve the overall quality of the products being produced. Shandong HeadPowder Engineering Co., Ltd. offers tailored solutions that leverage these benefits to enhance client operations.
Conclusion
Gray bin material handling is a critical component of many industrial operations, providing an efficient and reliable method for moving bulk materials. The design principles and components of these systems are carefully engineered to ensure optimal performance, safety, and durability. By understanding the fundamentals of gray bin material handling and its design principles, industrial operations can optimize their material flow and improve overall productivity. As technology continues to advance, gray bin material handling systems are likely to become even more efficient and effective, further enhancing their role in industrial operations. With a focus on quality and innovation, Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of providing advanced material handling solutions for industries worldwide.