

What is a Rare Earth Powder Pneumatic Conveying System Equipment? And What Are Its Design Principles
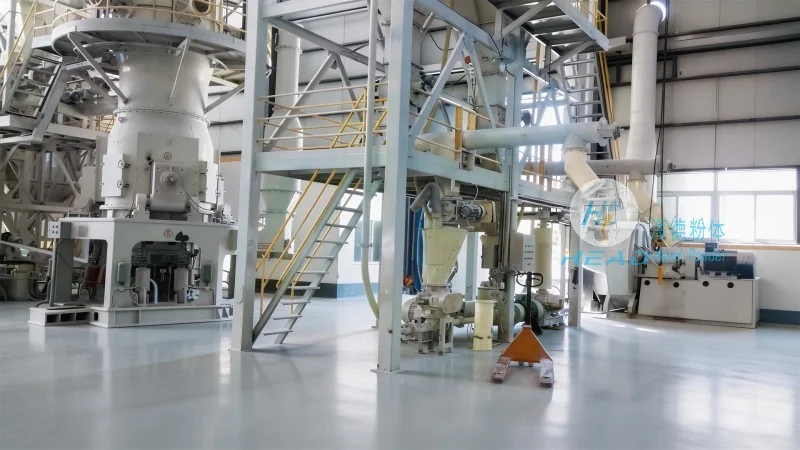
For industries dealing with rare earth powders, efficient and reliable material handling is crucial. A rare earth powder pneumatic conveying system equipment is a specialized solution designed to transport these fine particles through a pipeline using air or other gas as the conveying medium. This system combines mechanical and pneumatic principles to ensure safe, clean, and efficient movement of rare earth powders from one location to another.
Key Components of the Rare Earth Powder Pneumatic Conveying System
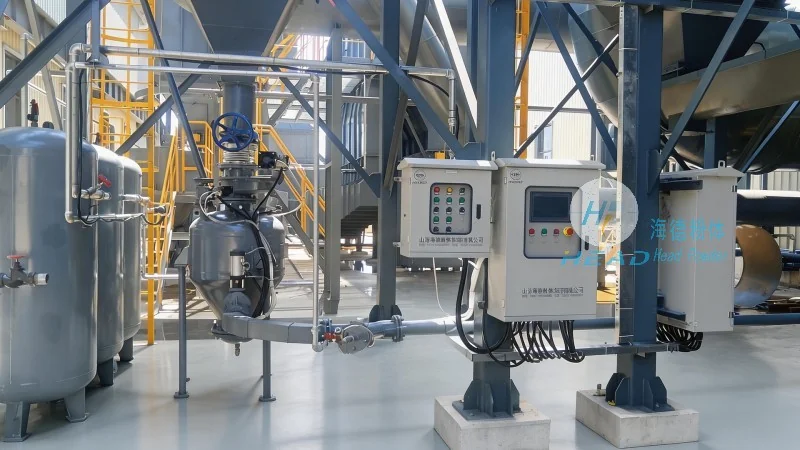
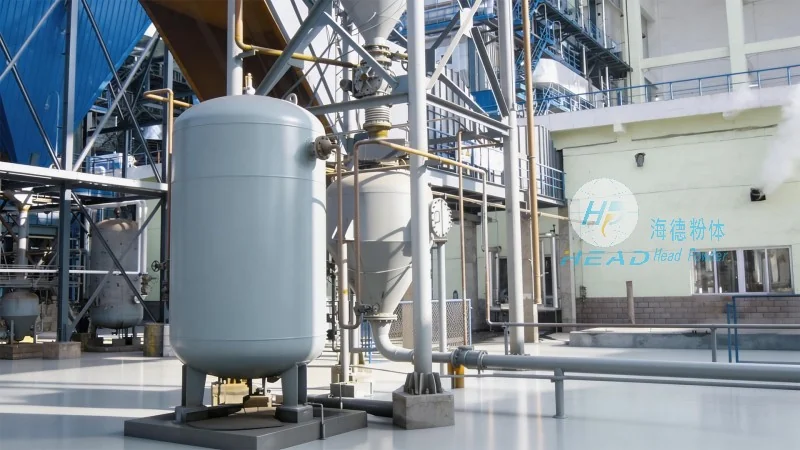
The system typically consists of several core components that work in tandem to achieve effective material transport. The primary components include a material feeder, which ensures a consistent flow of rare earth powder into the system; a conveying pipeline, which may be made of materials resistant to corrosion and abrasion, such as stainless steel or special polymers; a gas source, often a blower or compressor, that generates the necessary air pressure to move the powder; and a separation or collection unit that captures the powder at the destination point and returns the air to the system or releases it to the environment.
Design Principles for Rare Earth Powder Pneumatic Conveying
The design of a rare earth powder pneumatic conveying system is tailored to the specific characteristics of the material being transported. Key design principles include considering the particle size, density, and flowability of the rare earth powder, as these factors directly impact the air velocity and pressure required for effective transport. The system must also account for the distance between the source and destination, as longer distances may necessitate additional boosters or larger diameter pipelines to maintain sufficient pressure and prevent particle deposition. Additionally, the system is designed to minimize product degradation, ensuring that the rare earth powder remains in its original state without clumping or agglomeration during the conveying process. The selection of materials for the pipeline and components is critical to prevent contamination and corrosion, as rare earth powders can be sensitive to certain chemicals or environmental conditions.
Application and Benefits in Rare Earth Processing
Rare earth powder pneumatic conveying systems are widely used in the processing and manufacturing of rare earth elements, where precise and controlled material handling is essential. These systems offer several advantages over traditional methods like bucket elevators or belt conveyors. They provide a closed-loop system that reduces dust emissions and contamination, which is vital for maintaining product purity and compliance with environmental regulations. The systems also offer flexibility in layout, allowing for complex routing of pipelines to accommodate different plant configurations. Furthermore, pneumatic conveying can handle a wide range of particle sizes and flow rates, making it suitable for various stages of rare earth processing, from raw material handling to final product packaging.
About Shandong HeadPowder Engineering Co., Ltd.
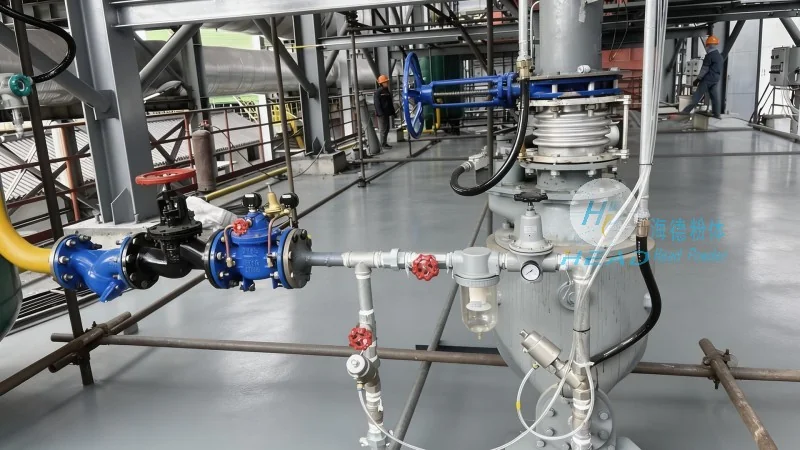
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of specialized equipment for powder handling, including rare earth powder pneumatic conveying systems. Headpowder is headquartered in Shandong, China, and has a strong reputation for delivering high-quality, reliable solutions tailored to the unique needs of the rare earth industry. The company focuses on innovation and precision engineering to ensure that its systems meet the stringent requirements of modern rare earth processing facilities, providing customers with efficient, cost-effective, and environmentally friendly material handling solutions.