

What is a Crystal Granule Pneumatic Conveying System Equipment? What is its Design Principle?
Crystal granule pneumatic conveying systems represent a sophisticated technology designed to transport fine or granular materials through a pipeline using pressurized air or other gas streams. This method offers an efficient alternative to traditional mechanical conveying systems, particularly for materials that are dusty, abrasive, or require a high degree of containment and control. The equipment itself comprises several key components, including a hopper for material storage, a feeder to regulate the flow of granules, a conveying line where the material is propelled by the gas, and a receiver for the discharged material. Each component is engineered to work in harmony to ensure reliable and continuous operation.
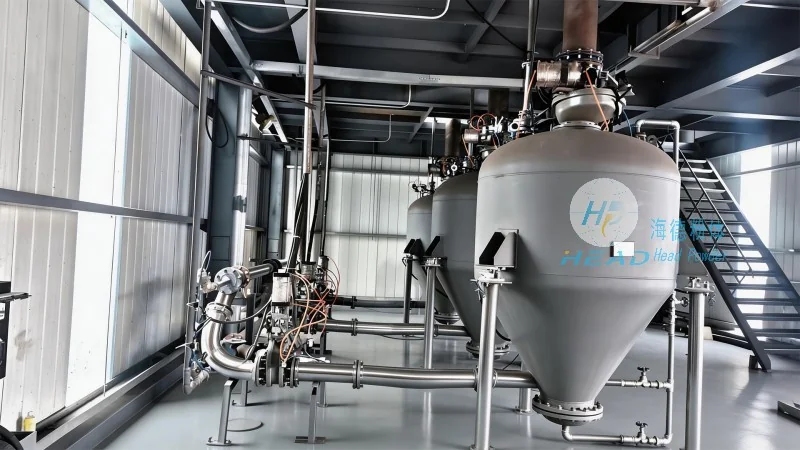
Design Principles of Crystal Granule Pneumatic Conveying Systems
The core design principle revolves around the balance between the material's properties and the gas dynamics within the system. Key factors include the material's density, particle size distribution, and flowability, which determine the appropriate air velocity and pressure required for effective transport. The system typically operates under either positive pressure (where air is forced through the line) or negative pressure (where air is drawn out), with positive pressure being more common for bulk material handling due to its ability to handle larger quantities and longer distances. The design also considers the risk of material degradation or segregation, which can be mitigated through features such as pulse-jet cleaning of the conveying line and the use of smooth, non-stick surfaces to prevent particle buildup.
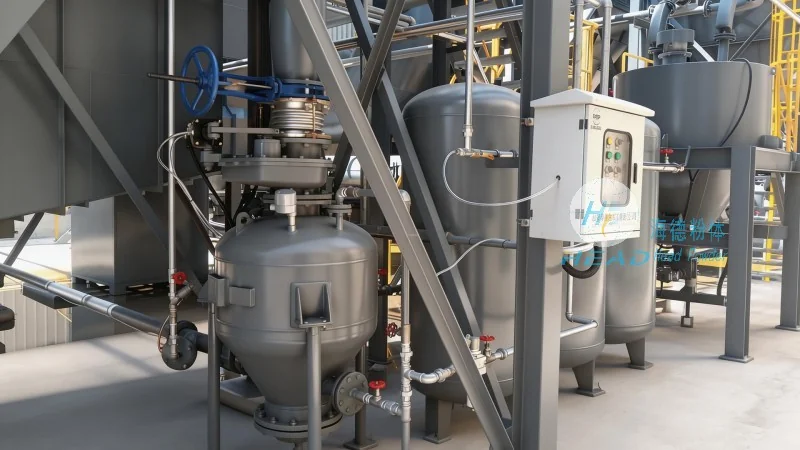
Key Components and Their Functions
At the heart of a crystal granule pneumatic conveying system is the material hopper, which serves as the primary storage vessel. This hopper is equipped with a discharge valve, often a rotary valve or a star valve, that controls the flow of granules into the feeder. The feeder, typically a screw or a rotary valve, regulates the material feed rate to match the system's demand, preventing overloading or underfeeding that could lead to system inefficiencies. The conveying line itself is usually made of stainless steel or other corrosion-resistant materials to accommodate the potential acidity or moisture of crystal granules. The line may include bends, elbows, and expansion joints to accommodate changes in direction and pressure, while maintaining minimal pressure drop. The receiver, positioned at the end of the line, collects the conveyed material and may include a filter or a cyclone to separate any entrained air or fine particles from the product.
Advantages of Crystal Granule Pneumatic Conveying Systems
Compared to traditional mechanical conveying methods, crystal granule pneumatic conveying systems offer several advantages. One of the most significant is the ability to handle materials that are difficult to transport mechanically, such as dusty or fine powders, without the risk of clogging or material degradation. The enclosed system also provides better environmental control, reducing dust emissions and improving workplace safety. Additionally, the system can be designed for long-distance transport, making it suitable for industrial facilities where material sources and destinations are separated by considerable distances. The flexibility of the system allows for easy integration with other processing equipment, such as mixers, classifiers, or packaging machines, enhancing overall production efficiency.

About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling solutions, including crystal granule pneumatic conveying systems. With headquarters located in Shandong, China, the company has established itself as a trusted partner in the chemical, pharmaceutical, and food processing industries. HeadPowder specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of its clients, ensuring optimal performance and reliability. The company's commitment to quality and innovation has earned it a reputation for delivering durable, efficient, and cost-effective solutions that meet the highest industry standards. Through continuous research and development, HeadPowder remains at the forefront of material handling technology, providing solutions that enhance productivity and safety in industrial applications.