

[Pneumatic Conveying in Bulk Transport of Ammonium Bicarbonate]
Ammonium bicarbonate is a widely used chemical in various industries, including agriculture and food processing. Its bulk handling requires efficient and reliable transport systems to maintain product quality and ensure smooth operational processes. Pneumatic conveying technology has emerged as a preferred solution for transporting ammonium bicarbonate due to its ability to handle fine powders and minimize product degradation. This article explores the application of pneumatic conveying in the bulk transport of ammonium bicarbonate, highlighting the technical advantages and practical implementation by Shandong HeadPowder Engineering Co., Ltd.
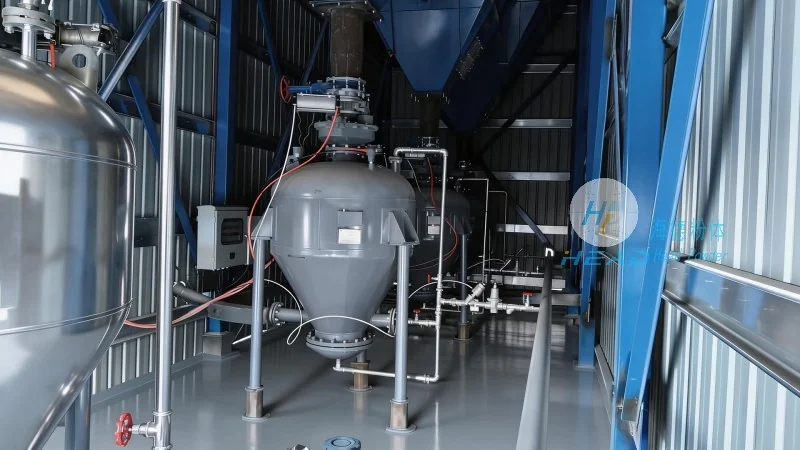
Understanding Ammonium Bicarbonate and Its Handling Challenges
Ammonium bicarbonate (NH₄HCO₃) is a white crystalline powder with a slightly alkaline taste. It is highly soluble in water and is commonly used as a leavening agent in baking, a fertilizer component, and in chemical synthesis. The material's fine particle size and hygroscopic nature pose challenges during bulk transport. Traditional methods like belt conveyors or bucket elevators may cause product segregation, agglomeration, and moisture absorption, leading to quality issues. Pneumatic conveying addresses these challenges by using air to transport the material in a closed system, reducing exposure to external elements and maintaining product integrity.
Pneumatic Conveying Technology for Bulk Transport
Pneumatic conveying systems utilize compressed air to move powders through pipelines. There are two main types: dilute-phase and dense-phase systems. Dilute-phase conveying uses low air velocity and high material flow rates, suitable for short distances and low pressure applications. Dense-phase conveying, on the other hand, operates at higher air pressure and lower flow rates, providing better control over material velocity and minimizing product degradation. For ammonium bicarbonate, dense-phase pneumatic conveying is often preferred as it offers superior control over particle movement and reduces the risk of clogging or product loss.
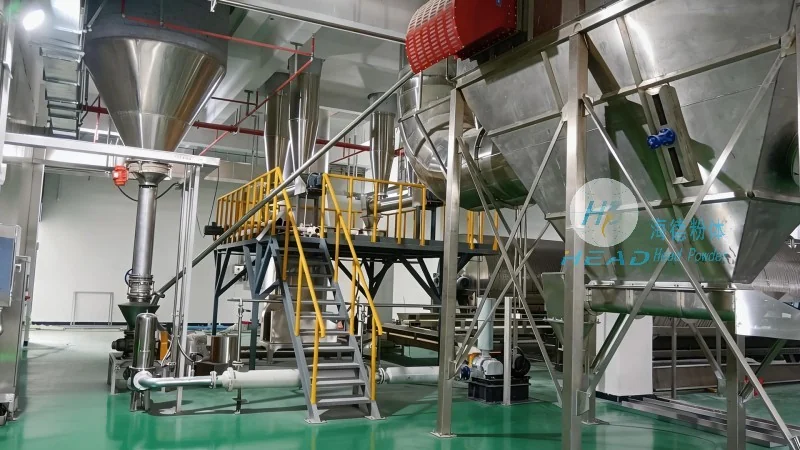
HeadPowder's Expertise in Ammonium Bicarbonate Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the unique requirements of ammonium bicarbonate. The company's engineers leverage advanced engineering principles and extensive industry experience to develop customized solutions that ensure efficient, safe, and cost-effective transport. HeadPowder's systems are equipped with features such as air filtration, moisture control, and material flow monitoring to maintain product quality throughout the conveying process.
Key Advantages of Pneumatic Conveying for Ammonium Bicarbonate
Implementing pneumatic conveying for ammonium bicarbonate offers several key advantages. Firstly, it eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and downtime. Secondly, the closed system prevents contamination from dust or moisture, ensuring the material remains in its original state. Thirdly, the technology allows for flexible and scalable solutions, adapting to varying production volumes and facility layouts. Additionally, pneumatic conveying systems can be integrated with other processing equipment, creating a seamless material flow from storage to processing units.
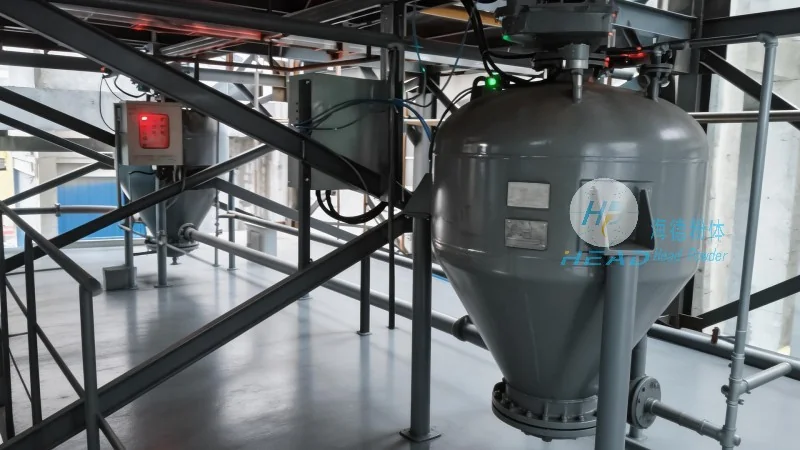
Customized Solutions for Diverse Applications
HeadPowder recognizes that each ammonium bicarbonate application has specific requirements. Whether for agricultural fertilizer production, food processing, or chemical manufacturing, the company offers tailored pneumatic conveying solutions. These solutions may include different pipeline configurations, air pressure systems, and material handling accessories to meet the unique needs of each client. The company's team of experts works closely with clients to assess their operational needs, provide technical recommendations, and deliver systems that optimize performance and efficiency.
Ensuring Product Quality and Safety
For ammonium bicarbonate, maintaining product quality and safety is paramount. HeadPowder's pneumatic conveying systems incorporate advanced filtration and air purification technologies to prevent contamination. The systems also include safety features such as pressure relief valves and emergency shut-off mechanisms to protect against over-pressurization and other hazards. By adhering to strict quality control standards, HeadPowder ensures that its conveying solutions meet the highest industry benchmarks, providing clients with reliable and trustworthy equipment for their bulk transport needs.