

Airborne Conveying in the Bulk Handling of Calcium Hydroxide
For industries dealing with calcium hydroxide, efficient and reliable bulk material handling is crucial. The process of transporting this chemical, especially in large quantities, requires specialized equipment and systems to ensure safety, efficiency, and minimal product degradation. This article explores the application of airborne conveying technology in the bulk handling of calcium hydroxide, highlighting its benefits and practical implementation.
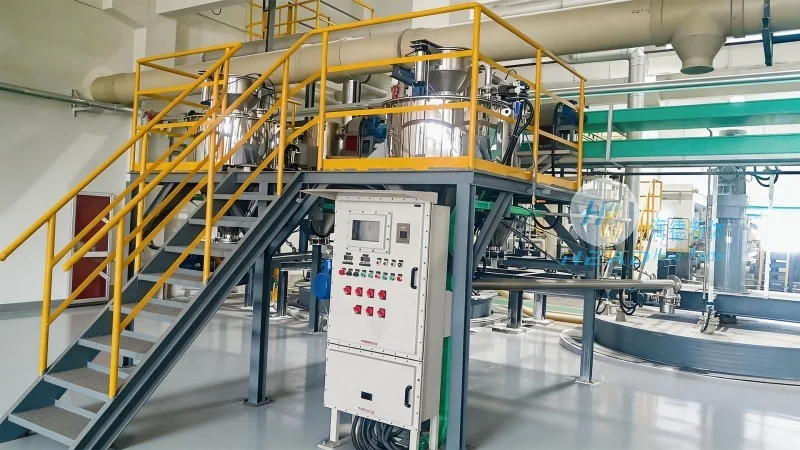
Understanding Calcium Hydroxide and Its Handling Challenges
Calcium hydroxide, commonly known as slaked lime, is a white powder used in various industries such as construction, agriculture, and water treatment. Its bulk handling presents unique challenges due to its fine particle size, hygroscopic nature, and potential for dust generation. Traditional methods like belt conveyors or screw conveyors may not be ideal for calcium hydroxide due to the risk of clogging, material degradation, and health hazards from dust exposure. Airborne conveying offers a solution by using air to transport the material, reducing these risks and improving overall handling efficiency.
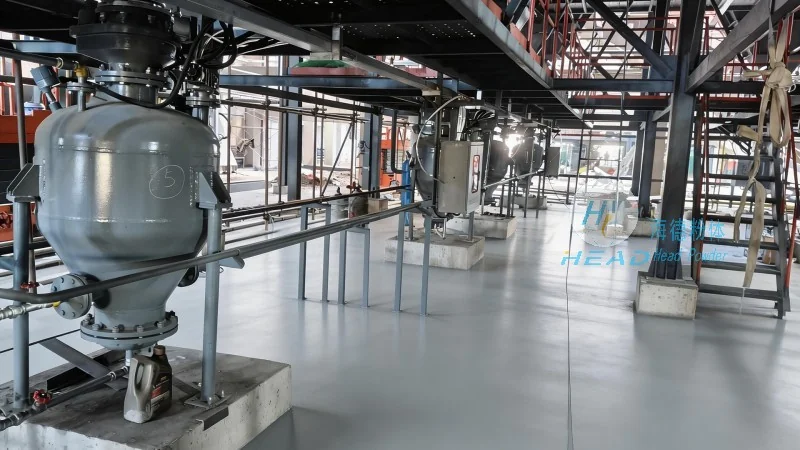
The HeadPowder Approach to Airborne Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing advanced airborne conveying systems tailored for calcium hydroxide. With years of experience in the industry, HeadPowder understands the specific requirements of handling this chemical and has developed systems that address common challenges such as dust control, material flow optimization, and system durability. The company’s approach focuses on customizing solutions to meet the unique needs of each client, ensuring that the conveying system is both efficient and safe.
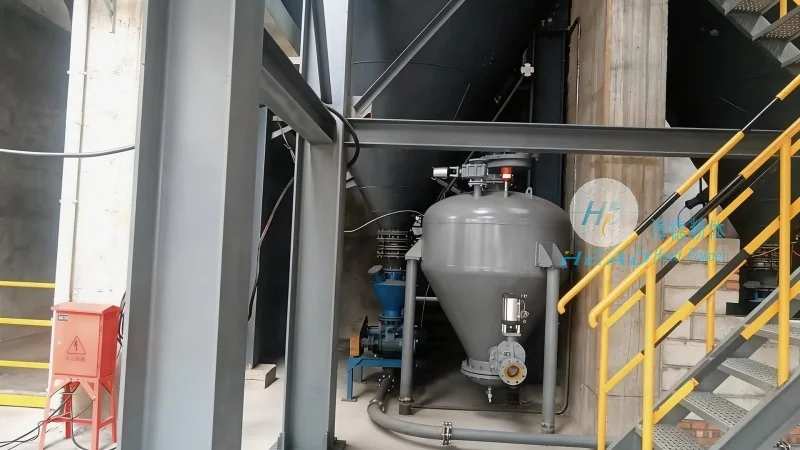
Key Features and Benefits of Airborne Conveying for Calcium Hydroxide
HeadPowder’s airborne conveying systems for calcium hydroxide offer several key features that enhance performance and reliability. These include: High Efficiency and Capacity - The systems can handle large volumes of calcium hydroxide with minimal downtime, improving overall production throughput. Low Maintenance and Durability - The components are designed to withstand the corrosive and abrasive nature of calcium hydroxide, reducing maintenance costs and extending the system's lifespan. Effective Dust Control - Advanced filtration and sealing systems minimize dust emissions, ensuring a safe working environment and compliance with environmental regulations. Energy Efficiency - Optimized air flow and system design reduce energy consumption, leading to lower operational costs.
Customization and Integration for Optimal Performance
HeadPowder recognizes that each calcium hydroxide handling operation has unique requirements. Therefore, the company offers comprehensive customization options to ensure that the airborne conveying system integrates seamlessly with existing infrastructure. This includes adjusting the system's capacity, modifying the conveying distance, and incorporating additional features such as material storage and dosing systems. The company's engineering team works closely with clients to understand their specific needs and develop a tailored solution that maximizes efficiency and minimizes operational risks.
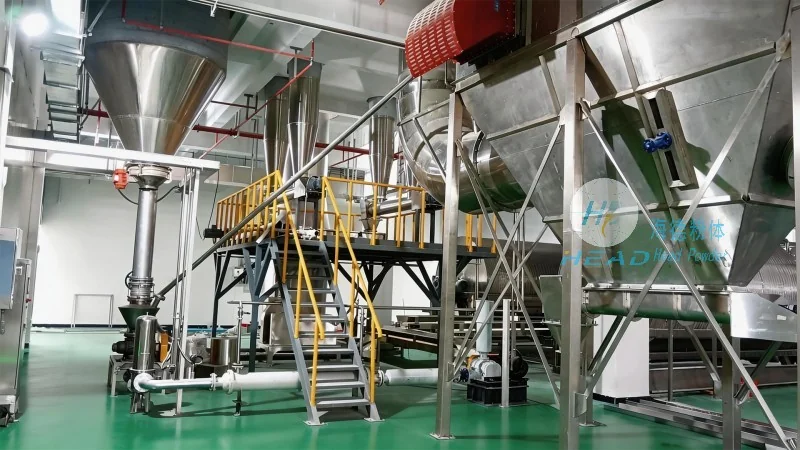
Conclusion: Enhancing Calcium Hydroxide Handling with Airborne Conveying
For businesses looking to improve the efficiency and safety of calcium hydroxide bulk handling, airborne conveying technology from Shandong HeadPowder Engineering Co., Ltd. provides a reliable and effective solution. By leveraging advanced engineering and customization, HeadPowder's systems address the unique challenges of handling calcium hydroxide while offering significant benefits in terms of efficiency, durability, and environmental compliance. As a trusted partner in bulk material handling, HeadPowder continues to deliver high-quality solutions that meet the evolving needs of the industry.