

Design of a Vacuum Pneumatic Conveying Device for Glucose
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling solutions. The company's expertise lies in creating efficient and reliable systems for transporting bulk materials, including the vacuum pneumatic conveying device specifically designed for glucose. This system utilizes a vacuum-driven mechanism to draw material from a storage silo or hopper into a processing unit, ensuring minimal product contamination and loss. The design incorporates stainless steel components and advanced control systems to meet the stringent requirements of the food and pharmaceutical industries.
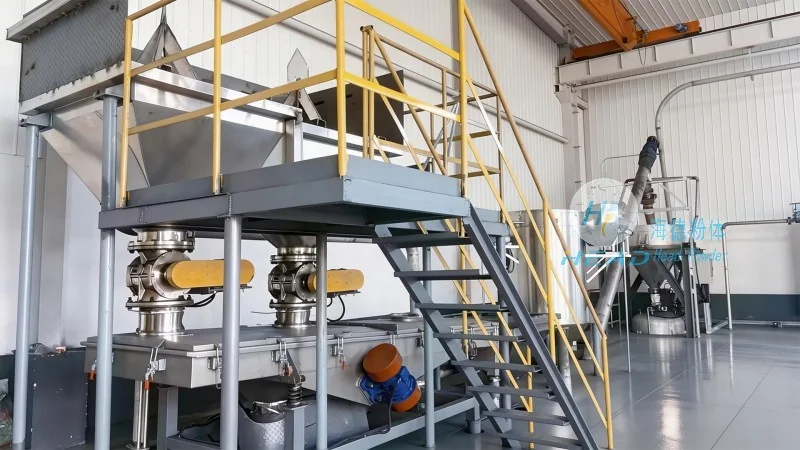
Product Overview: Vacuum Pneumatic Conveying System for Glucose
The vacuum pneumatic conveying device for glucose is engineered to provide a clean, efficient, and hygienic method for transporting granular or powdered glucose. This system utilizes a vacuum-driven mechanism to draw material from a storage silo or hopper into a processing unit, ensuring minimal product contamination and loss. The design incorporates stainless steel components and advanced control systems to meet the stringent requirements of the food and pharmaceutical industries.
Key Design Features and Advantages
One of the primary advantages of this vacuum pneumatic conveying system is its ability to handle sensitive materials like glucose without degradation. The system operates under negative pressure, which prevents dust and airborne contamination, maintaining product purity. Additionally, the design allows for flexible installation, accommodating various plant layouts and material flow requirements. The equipment is equipped with automated controls that optimize energy consumption and ensure consistent material flow rates, reducing operational costs and enhancing process efficiency. Furthermore, the system is designed with easy access points for maintenance, minimizing downtime and ensuring continuous operation.
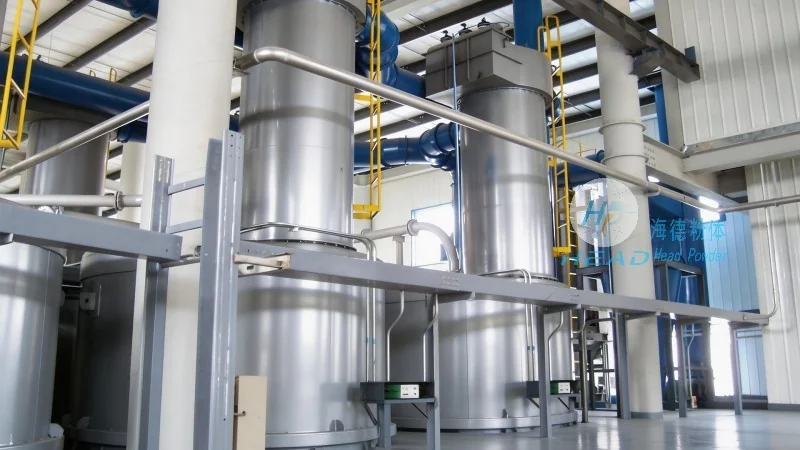
Technical Specifications and Performance
The vacuum pneumatic conveying device for glucose is built with robust components that ensure long-term reliability. Key technical specifications include a conveying capacity ranging from 0.5 to 10 tons per hour, depending on the application. The system features a high-efficiency vacuum pump that maintains consistent negative pressure levels, ensuring smooth material transport. The stainless steel construction is easy to clean and maintain, adhering to GMP (Good Manufacturing Practice) standards. The control panel provides real-time monitoring of pressure, flow rate, and system status, enabling operators to quickly identify and resolve any issues. The system also includes safety features such as pressure relief valves and overcurrent protection to prevent equipment damage and ensure operator safety.
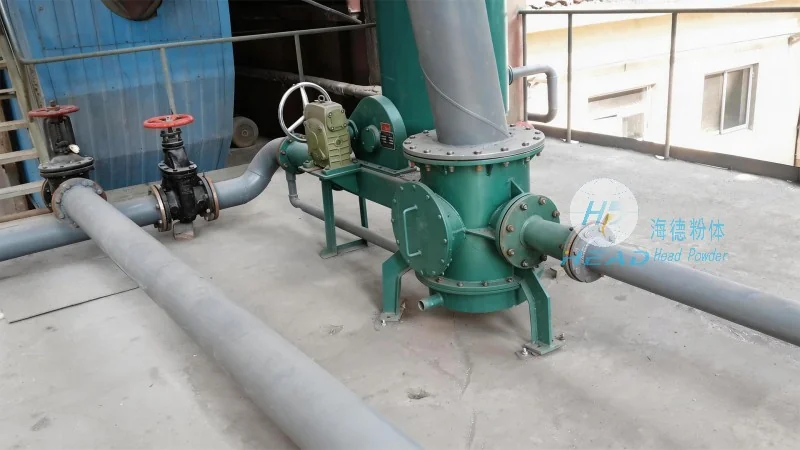
Application and Industry Use Cases
This vacuum pneumatic conveying system is particularly suitable for glucose processing facilities, where maintaining product quality and hygiene is paramount. It is commonly used in the production of glucose syrups, sweeteners, and other glucose-based products. The system can be integrated into existing production lines, replacing traditional bulk handling methods that are often less efficient and more prone to contamination. By implementing this advanced conveying solution, manufacturers can improve production throughput, reduce downtime, and enhance overall operational efficiency. Additionally, the system's hygienic design makes it ideal for applications where product sterility is critical, such as in the pharmaceutical sector.
Company Information and Contact
HeadPowder Engineering Co., Ltd. is committed to delivering high-quality engineering solutions tailored to the needs of the food, pharmaceutical, and chemical industries. With a focus on innovation and customer satisfaction, the company provides comprehensive support, including design, installation, and after-sales service. HeadPowder's headquarters is located in Shandong, China, and the company serves clients globally with customized material handling systems that meet international standards. The company's team of experienced engineers works closely with clients to understand their specific requirements and develop solutions that enhance productivity and reduce operational costs.