

Introduction to High-Pressure Bin Pump Pneumatic Conveying Systems and Their Structural Principles
High-pressure bin pump pneumatic conveying systems represent a sophisticated and efficient method for transporting bulk materials over long distances or within industrial facilities. These systems are designed to handle a wide range of materials, including powders, granules, and other particulate substances, with high reliability and minimal maintenance requirements. The core of such systems is the high-pressure bin pump, which operates by creating a pressure differential to move material through a pipeline network. This technology offers significant advantages over traditional conveying methods, such as reduced labor costs, improved safety, and the ability to transport materials in a closed system, minimizing dust and contamination.
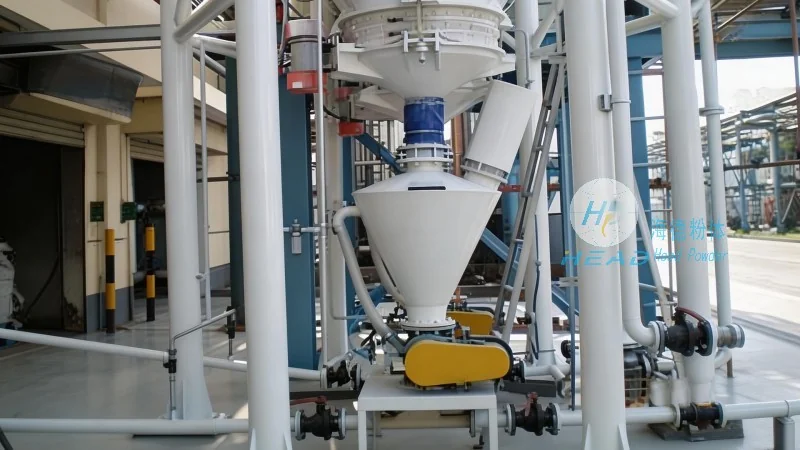
Structural Principles and Key Components
The structural principle of a high-pressure bin pump system involves several key components working in concert. The system typically includes a storage bin (or hopper) where the material is stored, a bin pump that generates the necessary pressure to move the material, a pipeline network that transports the material from the source to the destination, and a receiver or discharge point where the material is deposited. The bin pump itself is a positive displacement pump that uses a rotating or reciprocating mechanism to create the pressure needed to push the material through the pipeline. This pump is often equipped with a pressure control system to regulate the flow and ensure consistent performance. The pipeline network may include various fittings, valves, and filters to manage the material flow and maintain system efficiency. Additionally, the system may incorporate a dust collection or filtration system to ensure environmental compliance and product purity.
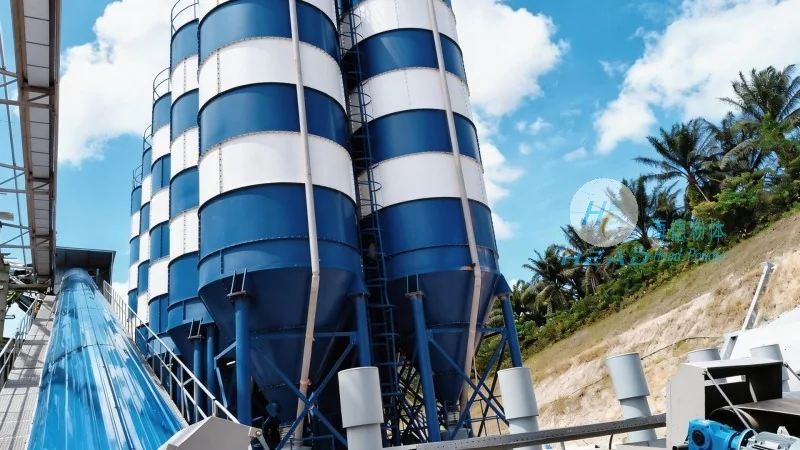
Operational Efficiency and Material Handling Capabilities
High-pressure bin pump systems are known for their operational efficiency and ability to handle diverse materials. The positive displacement nature of the pump ensures a consistent flow rate, which is crucial for processes that require precise material delivery. These systems can transport materials over distances of several hundred meters or more, depending on the design and pressure capabilities. The closed pipeline system also helps in maintaining material quality by preventing exposure to air, moisture, or contaminants, which is particularly important for sensitive materials like pharmaceuticals or food products. Furthermore, the system's ability to operate under high pressure allows for the efficient movement of materials with high bulk density, reducing the number of transfer points and overall system complexity.
About HeadPowder: A Leading Manufacturer in China
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, manufacturing, and supply of high-pressure bin pump pneumatic conveying systems. With years of experience in the industry, HeadPowder has developed a reputation for producing high-quality, durable, and efficient equipment tailored to meet the specific needs of various industries, including chemical, food, pharmaceutical, and mining sectors. The company's products are engineered to withstand harsh operating conditions and provide long-term reliability, ensuring that customers receive a return on their investment. HeadPowder's commitment to innovation and customer service has made it a trusted partner for businesses seeking advanced material handling solutions.
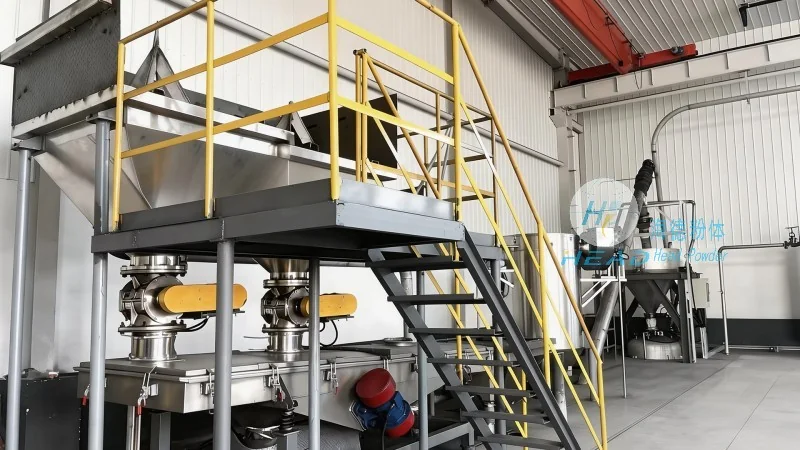
Application Examples and Industry Impact
High-pressure bin pump pneumatic conveying systems are widely used in various industries due to their versatility and efficiency. In the chemical industry, these systems are used to transport raw materials and finished products, such as powders and granules, between processing units. In the food and pharmaceutical sectors, the closed system and pressure control features are essential for maintaining product purity and safety standards. The mining industry also benefits from these systems for transporting ore and other minerals from extraction sites to processing facilities. By providing a reliable and efficient means of material transport, high-pressure bin pump systems contribute to increased productivity and reduced operational costs for businesses across different sectors.