

Operation Process and Working Principle of Intelligent Bulk Bag Unloading Pneumatic Powder Conveying
HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced powder handling solutions. Their flagship product, the intelligent bulk bag unloading pneumatic powder conveying machine, represents a significant advancement in material handling technology. This equipment is designed to efficiently and safely transfer bulk powders from sealed bags into processing systems, streamlining industrial operations.
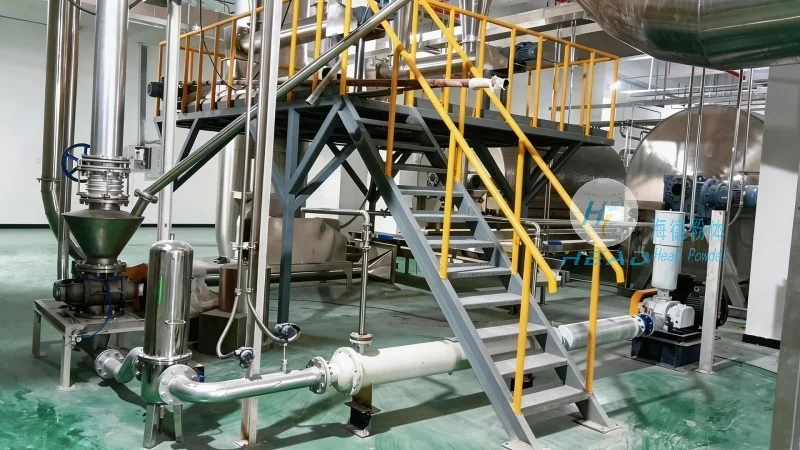
Key Components and Design Features
The intelligent bulk bag unloading pneumatic powder conveying machine incorporates several key components that enhance its performance and reliability. The system typically includes a bulk bag discharger, a pneumatic conveying unit, and a control panel. The discharger is engineered to open and empty the bag without manual intervention, while the pneumatic conveying section uses air pressure to transport the powder to the desired destination. Advanced sensors and automation features ensure precise control over the entire process, minimizing material loss and optimizing operational efficiency.
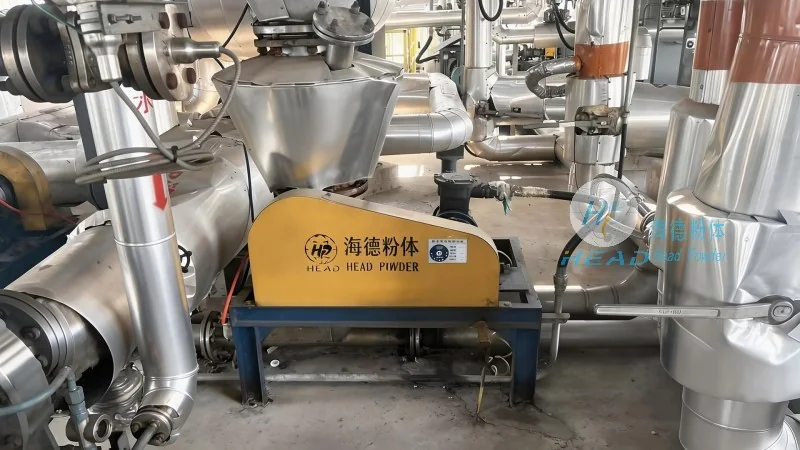
Operation Process: Step-by-Step Overview
The operation of the intelligent bulk bag unloading pneumatic powder conveying machine follows a systematic sequence to ensure smooth and efficient material transfer. Initially, the bulk bag is positioned on the discharger frame. The system then automatically opens the bag's top, allowing the powder to flow into the hopper. Concurrently, the pneumatic conveying unit activates, generating the necessary air pressure to move the powder through the pipeline. The control panel monitors the process in real-time, adjusting air flow and pressure as needed to maintain consistent material transfer rates. Once the bag is empty, the system automatically shuts down and signals for the next bag to be loaded, completing the cycle.
Working Principle: How It Transforms Material Handling
The working principle of this machine combines mechanical and pneumatic technologies to achieve seamless powder transfer. The bulk bag discharger uses a mechanical mechanism to open the bag and guide the powder into the hopper. Simultaneously, the pneumatic conveying system employs compressed air to create a low-pressure zone in the pipeline, drawing the powder from the hopper and transporting it to the processing unit. This combination of methods ensures that even fine or cohesive powders are handled without degradation or segregation. The intelligent control system further enhances the process by integrating sensors that detect the bag's weight, flow rate, and pressure, providing data for process optimization and maintenance scheduling.
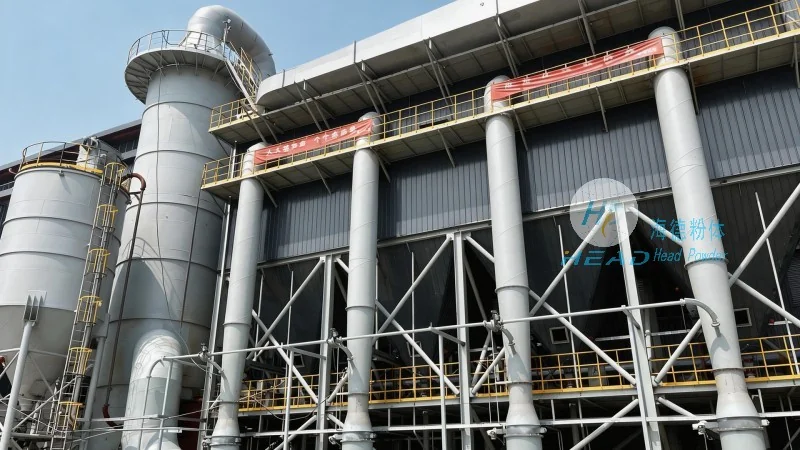
Benefits and Applications in Industrial Settings
The intelligent bulk bag unloading pneumatic powder conveying machine offers numerous benefits for industries that rely on bulk powder handling. It significantly reduces labor costs by automating the unloading process, eliminates the need for manual bag opening and handling, and minimizes the risk of dust exposure and material contamination. The system is particularly suitable for applications in pharmaceuticals, food processing, chemical manufacturing, and other industries where product purity and safety are paramount. Its compact design and flexible configuration allow it to be integrated into existing production lines, enhancing overall operational efficiency and productivity.