

Operation Process and Working Principle of Purified Powder Pneumatic Conveying Equipment
Efficient and reliable transportation of powdered materials is a critical requirement in various industrial sectors, including chemical, pharmaceutical, food processing, and mining. Among the technologies available, purified powder pneumatic conveying equipment stands out as a versatile solution for handling fine powders with high precision and minimal contamination. This article, produced by Shandong HeadPowder Engineering Co., Ltd. (headpowder), delves into the operation process and working principle of such equipment, highlighting its key components, operational flow, and the advanced purification systems that ensure product integrity and environmental compliance. The company, based in Shandong, China, specializes in designing and manufacturing advanced material handling solutions tailored to meet the diverse needs of modern industries.
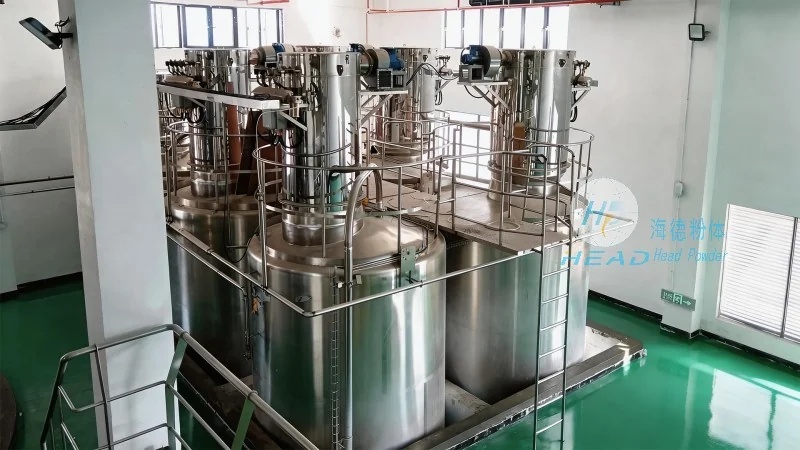
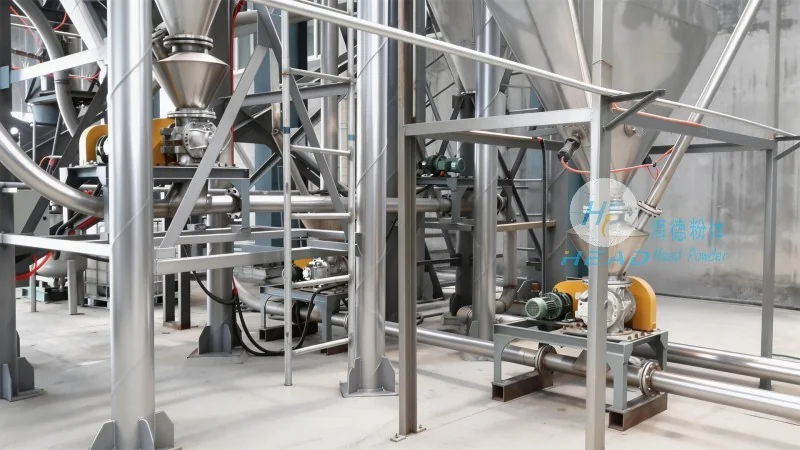
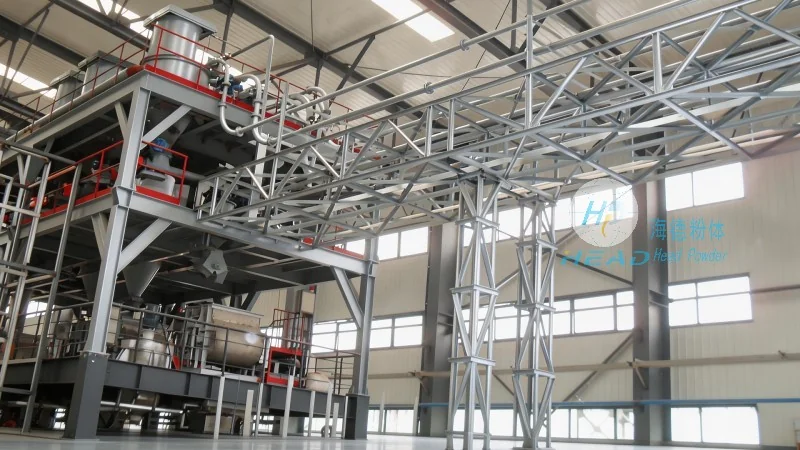
Overview of Purified Powder Pneumatic Conveying Equipment
Purified powder pneumatic conveying systems are engineered to transport dry powders or granules through a closed pipeline using air or other gases as the conveying medium. The primary goal is to achieve efficient material transfer while maintaining the purity of the product and protecting the environment from dust emissions. These systems are particularly suitable for materials that are sensitive to moisture, temperature, or contamination, making them indispensable in industries where product quality is paramount.