

Operation Process and Working Principle of Activated Carbon Powder Conveyor
Activated carbon powder conveying machines are essential equipment in industrial processes, particularly for handling fine powders like activated carbon. These machines are designed to efficiently transport activated carbon powder from one location to another while maintaining product integrity and minimizing dust emissions. The operation process and working principle of such conveyors are critical for understanding their functionality and optimizing performance in various industrial applications.
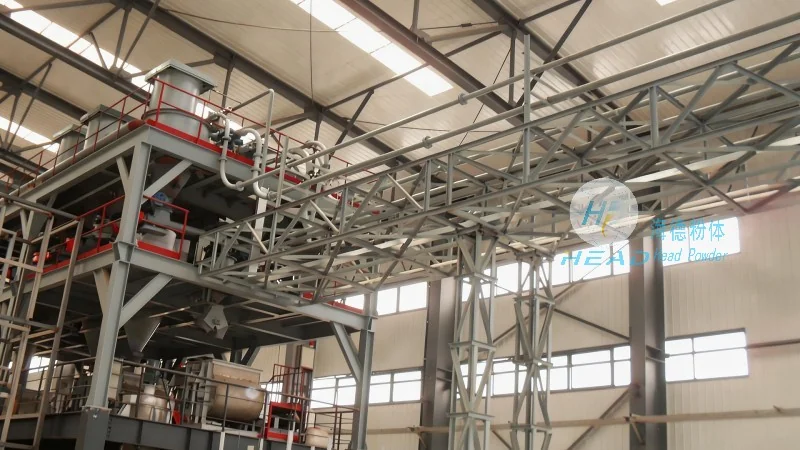
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of high-quality powder conveying systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner in the industry, providing reliable solutions for activated carbon and other fine powder handling needs. The company’s headquarters and main production facilities are located in Shandong, China, where advanced manufacturing technologies and rigorous quality control measures are employed to ensure the excellence of their products.
Key Components and Structure of the Conveyor System
The activated carbon powder conveying machine typically consists of several key components that work in harmony to achieve efficient material transport. These components include a hopper for material storage, a feeding mechanism to control the flow of powder, a conveyor belt or screw mechanism for actual transport, and a discharge system to deliver the material to the desired destination. The hopper is designed to hold a sufficient quantity of activated carbon powder, ensuring a continuous supply to the conveyor. The feeding mechanism, often equipped with a variable speed drive, allows for precise control over the powder flow rate, preventing overloading or underloading of the conveyor. The conveyor itself, whether a belt conveyor or a screw conveyor, is engineered to handle fine powders without causing blockages or degradation of the material. The discharge system ensures that the activated carbon powder is delivered smoothly to the next processing stage or storage area.
Operation Process of the Activated Carbon Powder Conveyor
The operation process of the activated carbon powder conveying machine involves several sequential steps that ensure the efficient and safe transport of activated carbon powder. First, the activated carbon powder is loaded into the hopper from a storage silo or bulk container. The powder is then fed into the conveyor system through the feeding mechanism, which regulates the flow rate based on the system’s requirements. As the powder moves along the conveyor, it is transported to the discharge point. The conveyor’s speed and feeding rate are continuously monitored and adjusted to maintain a consistent flow, preventing any buildup or clogging. The entire process is automated, with sensors and control systems ensuring that the conveyor operates within optimal parameters. This automated operation not only enhances efficiency but also reduces the risk of human error and ensures consistent product quality.

Working Principle of the Activated Carbon Powder Conveyor
The working principle of the activated carbon powder conveying machine is based on the mechanical transport of fine powders using a conveyor system. The machine utilizes a combination of gravity, friction, and controlled feeding to move the activated carbon powder from the hopper to the discharge point. The feeding mechanism, such as a rotary valve or a screw feeder, controls the rate at which the powder enters the conveyor. The conveyor belt or screw rotates at a specific speed, creating a moving surface that pulls the powder along its path. The design of the conveyor, including the angle of inclination and the material of the conveyor surface, is optimized to minimize friction and prevent the powder from sticking or clogging. The discharge system then collects the transported powder and directs it to the next stage of the process. The entire system operates under controlled conditions, ensuring that the activated carbon powder remains in a dry and stable state throughout the conveying process.
Advantages of Using Activated Carbon Powder Conveying Machines
Activated carbon powder conveying machines offer several advantages over traditional manual or pneumatic conveying methods. One of the primary benefits is the ability to handle fine powders without causing dust emissions or contamination. The enclosed design of the conveyor system prevents dust from escaping into the environment, making it suitable for applications where dust control is critical. Additionally, these machines provide consistent and reliable transport of activated carbon powder, ensuring that the material reaches its destination without degradation or loss. The automated operation reduces labor costs and increases productivity, as the system can operate continuously without the need for constant human supervision. Furthermore, the modular design of the conveyor allows for easy integration with existing industrial processes, making it a versatile solution for various applications. The energy efficiency of the conveyor system also contributes to lower operational costs, as it requires less power to operate compared to other conveying methods.
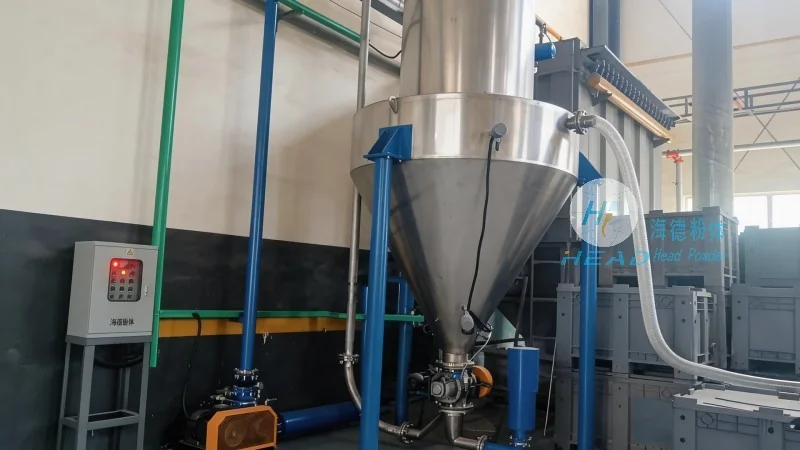
Applications and Industries Using Activated Carbon Powder Conveying Machines
Activated carbon powder conveying machines are widely used in various industries that rely on the handling of fine powders. In the chemical industry, these machines are used to transport activated carbon for adsorption processes, such as water treatment and air purification. The food and beverage industry also utilizes these conveyors to handle activated carbon used in filtration and purification of beverages. The pharmaceutical industry benefits from the precise and dust-free transport of activated carbon, which is essential for maintaining product quality and compliance with regulatory standards. Additionally, the environmental industry uses activated carbon powder conveying machines for waste treatment and pollution control applications, where the efficient transport of activated carbon is crucial for effective adsorption and remediation. The versatility of the conveyor system makes it suitable for a wide range of applications, from small-scale laboratory use to large-scale industrial production.
Maintenance and Troubleshooting Tips for Activated Carbon Powder Conveying Machines
Proper maintenance and regular troubleshooting are essential to ensure the long-term performance and reliability of activated carbon powder conveying machines. Regular inspection of the hopper and feeding mechanism is necessary to check for any blockages or wear and tear. The conveyor belt or screw should be inspected for signs of wear, such as cracks or fraying, and replaced if necessary. The control systems and sensors should be checked to ensure they are functioning correctly and providing accurate data. Cleaning the conveyor system regularly, especially after handling different materials, helps prevent the buildup of dust and debris, which can affect the performance of the machine. If the conveyor experiences issues such as clogging or uneven flow, it is important to check the feeding rate and conveyor speed settings. Adjusting these parameters can often resolve the problem. In case of more serious issues, such as motor failure or mechanical damage, professional maintenance services should be sought to ensure the machine is repaired correctly and safely. Regular maintenance not only extends the lifespan of the conveyor but also ensures consistent performance and reduces the risk of downtime.
Conclusion
Activated carbon powder conveying machines are critical equipment for efficiently handling fine powders in various industrial applications. The operation process and working principle of these machines are designed to ensure reliable, dust-free, and consistent transport of activated carbon powder. Manufactured by companies like Shandong HeadPowder Engineering Co., Ltd., these conveyors offer several advantages, including improved efficiency, reduced labor costs, and enhanced product quality. By understanding the key components, operation process, and working principles of activated carbon powder conveyors, industries can optimize their processes and achieve better results. With proper maintenance and regular troubleshooting, these machines can provide long-term performance and reliability, making them a valuable investment for any industrial operation.