

Principle and Working Scene Characteristics of Organic Salt Material Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for organic salt materials. These systems represent a sophisticated solution for material handling, offering efficient, dust-free, and flexible transport solutions that address the unique challenges associated with handling organic salts in industrial settings.
The Core Principle of Pneumatic Conveying Systems
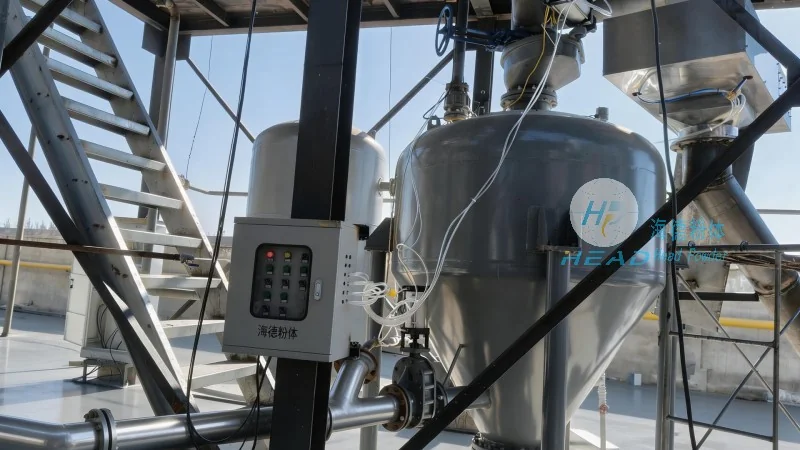
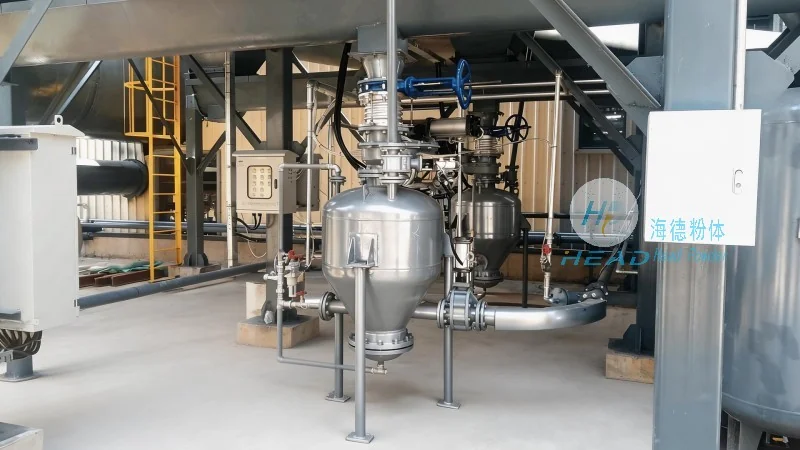
The fundamental principle of pneumatic conveying systems involves the use of compressed air or gas to transport bulk materials through a pipeline. In the context of organic salt materials, this technology leverages the kinetic energy of the air stream to move particles from a source to a destination. The system typically consists of a hopper or feeder, a compressor, a pipeline network, and a discharge unit. The organic salt material is fed into the system, where it is entrained by the air flow and carried through the pipeline. The design of the system, including the air velocity, pipeline diameter, and material properties, is critical to ensuring efficient and reliable transport. The principle allows for continuous, unattended operation, reducing labor costs and improving process safety by eliminating manual handling of potentially dusty or hazardous materials.
Key Working Scene Characteristics
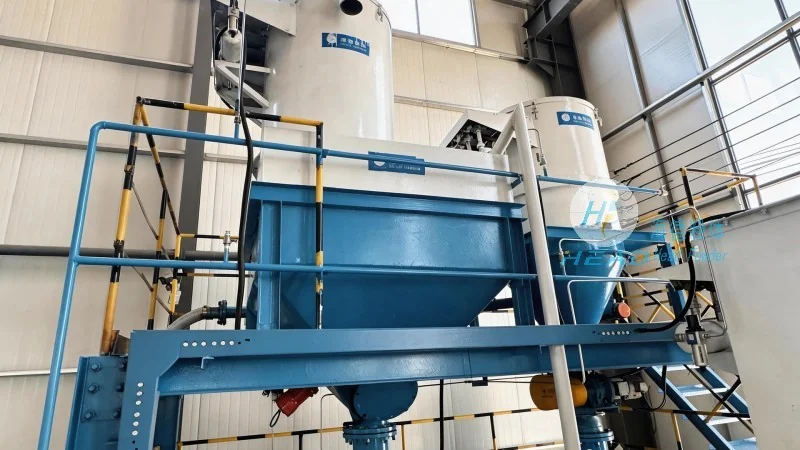
Organic salt material pneumatic conveying systems are characterized by several distinct working scene features that make them suitable for a variety of industrial applications. First, the systems are designed to handle materials with varying particle sizes and moisture content, which is common in organic salt processing. The flexible pipeline layout enables easy integration into existing production lines or new facility designs, adapting to different spatial constraints and operational requirements. Second, the dust-free operation is a significant advantage, as organic salts can be hygroscopic or generate fine particles that pose health and safety risks. The enclosed system prevents dust dispersion, complying with environmental regulations and improving workplace conditions. Third, the systems offer high transport efficiency, with the ability to move large volumes of material over long distances with minimal energy consumption compared to traditional methods like belt conveyors or bucket elevators. This efficiency translates into cost savings and increased productivity for industrial operations.
Application Scenarios and Operational Advantages
These pneumatic conveying systems are widely applied in various industrial sectors where organic salt materials are processed. For instance, in the chemical industry, they are used to transport raw organic salts to reactors or storage tanks, ensuring a consistent feed rate and preventing material degradation. In the food processing industry, the systems handle organic salt products, maintaining hygiene standards and preventing contamination. The systems are also utilized in the pharmaceutical sector for transporting raw materials to production lines, where precision and cleanliness are paramount. The operational advantages extend beyond efficiency and safety; the systems provide real-time monitoring capabilities, allowing operators to track material flow and detect potential issues such as blockages or pressure drops. This monitoring enhances process control and reduces downtime, contributing to overall operational reliability.
Conclusion and Company Expertise
Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in engineering and material handling to provide customized pneumatic conveying solutions for organic salt materials. By understanding the unique properties of organic salts and the specific requirements of industrial applications, the company designs systems that optimize performance, safety, and cost-effectiveness. The company's commitment to innovation and adherence to industry standards ensures that clients receive reliable, efficient, and sustainable material transport solutions tailored to their needs. With a focus on practical application and customer satisfaction, HeadPowder Engineering continues to be a trusted partner in the development of advanced material handling systems for the organic salt industry.