

Principle and Working Scene Characteristics of Tote Bag Packaging Powder Conveying Machines
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder handling equipment. Among their product lineup, the tote bag packaging powder conveying machine stands out as a critical solution for efficient material transport and storage in various industrial applications. This article delves into the operational principles and key characteristics of these machines, highlighting their role in modern powder processing workflows.
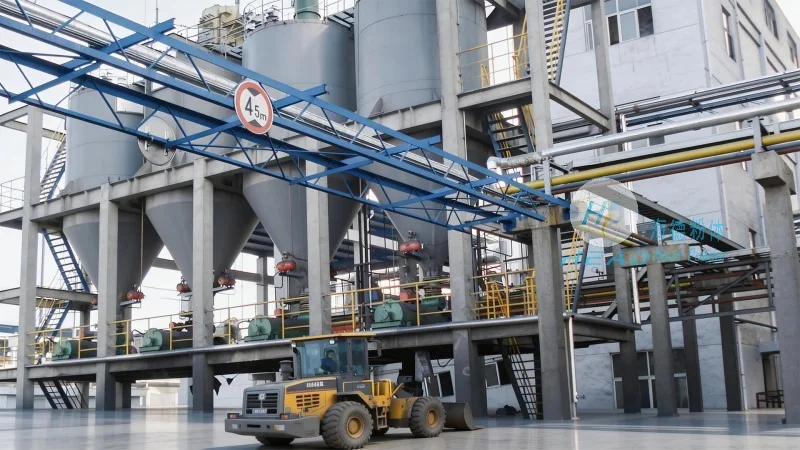
Introduction to Tote Bag Packaging Powder Conveying Machines
The tote bag packaging powder conveying machine is a specialized system engineered to handle bulk powders, granules, and other particulate materials. It integrates several key components, including a tote bag loading mechanism, a conveying system, and a control unit, to facilitate seamless material transfer from the source to the destination. The system is designed to operate efficiently in environments where large volumes of powders need to be moved, often in conjunction with tote bag packaging and handling processes.
Principle of Operation
The core principle of the tote bag packaging powder conveying machine revolves around the use of a positive displacement or pneumatic conveying system to move materials through a sealed pipeline. The process typically begins with the loading of the material into a tote bag, which is then positioned under the loading port of the conveying machine. As the material is discharged from the tote bag, it is drawn into the conveying line by a vacuum or pressure differential, depending on the system design. The conveying line may include components such as rotary valves, airlocks, and filters to ensure consistent flow and prevent material degradation or contamination. The control unit monitors and regulates the flow rate, pressure, and other parameters to maintain optimal performance and ensure the safe and efficient transfer of the material.
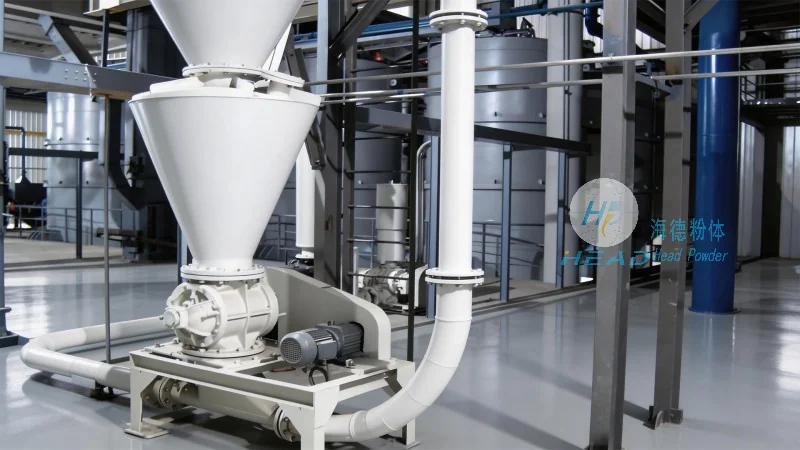
Key Working Scene Characteristics
Several distinct characteristics define the working scenes where tote bag packaging powder conveying machines are employed. Firstly, these machines are typically used in industrial settings that require the handling of large quantities of powders, such as chemical plants, food processing facilities, and pharmaceutical manufacturing sites. The ability to handle bulk materials without the need for manual intervention is a significant advantage, as it reduces labor costs and minimizes the risk of human error. Secondly, the system is designed to operate in a clean and controlled environment, which is essential for industries where product purity and contamination control are paramount. The sealed conveying system prevents dust and particles from escaping into the air, ensuring compliance with environmental regulations and maintaining product quality. Thirdly, the machine's modular design allows for easy integration with existing production lines, making it a versatile solution for both new and existing facilities. This adaptability is crucial for companies looking to upgrade their material handling capabilities without significant infrastructure changes.
Application Scenarios
The tote bag packaging powder conveying machine finds applications in a wide range of industries where bulk powder handling is essential. In the chemical industry, it is commonly used to transport raw materials like powders and granules to processing units, ensuring a continuous supply of materials for production. In the food and beverage sector, the machine is employed to handle ingredients such as flour, sugar, and spices, maintaining the integrity and freshness of the products. The pharmaceutical industry also relies on these systems to transport active pharmaceutical ingredients (APIs) and other powders, adhering to stringent quality and safety standards. Additionally, in the agricultural sector, the machine can be used to handle fertilizers and other agricultural chemicals, supporting efficient farming operations. Each of these applications benefits from the machine's ability to handle large volumes of powders efficiently and safely, reducing downtime and improving overall operational efficiency.
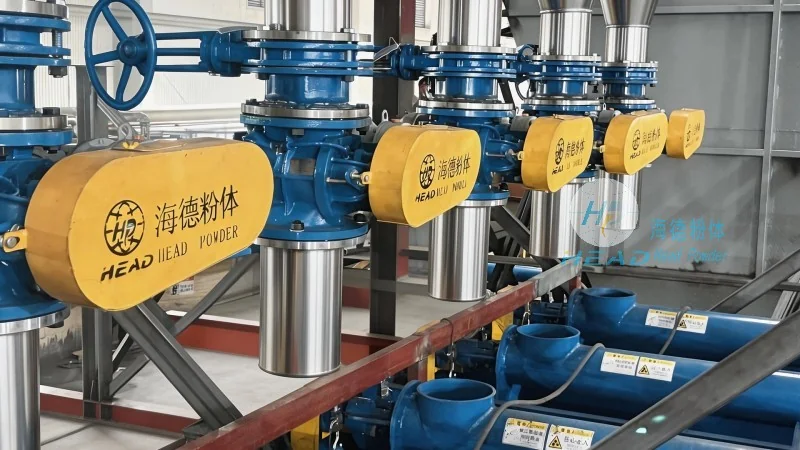
Advantages in Modern Powder Processing
Implementing a tote bag packaging powder conveying machine offers several advantages in modern powder processing. One of the primary benefits is the reduction in material handling time and labor costs. By automating the transfer of powders from tote bags to processing equipment, companies can significantly increase their production throughput. The system also minimizes the risk of material spillage and contamination, which is critical for maintaining product quality and regulatory compliance. Furthermore, the sealed conveying system helps to control dust emissions, improving workplace safety and reducing the environmental impact of the operation. The modular design of the machine allows for easy maintenance and repair, ensuring minimal downtime and maximizing the system's lifespan. These advantages make the tote bag packaging powder conveying machine an indispensable tool for companies operating in industries that rely on bulk powder handling.
Conclusion
HeadPowder's tote bag packaging powder conveying machine represents a sophisticated solution for efficient powder handling in various industrial applications. By understanding the operational principles and key characteristics of these machines, businesses can make informed decisions about integrating such systems into their production workflows. The machine's ability to handle large volumes of powders safely and efficiently, combined with its adaptability and reliability, makes it a valuable asset for companies seeking to enhance their material handling capabilities. As industries continue to evolve and demand higher efficiency and quality in powder processing, the role of advanced conveying systems like this will only become more critical.