

Principles and Application Scenarios of Fine Chemical Powder Conveying Machines
For industries dealing with fine chemicals, efficient and reliable powder conveying is crucial for maintaining production efficiency and product quality. The fine chemical powder conveying machine, developed by Shandong HeadPowder Engineering Co., Ltd., is a specialized equipment designed to handle the unique challenges of transporting fine powders in chemical processing environments. This article will explore the fundamental principles behind these machines and highlight their key operational characteristics and typical application scenarios.
Company Overview
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer in the field of powder handling equipment. With its headquarters located in Shandong, China, the company specializes in the research, development, and production of advanced conveying systems tailored for various industrial applications. HeadPowder's commitment to innovation and quality has positioned it as a trusted partner for businesses seeking reliable solutions for powder transportation in demanding environments.
Principles of Fine Chemical Powder Conveying Machines
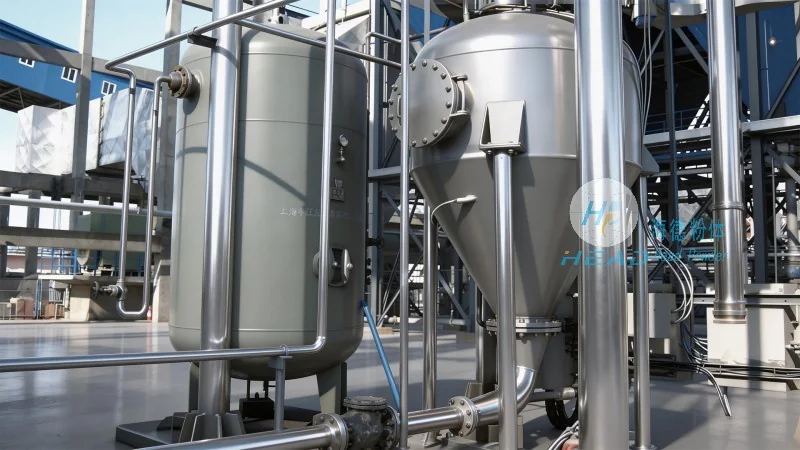
The core principle of fine chemical powder conveying machines is to transport powders from one location to another while maintaining the integrity of the material. These machines are engineered to handle fine powders, which often present challenges such as dust generation, caking, and agglomeration. The design incorporates several key mechanisms to address these issues, including air pressure control, material separation, and consistent flow regulation. By utilizing a combination of pneumatic and mechanical components, the equipment ensures that powders are conveyed smoothly without degradation or loss of quality. The system typically operates by creating a pressure differential between the inlet and outlet, allowing the powder to be transported through a pipeline network. This pneumatic approach is particularly effective for fine powders, as it minimizes mechanical stress and prevents particle breakage, which could alter the chemical properties of the material.
Working Characteristics and Operational Features
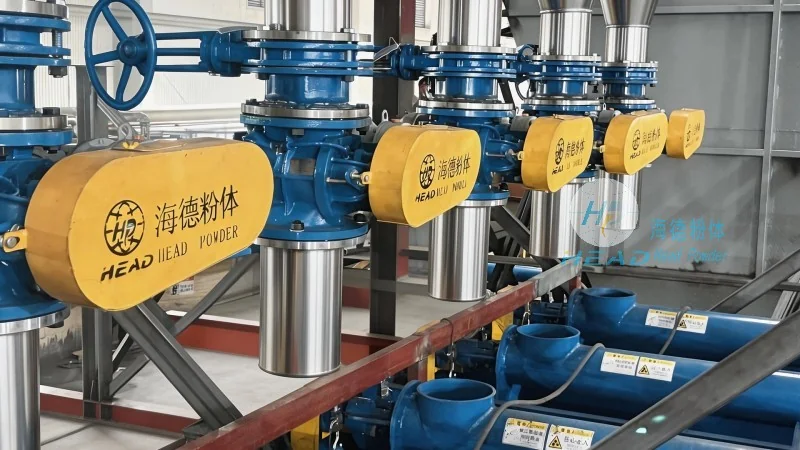
Fine chemical powder conveying machines from HeadPowder are characterized by several operational features that enhance their performance and adaptability. One of the primary features is the ability to handle a wide range of powder types, from highly fine powders with particle sizes as small as microns to slightly coarser materials. The equipment is designed to maintain a consistent flow rate, which is critical for processes that require precise material delivery. Additionally, the machines are equipped with advanced control systems that allow for real-time monitoring and adjustment of conveying parameters. This ensures that the system operates efficiently and can be quickly adjusted to accommodate changes in production demand or material characteristics. The design also emphasizes safety and maintenance, with features such as dust collection systems and easy access for routine checks and maintenance. These features help to minimize downtime and ensure long-term reliability in industrial settings.
Key Application Scenarios
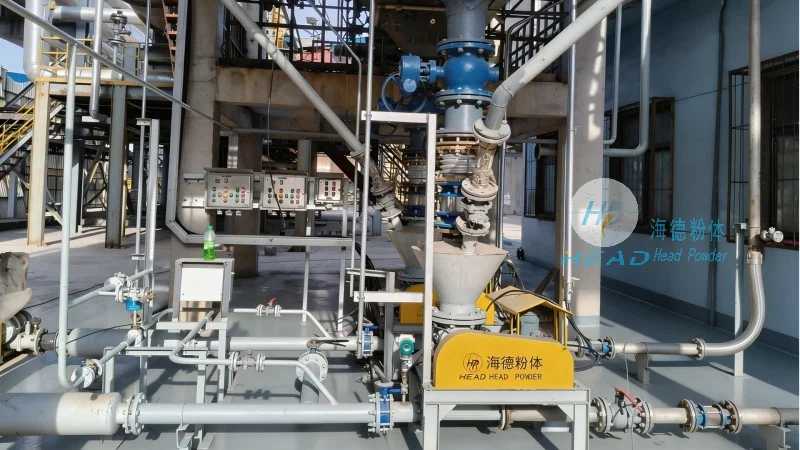
The fine chemical powder conveying machines are widely used in various industrial sectors, particularly in the chemical and pharmaceutical industries. In chemical manufacturing, these machines are essential for transporting raw materials and intermediates between processing stages, ensuring a continuous and controlled production flow. The pharmaceutical industry benefits from the equipment's ability to handle sensitive powders, maintaining the purity and integrity of active ingredients during transportation. Other applications include food processing, where fine powders such as spices or flavorings are conveyed, and in the production of cosmetics, where the equipment ensures that powders are handled hygienically and without contamination. The versatility of the machines makes them suitable for both large-scale industrial operations and smaller-scale laboratory applications, providing flexibility for different production needs.
Advantages and Benefits
Implementing fine chemical powder conveying machines offers several advantages for businesses operating in the fine chemical sector. The primary benefit is the improvement in production efficiency, as the equipment enables seamless and continuous material flow, reducing bottlenecks and increasing throughput. Additionally, the machines help to maintain product quality by minimizing material degradation and contamination during transportation. This is particularly important for fine chemicals, where even minor changes in particle size or composition can affect the final product's performance. The equipment also contributes to operational safety by reducing the need for manual handling of powders, which can pose health and safety risks. Furthermore, the advanced control systems allow for energy-efficient operation, helping to lower operational costs and reduce the environmental impact of the conveying process. Overall, the fine chemical powder conveying machines from HeadPowder provide a reliable and efficient solution for the transportation of fine powders, supporting the success of industrial operations in the chemical and related industries.