

Principles and Operational Characteristics of Calcite Pneumatic Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design, development, and supply of advanced pneumatic conveying systems tailored for various industrial applications. The company's expertise lies in optimizing material handling processes, particularly for calcite and other similar bulk materials, ensuring efficient and reliable transportation solutions.
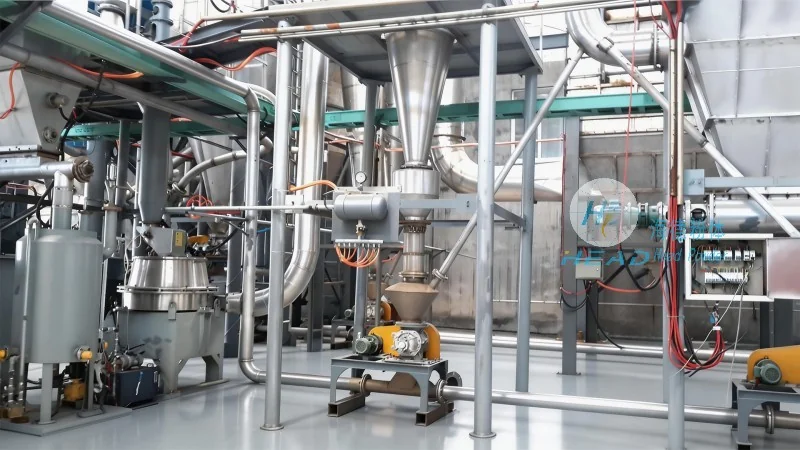
Overview of Pneumatic Conveying Systems
Pneumatic conveying systems are mechanical devices that utilize air or gas to transport bulk materials from one location to another. Unlike traditional methods such as belt conveyors or screw conveyors, these systems offer a flexible and enclosed solution for moving powders and granules. The core components typically include a hopper, a blower or compressor, a pipeline network, and a discharge device. By creating a pressure differential, the system draws or pushes the material through the pipeline, enabling seamless material transfer.
Principles of Operation
The fundamental principle of a pneumatic conveying system is the use of air flow to move material particles. In a typical positive pressure system, a blower generates high-pressure air that forces the material from the hopper into the pipeline. The material is then carried by the air stream, often in a dilute phase, where the particles are suspended and transported. Conversely, in a negative pressure (or vacuum) system, a vacuum pump creates a low-pressure environment that draws material from the source into the pipeline. The choice between positive and negative pressure depends on factors like material properties, distance, and system layout. For calcite, a common industrial mineral, the system must be designed to handle its specific characteristics, such as particle size, density, and flowability.
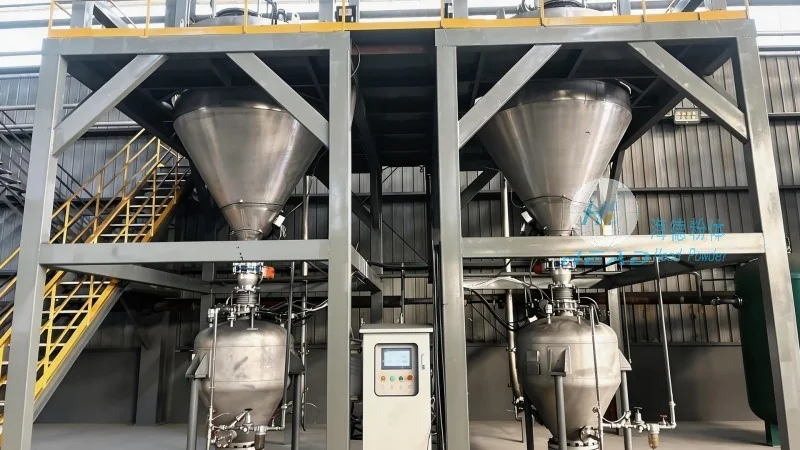
Operational Characteristics and Application Scenarios
The operational characteristics of calcite pneumatic conveying systems are tailored to meet the demands of different industrial environments. These systems are widely used in industries such as mining, construction, and chemical processing, where calcite is a key raw material. The key features include high efficiency in material transport, minimal product contamination due to enclosed pipelines, and the ability to handle materials with varying properties. For example, in a calcite processing plant, the system can efficiently transport raw calcite from storage silos to grinding mills or packaging units. The enclosed design prevents dust emissions, ensuring compliance with environmental regulations. Additionally, the system's flexibility allows for integration with other processing equipment, such as crushers, classifiers, and mixers, creating a streamlined production line.
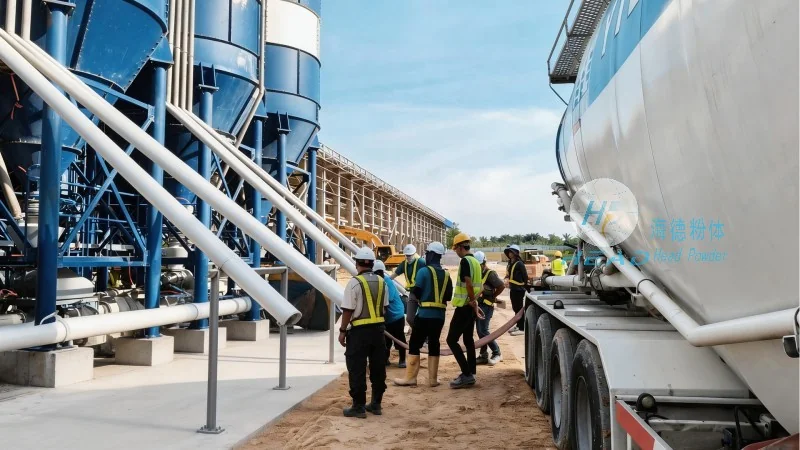
Key Advantages in Calcite Handling
When applied to calcite, pneumatic conveying systems offer several advantages over traditional methods. First, they reduce labor costs by automating the material handling process, minimizing the need for manual loading and unloading. Second, the enclosed system prevents dust and particle loss, maintaining product quality and safety standards. Third, the system's ability to handle high volumes of material efficiently improves overall production throughput. Moreover, the flexibility of the pipeline network allows for easy reconfiguration or expansion of the system as production needs change. In the context of Shandong HeadPowder Engineering Co., Ltd., the company's expertise in customizing these systems ensures that clients receive solutions optimized for their specific calcite handling requirements, whether for small-scale operations or large industrial facilities.
Conclusion
Calcite pneumatic conveying systems, as provided by Shandong HeadPowder Engineering Co., Ltd., represent a sophisticated solution for efficient material handling in various industrial applications. By leveraging the principles of pneumatic transport, these systems offer reliable, flexible, and environmentally friendly methods for moving calcite and other bulk materials. The company's commitment to quality and customization ensures that clients receive systems tailored to their operational needs, enhancing productivity and compliance with industry standards. With a strong presence in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. continues to be a trusted partner for businesses seeking advanced material handling solutions.