

Working Principle and Features of Maltose Material Pneumatic Conveying Equipment
The maltose material pneumatic conveying equipment is a specialized system designed to transport maltose, a common sugar derived from starch hydrolysis, efficiently and safely. This equipment utilizes pneumatic conveying technology, which involves the movement of bulk materials through a pipeline using air or gas as the conveying medium. For maltose, which is often in a granular or powdered form, such systems offer a non-contact, hygienic, and efficient method of handling compared to traditional mechanical conveyors.
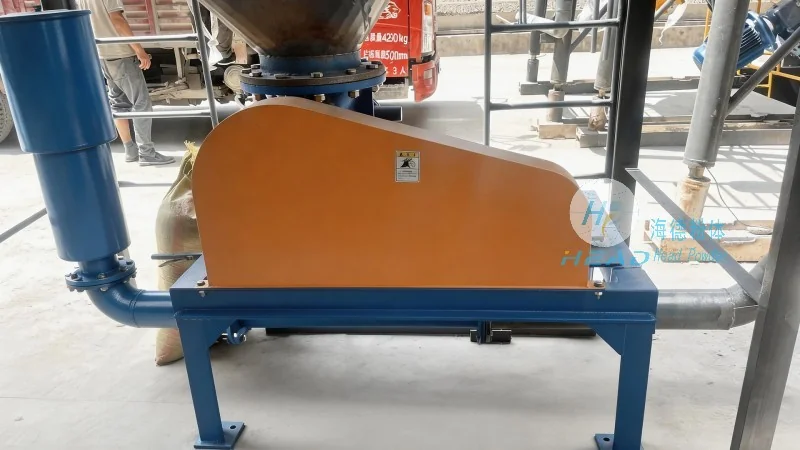
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the powder and bulk material handling industry, specializes in developing and supplying advanced pneumatic conveying solutions. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner for businesses requiring reliable and efficient material transport systems. HeadPowder's facilities are located in Shandong, China, where the company leverages local expertise and resources to deliver high-quality products tailored to specific industry needs.
Working Principle of Pneumatic Conveying Systems for Maltose
The core working principle of the maltose pneumatic conveying equipment revolves around the use of air pressure to move the material. In typical systems, there are two main modes: suction (or negative pressure) and pressure (or positive pressure) conveying. For maltose, which is often handled in a dry, free-flowing state, suction conveying is commonly employed. The process begins with the material being drawn into a hopper or feeding device by a vacuum created by a fan or blower. The material is then carried through the pipeline by the moving air stream, which transports it to the destination point, such as a storage silo, processing unit, or packaging area.
Key Features and Advantages of the Equipment
The maltose pneumatic conveying equipment from HeadPowder offers several distinct features and advantages that make it suitable for handling maltose and similar bulk materials. One of the primary benefits is its hygienic design, which is crucial for food-grade products like maltose. The system typically includes stainless steel components, smooth surfaces, and easy-to-clean features to prevent contamination and ensure compliance with food safety regulations. Additionally, the equipment is designed for high efficiency, with minimal material loss and low energy consumption compared to traditional methods.
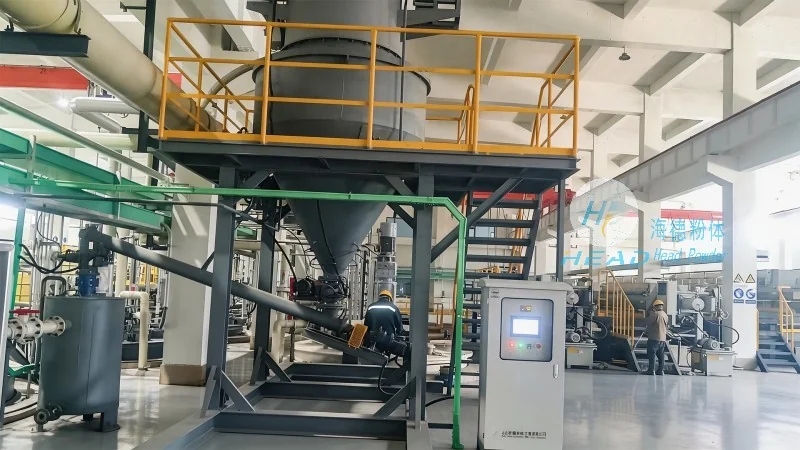
Another key feature is the flexibility in conveying distances and heights. The pneumatic system can transport maltose over long distances and vertical elevations, making it ideal for large-scale production facilities where material needs to be moved between different levels or locations. The system also provides excellent control over the flow rate, allowing for precise dosing and regulation of the material, which is essential for consistent product quality.
Furthermore, the equipment is equipped with advanced monitoring and control systems. These systems enable operators to track the conveying process in real-time, detect any blockages or issues, and adjust the system parameters as needed. This proactive approach ensures continuous and reliable operation, minimizing downtime and maximizing productivity.
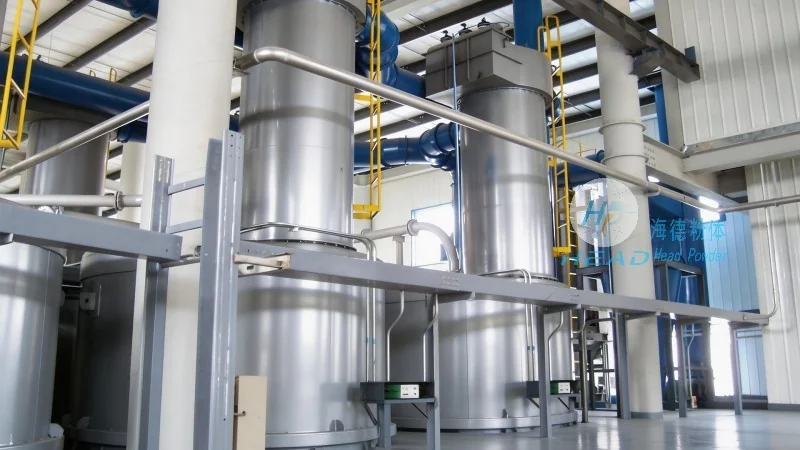
Application Scenarios and Benefits
The maltose pneumatic conveying equipment is widely used in various industries, particularly in the food and beverage sector, where maltose is a key ingredient in products such as syrups, candies, and baked goods. In these applications, the equipment helps streamline the production process by efficiently moving maltose from storage to processing lines, reducing manual handling and associated risks.
The benefits of using this equipment extend beyond just efficiency. By eliminating the need for manual handling, the system reduces the risk of product contamination and improves workplace safety. The hygienic design also helps maintain the quality and purity of the maltose, which is critical for maintaining consumer trust and meeting regulatory standards.
In summary, the maltose material pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for the efficient and safe handling of maltose. With its advanced working principles, hygienic design, and versatile features, the system addresses the specific needs of the food industry while ensuring high performance and reliability.