

Working Principle and Features of High-Calcium Powder Material Pneumatic Conveying Equipment
High-calcium powder, a critical raw material in various industrial sectors such as cement production, chemical processing, and food manufacturing, requires efficient and reliable transportation methods to maintain product quality and operational efficiency. The high-calcium powder pneumatic conveying equipment, developed by Shandong HeadPowder Engineering Co., Ltd., addresses these challenges by providing a robust solution for material handling. This article explores the working principle and key features of this advanced equipment, highlighting its benefits for industrial applications.
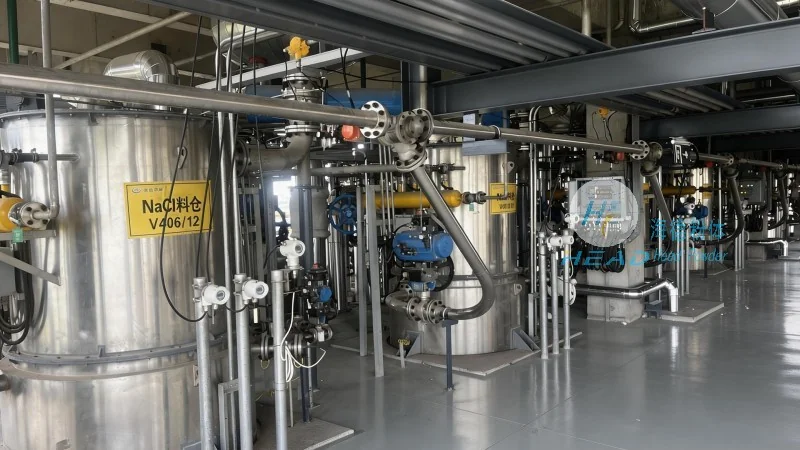
Introduction to High-Calcium Powder Pneumatic Conveying Equipment
High-calcium powder, characterized by its fine particle size and high reactivity, demands specialized handling equipment to prevent agglomeration, dust generation, and material degradation. The pneumatic conveying system offered by HeadPowder is engineered to meet these stringent requirements, ensuring safe and efficient transport of the powder from storage to processing units. This equipment is designed to handle high-volume material flows while maintaining consistent pressure and flow rates, making it suitable for continuous production lines.
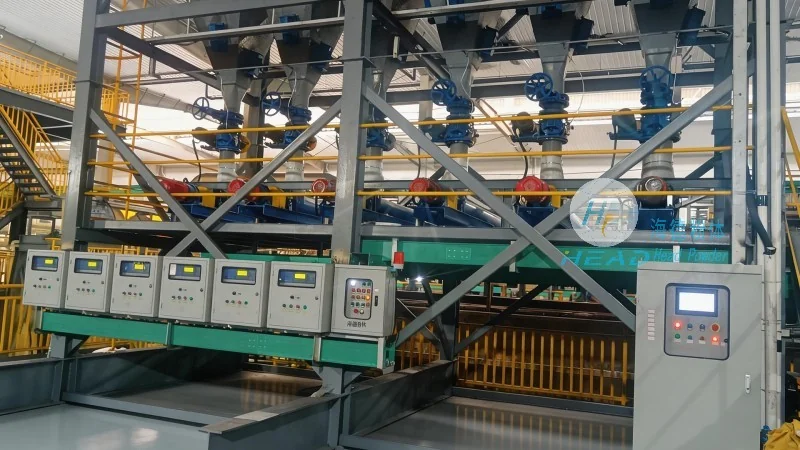
Working Principle of the High-Calcium Powder Pneumatic Conveying System
The core of the high-calcium powder pneumatic conveying system is the air flow mechanism that propels the powder through a network of pipes. The process begins with the powder being fed into a hopper or feeder, where it is then introduced into a pipeline. A high-pressure air source, typically a blower or compressor, generates the necessary airflow to move the powder particles. The air and powder mixture travels through the conveying line, with the air velocity maintained at a level sufficient to keep the powder suspended and prevent clogging. The system may include components such as a rotary valve, a filter, and a receiver, which work in tandem to ensure smooth material transport and dust control. The working principle is based on the principle of fluidization, where the powder particles are suspended in the air stream, allowing for efficient and low-friction movement. This method eliminates the need for mechanical components like belts or screws, reducing maintenance costs and increasing operational reliability.
Key Features of the High-Calcium Powder Pneumatic Conveying Equipment
HeadPowder's high-calcium powder pneumatic conveying equipment is equipped with several advanced features that enhance its performance and adaptability. One of the primary features is the adjustable air pressure and flow control system, which allows operators to optimize the conveying parameters based on the specific characteristics of the high-calcium powder. This flexibility ensures that the system can handle varying particle sizes and moisture content without compromising efficiency. Another key feature is the integrated dust collection and filtration system, which prevents dust emissions and maintains a clean working environment. The equipment also includes a material recovery system, which recovers any powder that may be lost during the conveying process, reducing material waste and improving overall efficiency. Additionally, the system is designed with corrosion-resistant materials to withstand the chemical properties of high-calcium powder, ensuring long-term durability and minimal maintenance. The compact design of the equipment makes it suitable for installation in limited space, and the modular construction allows for easy integration into existing production lines.
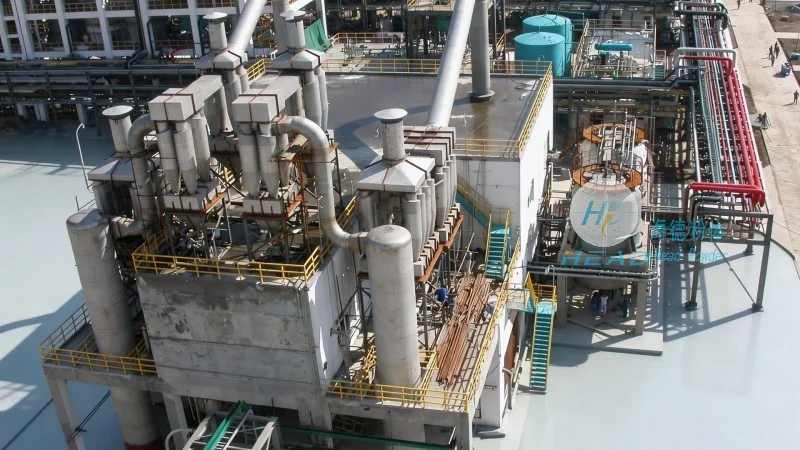
Benefits and Applications of the High-Calcium Powder Pneumatic Conveying System
The implementation of the high-calcium powder pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers numerous benefits to industrial operations. The primary advantage is the significant reduction in material handling time and labor costs, as the system automates the transport process. This leads to increased production throughput and improved overall efficiency. The equipment also minimizes product contamination and degradation, as the enclosed system prevents exposure to external elements and reduces the risk of dust inhalation. Furthermore, the system's low maintenance requirements and long service life contribute to lower operational costs over time. The high-calcium powder pneumatic conveying system is widely used in the cement industry for transporting raw materials, in chemical plants for handling reactive powders, and in food processing facilities for conveying high-calcium additives. Its versatility and reliability make it an essential component for any industrial process that involves the handling of fine, high-reactivity powders.