

Working Principle and Features of Lightweight Cement Material Handling Systems
Lightweight cement material handling systems represent a sophisticated solution designed to efficiently transport and manage lightweight cementitious materials in various industrial applications. These systems are engineered to enhance operational efficiency, reduce energy consumption, and ensure consistent material flow in construction, manufacturing, and other sectors where lightweight cement products are utilized.
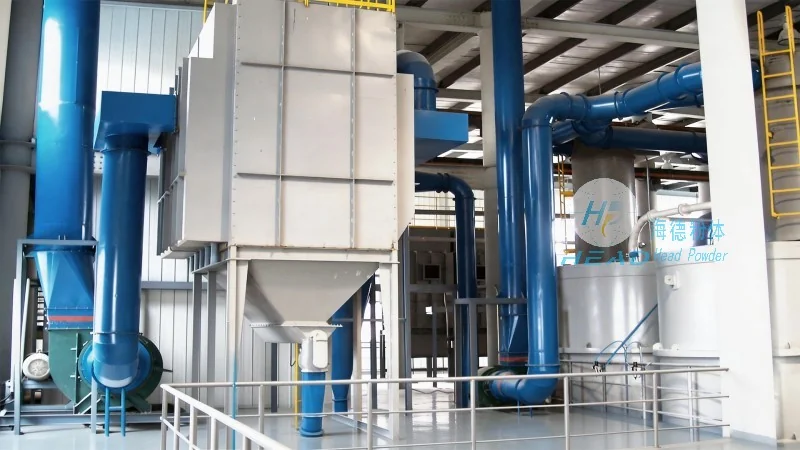
Overview of Lightweight Cement Material Handling Systems
At the core of these systems lies a combination of advanced engineering principles and specialized equipment tailored to handle lightweight cement materials, which often include aerated concrete, lightweight aggregate concrete, and other low-density cement products. The primary goal is to provide a reliable and efficient method for transporting these materials from storage to processing or application points, minimizing downtime and maximizing productivity.
Working Principle of Lightweight Cement Material Handling Systems
The working principle of a typical lightweight cement material handling system involves several key components and processes. Initially, the lightweight cement material is stored in bulk storage silos or hoppers, where it is kept in a dry and consistent condition. From there, the material is fed into a conveyor system, which may include belt conveyors, screw conveyors, or pneumatic conveying lines, depending on the specific system design and material characteristics.
For systems utilizing mechanical conveyors, such as belt or screw conveyors, the material is transported through a series of rollers or flights that move the material along a designated path. This method is particularly effective for handling bulk materials with moderate flowability and requires minimal maintenance. In contrast, pneumatic conveying systems use air pressure to transport the lightweight cement material through a network of pipes, which is ideal for materials that are more dusty or have lower bulk density.
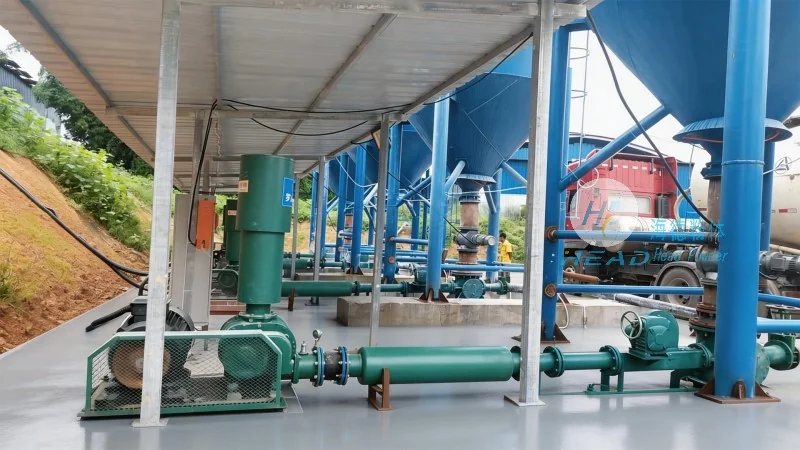
Once the material reaches the processing or application stage, it may be further processed through additional equipment like mixers, classifiers, or dispensing units. The entire system is typically controlled by a centralized control panel, allowing operators to monitor and adjust the flow rate, pressure, and other parameters to maintain optimal performance. This integrated approach ensures that the material is handled consistently and efficiently throughout the entire process.
Key Features of Lightweight Cement Material Handling Systems
Lightweight cement material handling systems are characterized by several distinct features that set them apart from traditional handling solutions. One of the most notable features is their ability to handle low-density materials with high efficiency, which is crucial for lightweight cement products that often have a lower bulk density compared to standard cement. This is achieved through specialized conveyor designs and air flow management in pneumatic systems.
Another key feature is the system's adaptability to different material types and processing requirements. Many modern systems are equipped with modular components that can be easily reconfigured to accommodate changes in material characteristics or production needs. This flexibility allows manufacturers to scale their operations without significant capital investment or system overhauls.
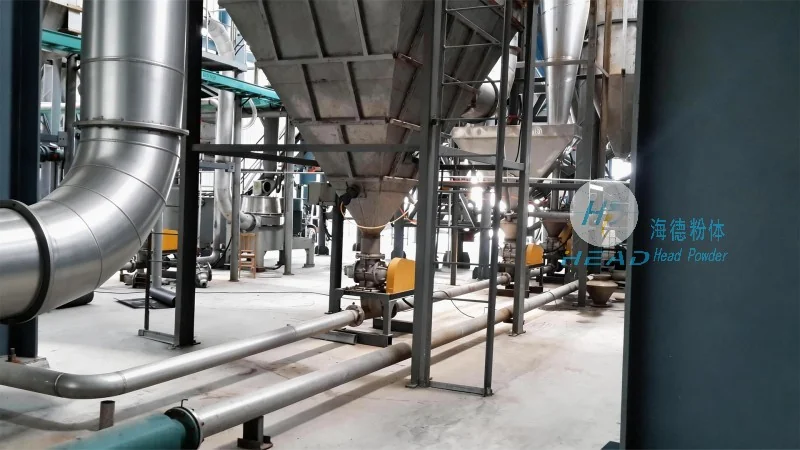
Energy efficiency is also a prominent feature of these systems, as they are designed to minimize energy consumption while maintaining high throughput. Advanced control systems and optimized conveyor designs help reduce power usage, contributing to lower operational costs and a smaller environmental footprint. Additionally, the systems often incorporate dust control measures, such as sealed conveyor sections and air filtration systems, to ensure a safe and clean working environment.
Applications and Benefits in Industrial Settings
Lightweight cement material handling systems find widespread application in various industrial sectors, including construction, precast concrete manufacturing, and building materials production. In construction projects, these systems are used to transport lightweight cement mixes to job sites, ensuring consistent material quality and reducing the need for manual handling, which can be labor-intensive and inefficient.
In precast concrete plants, the systems play a critical role in moving lightweight aggregate and cement mixes to mixing and casting stations. This streamlined material flow enhances production speed and reduces the risk of material segregation or contamination, which can affect the final product's quality and performance.
For building materials manufacturers, the systems help in the efficient handling of lightweight cement products during storage, packaging, and distribution. The ability to maintain consistent material properties and minimize handling-related losses is essential for meeting quality standards and customer expectations.
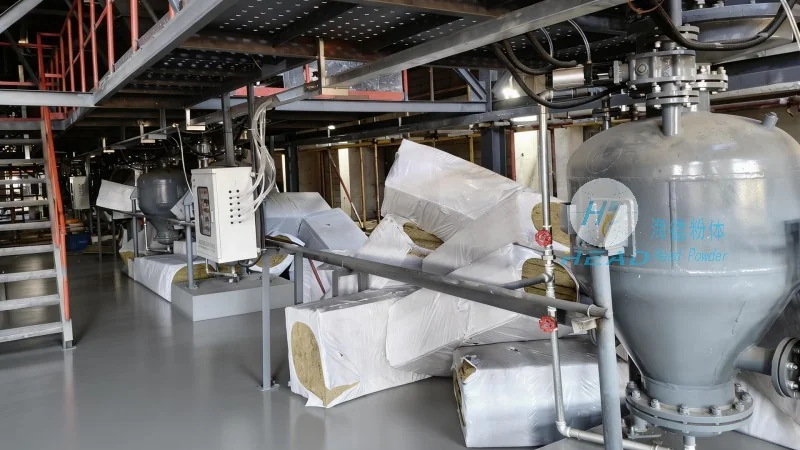
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced material handling systems, including lightweight cement material handling solutions. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the construction and building materials industry.
HeadPowder's lightweight cement material handling systems are designed and manufactured based on extensive research and practical experience in the field. The company's engineering team works closely with clients to understand their specific operational needs and develop customized solutions that meet their unique requirements. This customer-centric approach has helped HeadPowder build a reputation for delivering high-quality, reliable, and efficient material handling systems.
HeadPowder is committed to providing comprehensive support to its clients, from system design and installation to ongoing maintenance and technical assistance. The company's facilities are equipped with state-of-the-art technology and skilled personnel, ensuring that every product meets the highest standards of quality and performance. With a presence in China, HeadPowder serves clients both domestically and internationally, offering solutions tailored to diverse industrial applications.