

Working Principle and Features of Fertilizer Pneumatic Conveying Systems
For agricultural and industrial applications, efficient and reliable material handling is crucial, especially when dealing with bulk fertilizers. The fertilizer pneumatic conveying system, offered by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution designed to meet these demands. This article explores the working principle and key features of such systems, highlighting how they enhance operational efficiency and safety in fertilizer processing and distribution.
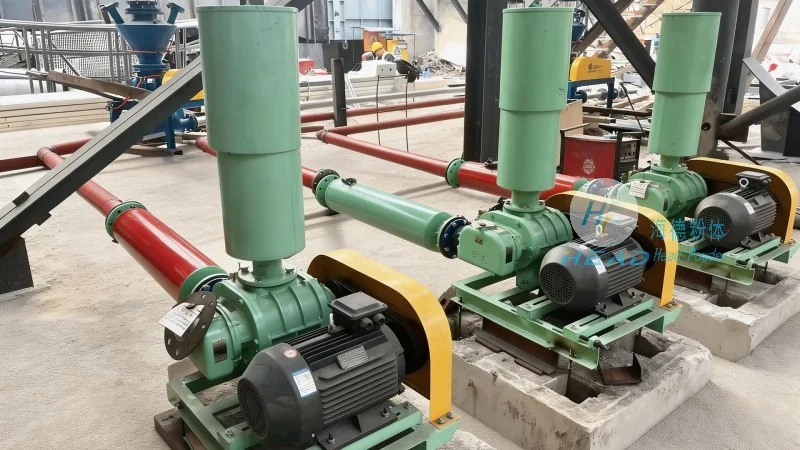
Understanding the Working Principle of Fertilizer Pneumatic Conveying Systems
The core of a fertilizer pneumatic conveying system lies in its ability to transport bulk materials like fertilizers through an enclosed pipeline using air pressure. The system typically operates on one of two principles: positive pressure or negative pressure. In positive pressure systems, a fan or blower generates air pressure that pushes the material through the pipeline. This method is ideal for long-distance or high-capacity transport, as it can maintain consistent flow rates and handle abrasive materials without excessive wear. Conversely, negative pressure systems use a vacuum to draw material into the pipeline, which is often preferred for shorter distances or when the material is sensitive to pressure changes. The system comprises several key components, including a hopper for material storage, a feeder to control the flow rate, a conveying line (usually made of stainless steel or other corrosion-resistant materials to withstand chemical exposure), and a receiver where the material is deposited. The air flow is regulated by a control valve to ensure optimal pressure and flow, preventing blockages and maintaining system efficiency.
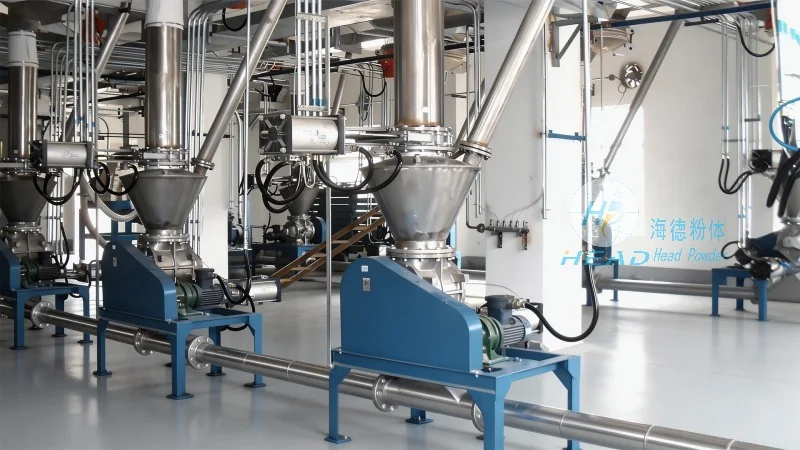
Key Features of Fertilizer Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd. designs and manufactures fertilizer pneumatic conveying systems with several distinct features that set them apart in the industry. First, the systems are built for durability and longevity, utilizing high-quality materials that resist corrosion and wear from abrasive fertilizers. This ensures low maintenance costs and extended operational life. Second, the systems offer flexibility in terms of layout and capacity, allowing customization to fit specific site requirements and production volumes. Whether for small-scale farm operations or large industrial facilities, the conveying lines can be adjusted to handle varying amounts of material. Third, safety is a top priority, with features such as automatic shut-off valves to prevent overpressure or vacuum, and dust collection systems to minimize environmental impact and protect personnel. Additionally, the systems are equipped with monitoring and control panels that allow operators to track performance in real-time, ensuring quick response to any issues and maintaining optimal efficiency. Another notable feature is the energy efficiency of modern pneumatic conveying systems, which use less power compared to traditional mechanical conveyors, reducing operational costs over time.
Benefits of Implementing Fertilizer Pneumatic Conveying Systems
Adopting a fertilizer pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. brings numerous benefits to agricultural and industrial operations. The primary advantage is enhanced productivity, as the systems can transport large volumes of material quickly and continuously, reducing downtime and increasing throughput. This is particularly valuable in fertilizer production facilities where speed and efficiency directly impact profitability. Additionally, the systems improve safety by eliminating the need for manual handling of bulk materials, which reduces the risk of accidents and exposure to dust or chemicals. The enclosed pipeline design also minimizes environmental contamination, as dust and particles are contained within the system rather than being released into the air. Furthermore, the systems are highly adaptable, allowing seamless integration with existing production lines and future expansion as business needs grow. The durability and low maintenance requirements of these systems contribute to long-term cost savings, as they require fewer repairs and replacements compared to other conveying methods. Overall, the investment in a fertilizer pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. is a strategic decision that enhances operational efficiency, safety, and sustainability.
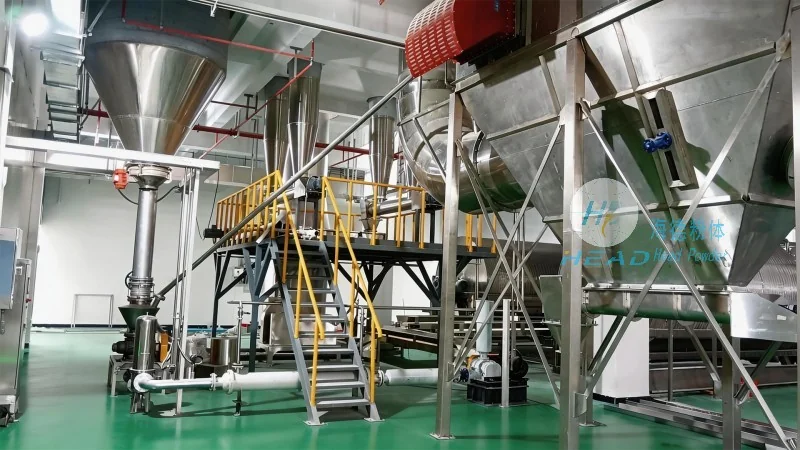
Conclusion and Company Information
In conclusion, fertilizer pneumatic conveying systems are a vital component in modern fertilizer handling and distribution, offering a reliable and efficient solution to material transport challenges. Shandong HeadPowder Engineering Co., Ltd., with its expertise in engineering and manufacturing, provides high-quality systems that combine advanced technology with robust design. Based in Shandong, China, the company leverages its local resources and industry knowledge to deliver tailored solutions that meet the specific needs of its clients. Whether for agricultural or industrial applications, the systems from Shandong HeadPowder Engineering Co., Ltd. are designed to enhance productivity, ensure safety, and promote sustainable operations. By choosing a fertilizer pneumatic conveying system from this company, businesses can expect long-term performance and cost-effectiveness, supporting their growth and success in the fertilizer industry.