

Working Principle and Features of Intelligent Bag-Opening Pneumatic Conveying Equipment
Intelligent bag-opening pneumatic conveying equipment represents a sophisticated solution in material handling, designed to streamline the process of transferring bulk materials from sealed bags to processing or storage systems. This technology integrates advanced automation and control mechanisms, enhancing efficiency and reducing operational risks in industrial settings. The equipment is particularly valuable in industries such as food, pharmaceuticals, chemicals, and powders, where maintaining product integrity and hygiene is critical.
Working Principle of the Equipment
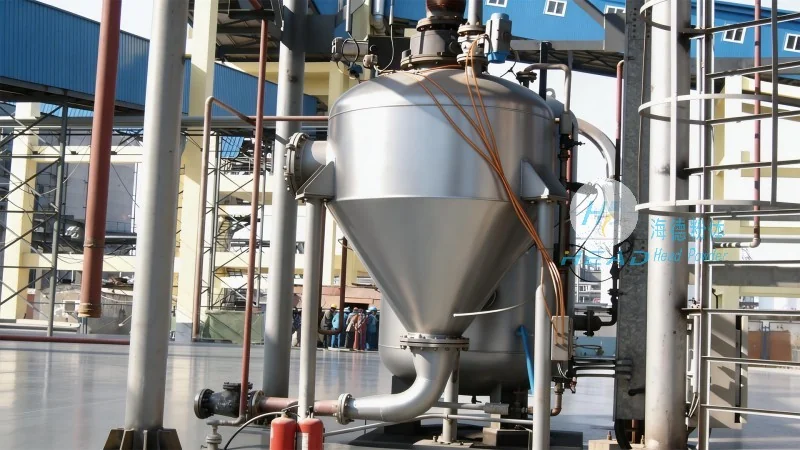
The core operation of intelligent bag-opening pneumatic conveying equipment involves several key steps, each optimized for reliability and precision. Initially, the sealed bag is positioned and secured by the equipment's mechanical system. A controlled opening mechanism then safely ruptures the bag, allowing the contents to flow into a hopper or collection chamber. Simultaneously, a pneumatic conveying system—typically utilizing air or gas as the medium—propels the material through a network of pipes to the desired destination. The system employs differential pressure and air flow management to ensure consistent material transport, with sensors monitoring flow rates and pressure to maintain optimal performance. This integrated approach minimizes manual intervention and enhances safety by automating the entire bag-to-pipe transfer process. The equipment operates on the principle of pneumatic transport, which uses compressed air or vacuum to move bulk materials through a sealed pipeline system. The process begins with the placement of a sealed bag into the equipment's designated position. A mechanical arm or gripper secures the bag, and an automated cutting or puncturing tool opens the bag safely, allowing the material to flow into a hopper. The hopper is then connected to a pneumatic conveying system, which can be configured as either a vacuum (suction) or positive pressure (blowing) system. In a vacuum system, the hopper is connected to a vacuum pump that creates a low-pressure environment, drawing the material from the hopper into the conveying line. In a positive pressure system, a blower supplies high-pressure air that pushes the material through the pipes. The system includes a series of valves, filters, and sensors to regulate the air flow and material transport, ensuring consistent and controlled movement. The equipment also features a dust collection system to capture any airborne particles, maintaining a clean and safe working environment.
Key Features and Advantages
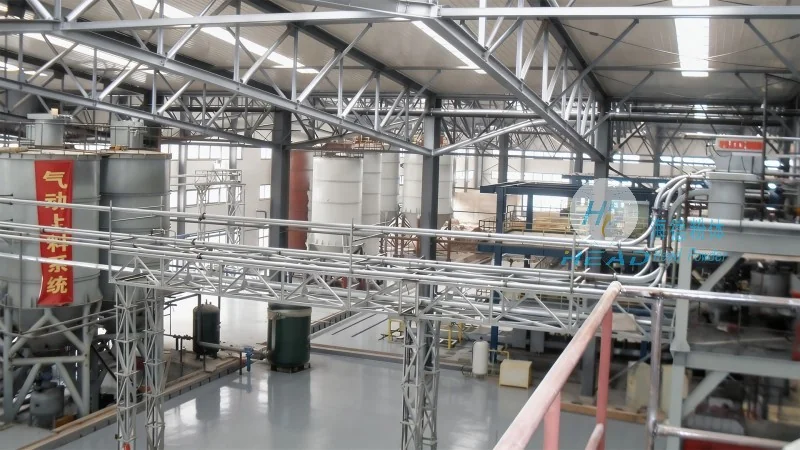
Intelligent bag-opening pneumatic conveying equipment offers numerous advantages that contribute to improved operational efficiency and product quality. One of the primary features is its ability to handle a wide range of bulk materials, including powders, granules, and fine particles, with minimal degradation. The automated bag-opening mechanism reduces the risk of contamination and spillage, which is crucial in industries where product purity is paramount. Additionally, the equipment is designed for high throughput, capable of processing large volumes of material in a short time, thereby increasing production capacity. The integrated control system allows for real-time monitoring and adjustment, ensuring consistent performance and reducing downtime. Another notable feature is the energy efficiency of the pneumatic conveying system, which uses less power compared to traditional mechanical conveying methods. This not only lowers operational costs but also aligns with sustainability goals in modern manufacturing. Furthermore, the equipment is constructed with durable materials and robust components, ensuring long-term reliability and minimal maintenance requirements. These features collectively make the intelligent bag-opening pneumatic conveying equipment a versatile and cost-effective solution for various industrial applications.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer specializing in the design, development, and supply of advanced material handling equipment. With a focus on innovation and customer-centric solutions, the company has established itself as a trusted partner in industries requiring efficient and reliable material transfer systems. HeadPowder's commitment to quality and technological advancement is reflected in its comprehensive product line, which includes pneumatic conveying systems, bag-openers, and related accessories. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-performance equipment tailored to global market needs. By adhering to stringent quality standards and providing comprehensive technical support, HeadPowder ensures that its clients receive products that meet their specific operational requirements and enhance overall productivity.