

What is a Borax Granular Material Pneumatic Conveying Equipment? And What Are Its Design Principles?
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling borax granular materials. This article explores the fundamental aspects of such equipment, including its operational principles and key design considerations.
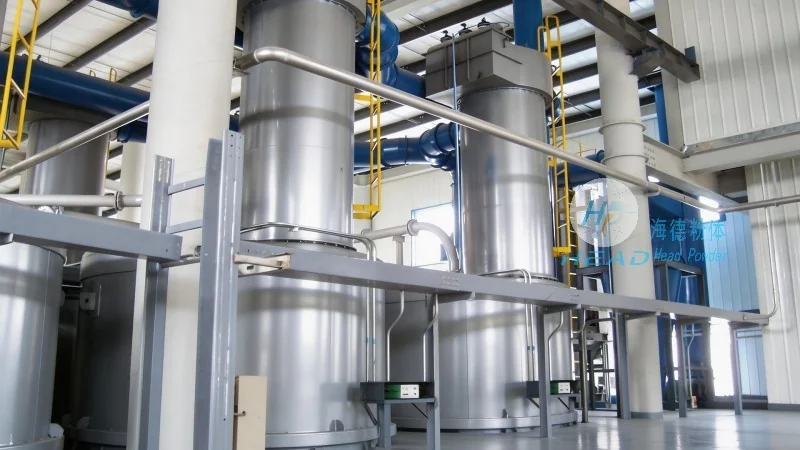
Introduction to Borax Granular Material Pneumatic Conveying Equipment
Borax granular material pneumatic conveying equipment is a specialized system engineered to transport borax particles through a pipeline using compressed air or other gas streams. This technology is widely adopted in industries where efficient, dust-free, and continuous material handling is essential. The equipment is designed to address the unique challenges associated with borax, such as its fine particle size, hygroscopic nature, and the need for controlled flow rates to prevent clogging or degradation.
Core Design Principles of Pneumatic Conveying Systems
The design of borax granular material pneumatic conveying equipment is built upon several critical principles to ensure optimal performance and reliability. The primary principle is the creation of a consistent air flow that can effectively lift and transport the material. This involves selecting appropriate air velocities and pressure levels to match the particle characteristics of borax. The system typically includes a feed hopper, a venturi or eductor, and a receiver or discharge unit. The feed hopper ensures a steady supply of borax granules, while the venturi or eductor generates the necessary airflow to move the particles. The receiver collects the conveyed material and may include features like cyclones or filters to separate any entrained air and prevent dust emissions.

Key Components and Their Functions
Several key components are integral to the functionality of borax granular material pneumatic conveying equipment. The feed hopper is designed to store and meter the borax granules, often equipped with a rotary valve or screw feeder to control the flow rate. The venturi or eductor is the heart of the system, converting the energy of the compressed air into the kinetic energy required to transport the particles. This component typically consists of a converging and diverging nozzle that accelerates the air flow, creating a low-pressure zone that draws in the material. The receiver or discharge unit is responsible for collecting the conveyed borax and may include a dust collection system to maintain environmental compliance. Additionally, the system may incorporate pressure relief valves, air filters, and moisture control mechanisms to ensure safe and efficient operation.
Advantages of Using Pneumatic Conveying for Borax Handling
Employing pneumatic conveying systems for borax granular material handling offers numerous advantages over traditional methods like belt conveyors or bucket elevators. One of the most significant benefits is the ability to achieve dust-free and enclosed transport, which reduces health hazards and environmental contamination. The system also provides flexibility in terms of layout, as it can be installed in various configurations to suit the plant's space constraints. Furthermore, pneumatic conveying allows for precise control over the flow rate and pressure, ensuring consistent material delivery to downstream processes. This control is particularly important in applications where borax is used as a raw material in chemical or pharmaceutical manufacturing, where uniformity is critical. Additionally, the system can handle a wide range of particle sizes and moisture contents, making it adaptable to different production requirements.
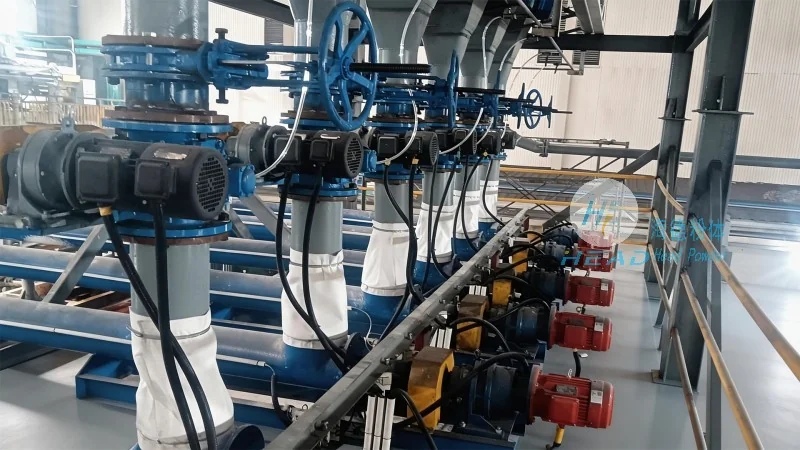
Customization and Application Considerations
HeadPowder, as a manufacturer based in Shandong, China, offers customized pneumatic conveying solutions tailored to the specific needs of borax handling applications. The company considers factors such as the particle size distribution, bulk density, and moisture content of the borax to design an optimal system. For instance, if the borax is highly hygroscopic, the system may include moisture control features like desiccant filters or heated lines to prevent clumping. Similarly, if the plant has limited space, the manufacturer may propose compact or vertical conveying systems. The design process also involves evaluating the operating conditions, such as the required conveying distance and the desired throughput, to select the appropriate air velocity and pressure. HeadPowder's expertise in material handling ensures that the final system meets the performance, safety, and efficiency standards required by the borax industry.
Conclusion
Borax granular material pneumatic conveying equipment, designed with advanced principles and components, provides an efficient and reliable solution for handling borax in various industrial applications. The system's ability to transport material in a dust-free environment, combined with precise control over flow rates, makes it a preferred choice for manufacturers. HeadPowder, with its roots in Shandong, China, continues to innovate and provide customized solutions that meet the evolving needs of the borax industry, ensuring optimal performance and operational safety.