

What is an Intelligent Bulk Material Pneumatic Conveying System? What are its Design Principles?
Intelligent bulk material pneumatic conveying systems represent a sophisticated solution for the efficient and reliable transport of powders, granules, and other bulk materials in industrial settings. These systems leverage advanced technology to optimize material handling processes, ensuring minimal product degradation, consistent flow rates, and enhanced operational safety. As a key component in modern manufacturing and processing industries, such systems are crucial for improving productivity and maintaining product quality.

About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of bulk material handling equipment, specializes in the design, development, and production of intelligent pneumatic conveying systems. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner for businesses seeking reliable and efficient material transport solutions. HeadPowder's products are engineered to meet the diverse needs of various industries, including food, pharmaceuticals, chemicals, and minerals, offering tailored solutions that enhance operational efficiency and reduce downtime.
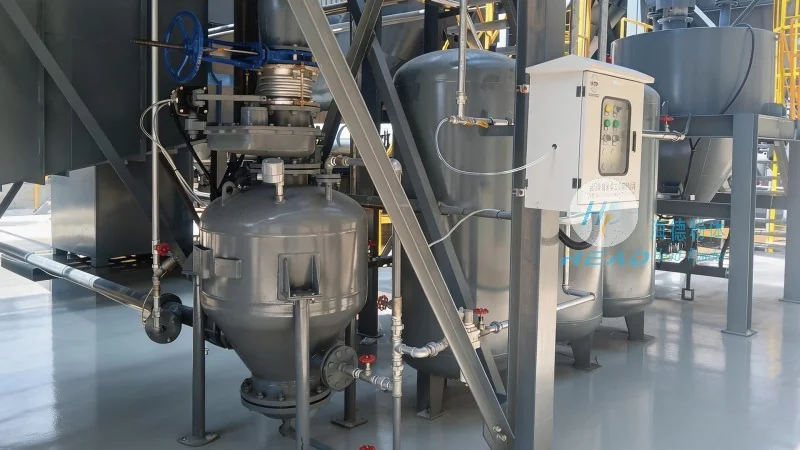
Key Features of Intelligent Pneumatic Conveying Systems
Intelligent bulk material pneumatic conveying systems are equipped with advanced features that set them apart from traditional conveying methods. These systems utilize intelligent control technologies, such as real-time monitoring and automated adjustments, to maintain optimal performance under varying operating conditions. The integration of sensors and data analytics enables precise control over material flow, pressure, and temperature, ensuring consistent and reliable transport. Additionally, these systems often incorporate energy-efficient designs, reducing operational costs while minimizing environmental impact. The user-friendly interface allows operators to easily monitor and adjust system parameters, enhancing overall operational flexibility.
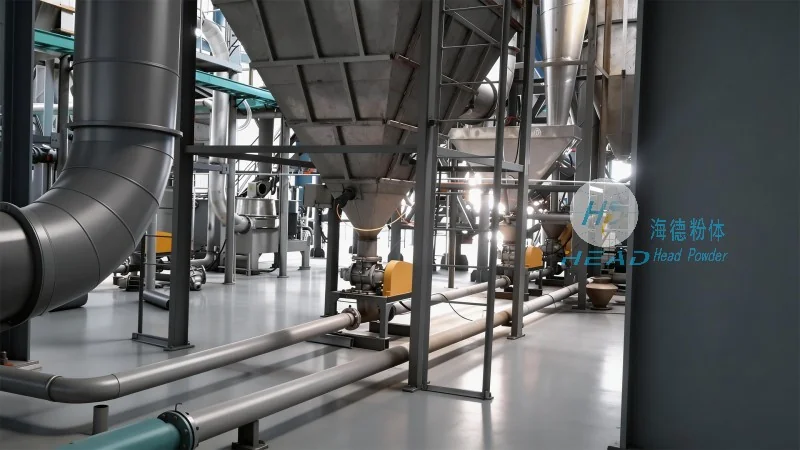
Design Principles of Pneumatic Conveying Systems
The design of intelligent pneumatic conveying systems is based on fundamental principles of fluid dynamics and material handling. The primary design principle is to create a pressure differential between the material source and the destination, using air or other gases to transport the bulk material. The system typically consists of a hopper, a conveyor line, and a receiver, with additional components like filters, cyclones, and control valves to ensure efficient and clean operation. The choice of conveying method—such as positive pressure, negative pressure, or hybrid systems—depends on the material characteristics, such as particle size, density, and moisture content. Advanced design incorporates computational fluid dynamics (CFD) simulations to optimize the system layout, ensuring minimal pressure drop and maximum material throughput. This approach minimizes energy consumption and maximizes the system's efficiency.
Applications and Benefits
Intelligent bulk material pneumatic conveying systems find applications in a wide range of industries, including food processing, pharmaceutical manufacturing, chemical production, and mining. In the food industry, these systems are used to transport ingredients like flour, sugar, and spices, ensuring hygienic and contamination-free handling. In pharmaceuticals, the systems are designed to meet stringent regulatory requirements, with features like aseptic conveying and particle size control. The benefits of using intelligent pneumatic conveying systems include improved product quality, reduced labor costs, enhanced safety, and increased production efficiency. By minimizing material degradation and maintaining consistent flow rates, these systems help businesses maintain high standards of quality and compliance.
Conclusion
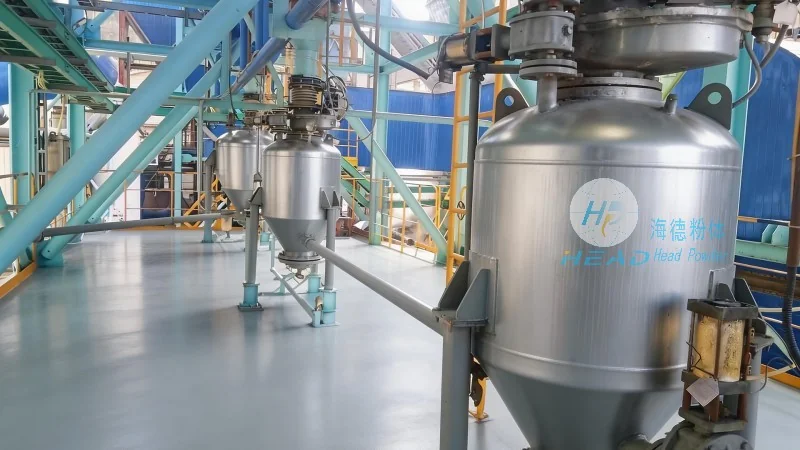
Intelligent bulk material pneumatic conveying systems, designed by Shandong HeadPowder Engineering Co., Ltd., offer a reliable and efficient solution for bulk material transport in various industrial applications. With advanced design principles and intelligent control features, these systems enhance operational performance, reduce costs, and improve product quality. As a leading manufacturer, HeadPowder continues to innovate and provide tailored solutions that meet the evolving needs of the industry, ensuring sustainable and efficient material handling for years to come.