

What is an Automatic Quantitative Powder Material Pneumatic Conveying System? And What Are Its Desig
When it comes to the efficient and precise handling of powder materials in industrial settings, the automatic quantitative powder material pneumatic conveying system stands out as a sophisticated solution. This system is engineered to transport bulk powders through a pressurized or vacuum pipeline, ensuring accurate and controlled delivery of material from the source to the destination. The core of this technology lies in its ability to automate the measurement and transport of powders, eliminating manual intervention and reducing the risk of human error. As a key component in modern material handling, understanding the functionality and design principles of such a system is crucial for optimizing industrial processes.
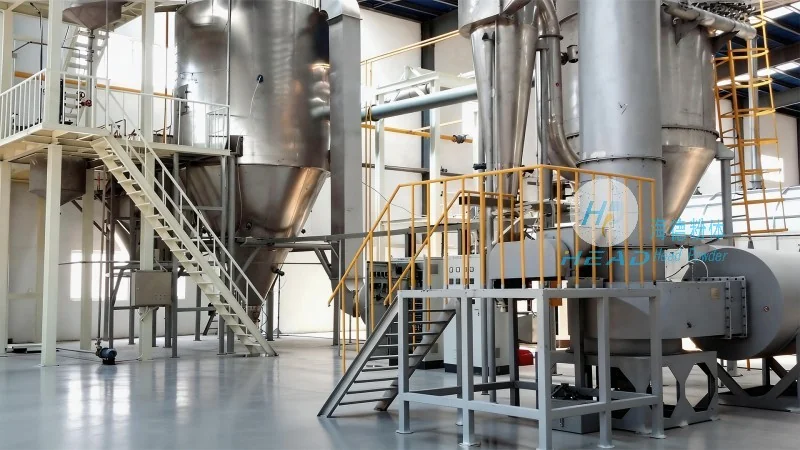
About HeadPowder: Your Trusted Partner in Powder Handling Solutions
HeadPowder, a leading name in the field of powder engineering, is dedicated to providing innovative and reliable solutions for the material handling industry. Based in Shandong, China, the company has established itself as a prominent manufacturer and supplier of advanced powder processing equipment. With a strong commitment to quality and customer satisfaction, HeadPowder leverages years of expertise to develop systems that meet the diverse needs of various industries, including pharmaceuticals, food processing, chemicals, and more. The company’s focus on research and development ensures that its products are at the forefront of technological advancements, offering enhanced performance and operational efficiency.
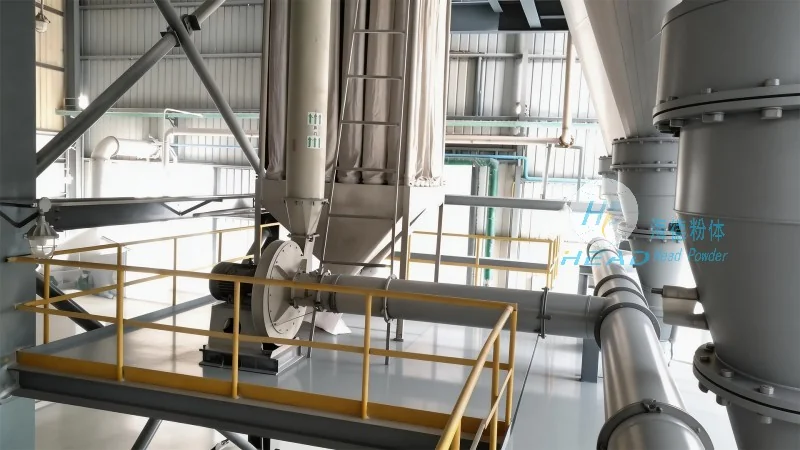
The Design Principles of the Automatic Quantitative Pneumatic Conveying System
The automatic quantitative powder material pneumatic conveying system operates on the fundamental principles of pneumatic transport, combining the mechanics of air flow with precise measurement technology. At its core, the system utilizes a pressurized air or vacuum source to move powder particles through a pipeline. The design incorporates several critical components, including a material hopper, a feeder, a conveying line, and a receiving hopper. The feeder is the key element for quantitative control, typically employing a rotary valve or a gravimetric feeder that can be calibrated to deliver a specific mass of powder per cycle. This ensures that the material is conveyed in precise quantities, meeting the exact requirements of downstream processes. The conveying line is designed to minimize particle degradation and maintain the integrity of the powder, with features such as smooth internal surfaces and appropriate pipe diameters. Additionally, the system may include a control panel that monitors and adjusts the air pressure, flow rate, and feeder speed in real-time, ensuring consistent performance and preventing system failures.
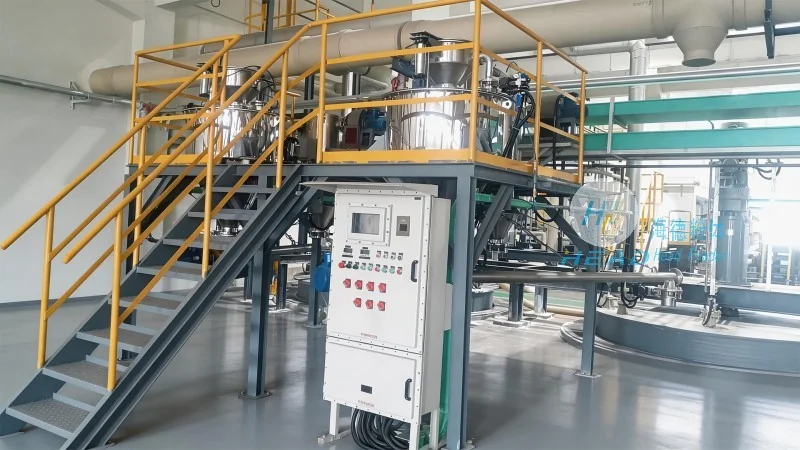
Key Advantages of the Automatic Quantitative Pneumatic Conveying System
Implementing an automatic quantitative powder material pneumatic conveying system offers numerous benefits for industrial operations. Firstly, it significantly enhances the accuracy and consistency of material delivery, reducing variations that can occur with manual handling. This precision is particularly critical in applications where exact dosing is required, such as in pharmaceutical manufacturing or food processing, where product quality and safety are paramount. Secondly, the system improves operational efficiency by automating the entire conveying process, minimizing downtime and labor costs. Unlike traditional methods that rely on manual scooping or bagging, the automated system can operate continuously, ensuring a steady flow of material. Thirdly, the pneumatic conveying method is inherently safer and more hygienic compared to other bulk handling techniques. It eliminates the need for manual handling of powders, reducing the risk of dust exposure and cross-contamination. Furthermore, the system is designed to be compact and space-efficient, making it suitable for facilities with limited floor space. The integration of advanced control systems also allows for remote monitoring and maintenance, further enhancing operational flexibility and reducing maintenance costs.
Applications and Industries Benefiting from the System
The automatic quantitative powder material pneumatic conveying system is versatile and can be applied across a wide range of industries. In the pharmaceutical industry, it is used for the transport of active pharmaceutical ingredients (APIs) and excipients, ensuring precise dosing and maintaining product purity. The food processing sector benefits from its ability to handle food-grade powders, such as sugar, flour, and spices, while maintaining hygiene standards. The chemical industry utilizes the system for transporting various chemical powders, including pigments, polymers, and catalysts, where accurate measurement and control are essential for process consistency. Additionally, in the agricultural and mining sectors, the system can be employed for the handling of bulk materials like fertilizers, minerals, and ores. The adaptability of the system to different powder types and industries makes it a valuable asset for any organization seeking to optimize its material handling processes.
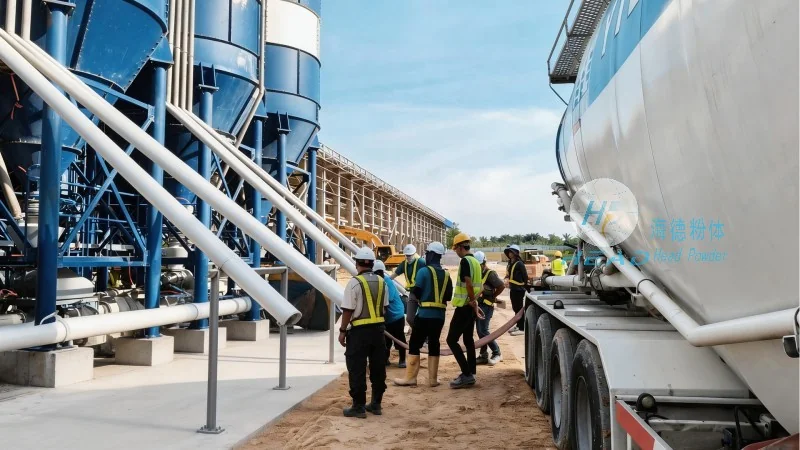
Conclusion: The Future of Powder Handling with HeadPowder
As industries continue to demand higher efficiency and precision in material handling, the automatic quantitative powder material pneumatic conveying system remains a vital solution. HeadPowder, with its expertise and commitment to innovation, provides cutting-edge systems that meet these evolving needs. By understanding the design principles and advantages of such a system, businesses can enhance their operational capabilities, reduce costs, and improve product quality. The integration of advanced technology and reliable engineering in HeadPowder’s systems ensures that they are not only effective but also durable and easy to maintain. For organizations looking to streamline their powder handling processes, the automatic quantitative pneumatic conveying system from HeadPowder is a reliable choice that delivers consistent performance and long-term value.