

What is a Sugar Material Handling System? What are the Design Principles?
For industries dealing with sugar processing, the efficiency and reliability of material handling systems are paramount. A sugar material handling system is a specialized setup designed to transport, store, and manage sugar in a manner that ensures optimal performance, safety, and product quality. This system integrates various components such as conveyors, elevators, and storage silos, all working in tandem to streamline the entire process from raw sugar reception to final packaging. Understanding the design principles behind these systems is crucial for optimizing operations and maintaining high standards in the sugar industry.
Understanding the Core Components of a Sugar Material Handling System
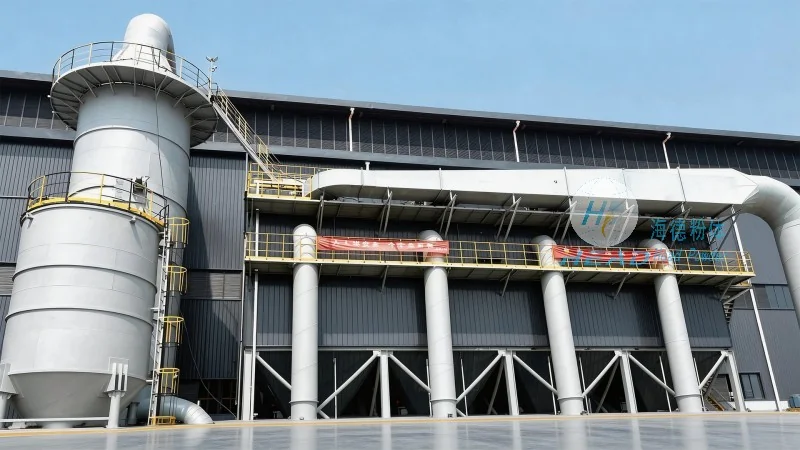
The foundation of any effective sugar material handling system lies in its core components. These typically include bulk material conveyors, which are essential for moving large quantities of sugar from one location to another. Common types include belt conveyors, screw conveyors, and bucket elevators, each tailored to specific operational needs. Storage silos or hoppers are another critical element, providing a secure and controlled environment for storing sugar, preventing contamination and ensuring consistent supply. Additionally, material handling equipment like feeders and classifiers may be integrated to regulate the flow and quality of the sugar being processed. Each component must be carefully selected and configured to handle the unique characteristics of sugar, such as its granular structure and potential for moisture absorption.
Design Principles for Efficient Sugar Material Handling
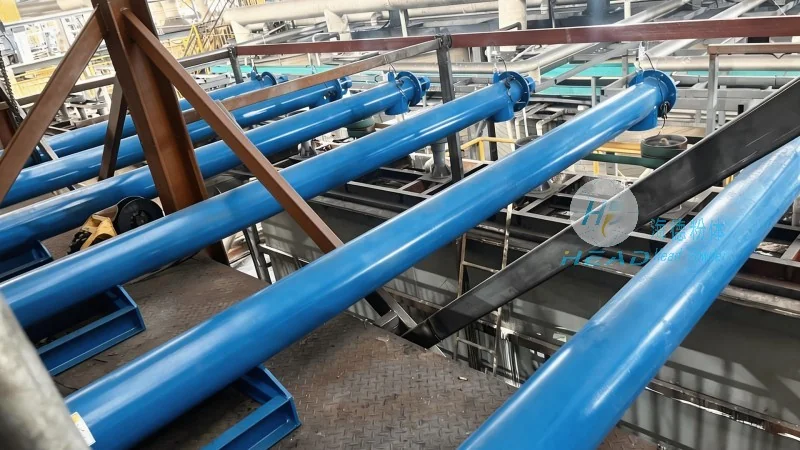
Designing an efficient sugar material handling system involves adhering to several key principles that enhance performance and durability. First, the system must prioritize minimal product degradation. Sugar is sensitive to moisture, temperature fluctuations, and physical damage, so the design must incorporate features like moisture-proof enclosures, temperature control mechanisms, and gentle handling equipment to preserve product quality. Second, energy efficiency is a critical consideration. Modern systems often utilize energy-saving technologies, such as variable speed drives and optimized conveyor systems, to reduce operational costs while maintaining throughput. Third, safety is paramount. The system should include safety features like emergency stop buttons, protective guards, and proper ventilation to prevent accidents and ensure compliance with industry regulations. Finally, scalability and adaptability are important. As production needs evolve, the system should be designed to accommodate future expansions or changes in processing requirements without requiring a complete overhaul.
HeadPowder's Expertise in Sugar Material Handling Solutions
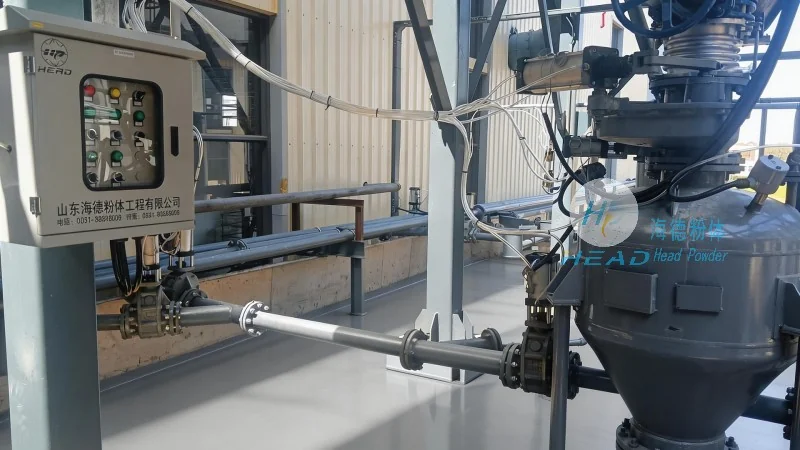
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial engineering solutions, specializes in designing and manufacturing tailored sugar material handling systems. With years of experience in the industry, HeadPowder understands the unique challenges faced by sugar processing facilities and offers customized solutions that meet specific operational demands. The company’s team of engineers leverages advanced design principles and cutting-edge technology to create systems that are not only efficient but also durable and cost-effective. HeadPowder’s commitment to quality and customer satisfaction is evident in its rigorous testing and quality control processes, ensuring that every system delivered meets the highest standards. The company’s headquarters is located in Shandong, China, where it continues to innovate and serve clients worldwide with reliable and efficient sugar material handling solutions.
Conclusion
In conclusion, a well-designed sugar material handling system is essential for the smooth operation of sugar processing facilities. By adhering to key design principles such as product preservation, energy efficiency, safety, and scalability, these systems can significantly enhance operational performance and product quality. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing expert solutions that address the specific needs of the sugar industry, ensuring that facilities can operate at peak efficiency while maintaining the highest standards of safety and quality.