

What is a Coffee Material Handling System? And What Are Its Design Principles?
Coffee material handling systems are essential components in the coffee processing industry, designed to efficiently transport, sort, and store coffee-related materials throughout the production process. From raw coffee beans to finished roasted products, these systems streamline operations, enhance productivity, and ensure consistent quality. Understanding the core functions and design principles of such systems is crucial for coffee businesses aiming to optimize their workflow and meet growing market demands.
Introduction to Coffee Material Handling Systems
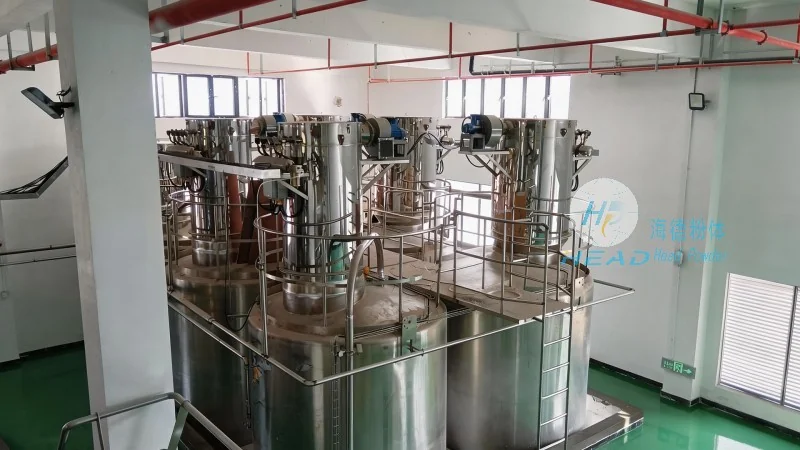
Coffee material handling systems encompass a range of equipment and processes used to manage coffee materials from the initial stage of raw bean reception to the final packaging of roasted coffee. These systems play a pivotal role in modern coffee processing, as they help reduce manual labor, minimize handling errors, and maintain the integrity of the coffee beans. By automating the movement of materials, businesses can achieve higher throughput, lower operational costs, and improved overall efficiency. The design and implementation of these systems are tailored to the specific needs of each coffee processing facility, whether it's a small-scale roastery or a large industrial processing plant.
Understanding the Core Components of a Coffee Material Handling System
The effectiveness of a coffee material handling system relies on its key components, each serving a distinct purpose in the material flow. Common components include conveyor belts, elevators, sorters, storage silos, and processing units. Conveyor belts, often made of durable materials like rubber or plastic, transport coffee beans and other materials horizontally or at slight inclines. Elevators, such as bucket elevators or screw conveyors, lift materials vertically, enabling vertical movement within the facility. Sorting equipment, like vibrating screens or air classifiers, separate coffee beans based on size, shape, or density, ensuring only high-quality beans proceed to the next stage. Storage silos or bins are used to store raw or processed coffee, providing controlled environments to maintain freshness and prevent contamination.
Design Principles for Efficient Coffee Material Handling
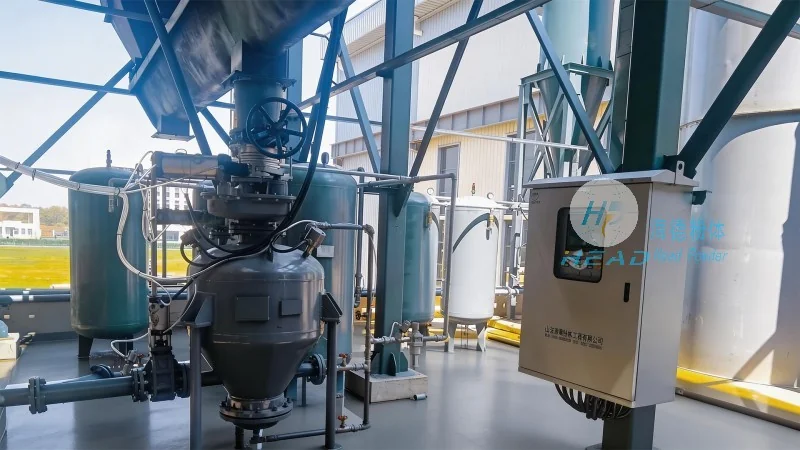
The design of a coffee material handling system follows several critical principles to ensure optimal performance and longevity. First, the system must be tailored to the physical characteristics of the coffee materials being handled. For instance, the size, density, and moisture content of raw coffee beans affect the choice of conveyor type and speed. Second, the system should be designed for high throughput while minimizing energy consumption. This involves selecting efficient motors, optimizing conveyor speeds, and reducing unnecessary stops or starts. Third, space constraints and facility layout are crucial considerations. A well-designed system maximizes the use of available space without compromising material flow. Fourth, ease of maintenance and cleaning is essential, as coffee processing environments require regular sanitation to prevent spoilage or contamination. Finally, the system should be scalable, allowing for future expansion as the business grows.
The Role of HeadPowder in Coffee Processing Solutions
HeadPowder, a leading manufacturer of coffee processing equipment, specializes in designing and manufacturing customized coffee material handling systems. With its headquarters in Shandong, China, HeadPowder Engineering Co., Ltd. leverages years of industry experience to develop solutions that meet the unique needs of coffee businesses worldwide. The company’s team of engineers and technicians works closely with clients to understand their specific requirements, from raw bean reception to final packaging, and designs systems that enhance efficiency and productivity. HeadPowder’s commitment to quality and innovation has made it a trusted partner for coffee processors seeking reliable and efficient material handling solutions.
Key Features and Benefits of Our Coffee Material Handling Systems
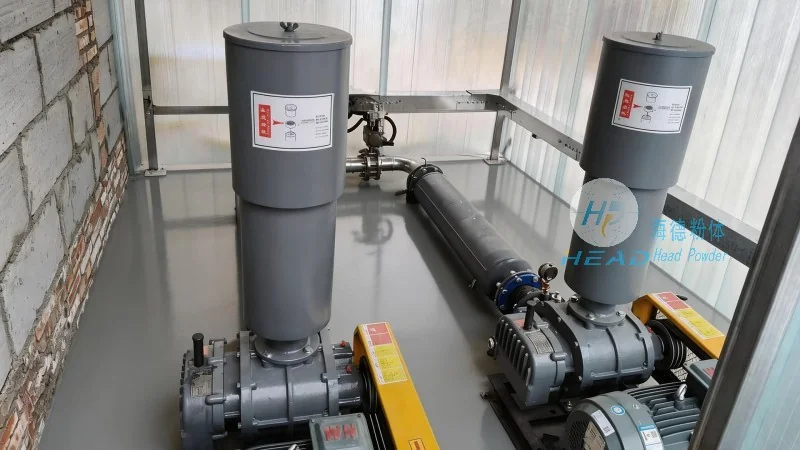
HeadPowder’s coffee material handling systems are equipped with several key features that contribute to their effectiveness and durability. These systems utilize advanced materials, such as food-grade stainless steel, to ensure compliance with industry standards and maintain the quality of the coffee. The conveyor systems are designed with smooth, non-stick surfaces to prevent coffee beans from sticking or damaging the equipment. Additionally, the systems incorporate automated controls, allowing for precise speed adjustments and monitoring of material flow. The sorters and elevators are engineered for high efficiency, with minimal downtime and easy maintenance. The benefits of implementing these systems include increased production capacity, reduced labor costs, improved product quality, and enhanced safety in the workplace. By streamlining the material handling process, businesses can focus on core activities, such as roasting and quality control, while leaving the logistics to the system.
Application Examples and Real-World Use Cases
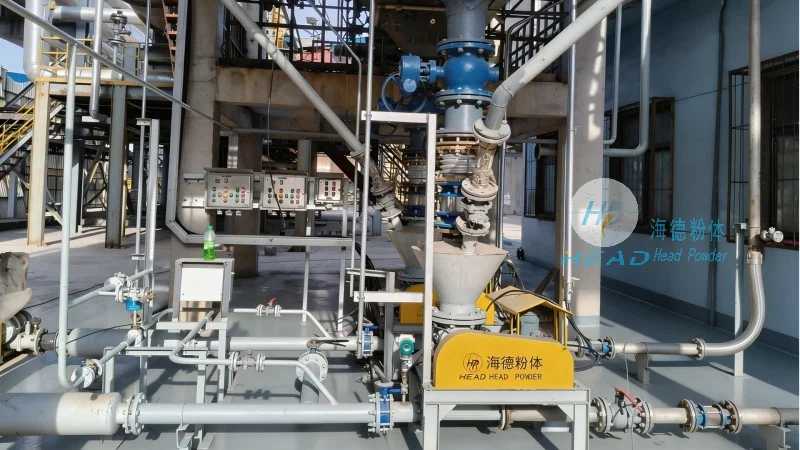
HeadPowder’s coffee material handling systems have been successfully implemented in various coffee processing facilities, demonstrating their versatility and effectiveness. For example, a small coffee roastery in the United States used a customized conveyor system to transport raw coffee beans from the reception area to the roasting machine. The system included a vibrating screen to remove foreign objects and a storage silo to hold the roasted beans until packaging. The result was a significant reduction in manual handling time and an increase in throughput by 30%. In another case, a large coffee processing plant in Brazil installed a multi-level elevator system to move coffee beans between different floors of the facility. The system’s ability to handle large volumes and maintain consistent speed ensured smooth operations during peak production periods. These examples highlight the adaptability of HeadPowder’s systems to different scales and operational needs, making them suitable for a wide range of coffee businesses.
Conclusion and Contact Information
Coffee material handling systems are indispensable tools for modern coffee processing, enabling businesses to achieve higher efficiency, lower costs, and improved product quality. The design principles and components of these systems are carefully selected to meet the specific requirements of each facility, ensuring optimal performance and longevity. HeadPowder Engineering Co., Ltd., based in Shandong, China, offers customized coffee material handling solutions that are tailored to the unique needs of coffee processors. With its commitment to quality, innovation, and customer satisfaction, HeadPowder is a reliable partner for businesses seeking to enhance their material handling processes. For more information or to discuss your specific coffee processing needs, please contact HeadPowder at its headquarters in Shandong, China.