

What is a Pneumatic Pulse Powder Conveyor? What is its Design Principle?
A pneumatic pulse powder conveyor is a specialized industrial equipment designed to transport bulk solid materials, such as powders, granules, and fine particles, through a pipeline using compressed air. This technology offers a flexible and efficient solution for moving materials over long distances or within complex layouts, making it a popular choice in various manufacturing and processing industries. The system operates by creating a series of high-pressure air pulses that propel the material forward, ensuring reliable and consistent delivery without the need for mechanical parts that might wear out or get clogged.
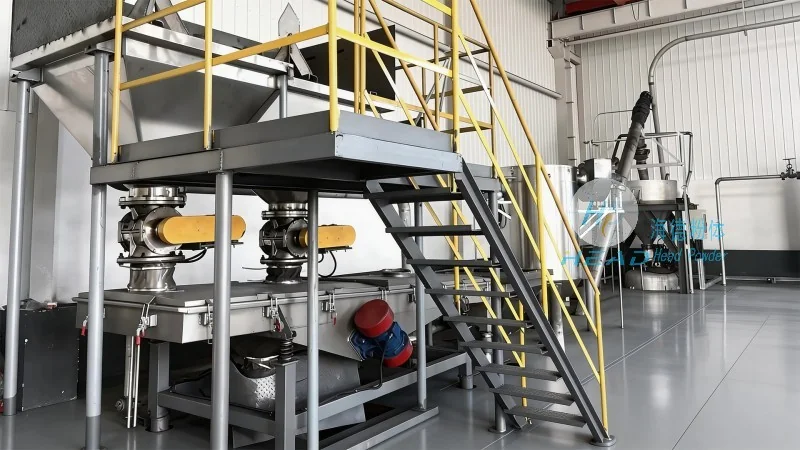
Understanding the Core Function of a Pulse Powder Conveyor
The primary function of a pulse powder conveyor is to transfer bulk materials from a source, like a hopper or silo, to a destination, such as a processing unit or storage tank. Unlike traditional mechanical conveyors, which rely on rotating parts or belts, a pulse conveyor uses compressed air to create a "push" effect, allowing it to handle a wide range of materials, including those that are abrasive, sticky, or prone to bridging. This makes it ideal for applications where traditional methods may fail due to material characteristics or operational constraints.
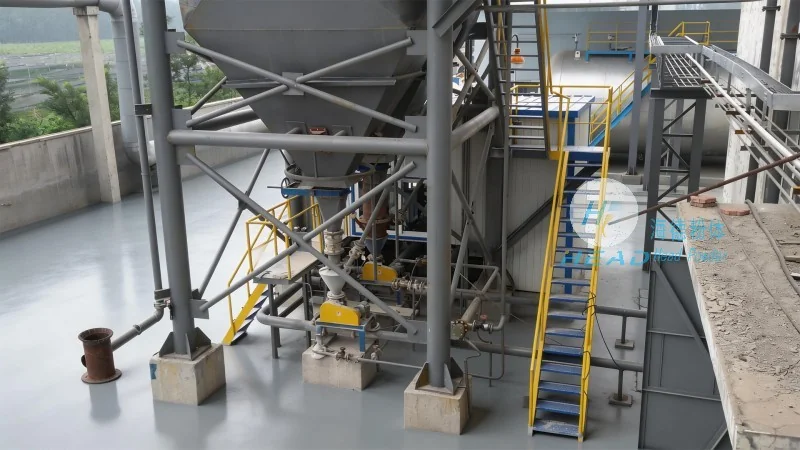
The Design Principle Behind Pneumatic Pulse Conveying Systems
The design principle of a pneumatic pulse powder conveyor is based on the Venturi effect and the principles of fluid dynamics. The system consists of a pipeline with a series of pulse valves that are activated by a control unit. When a pulse is generated, compressed air is introduced into the pipeline, creating a high-velocity airflow that draws the material from the hopper into the pipeline. The air then carries the material forward, and as the air pressure drops, the material is deposited at the discharge point. The cycle repeats, allowing for continuous material flow. The key to the system's efficiency lies in the precise control of the pulse frequency and pressure, which can be adjusted to match the specific characteristics of the material being conveyed.
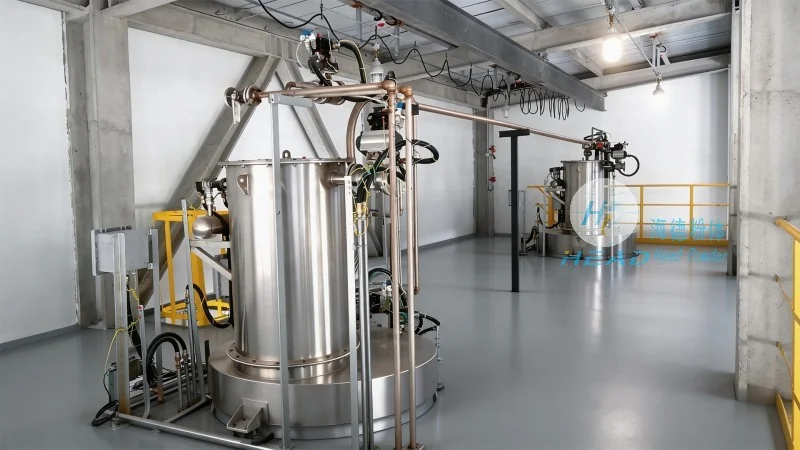
Key Components and Their Roles in the System
Several critical components work together to ensure the smooth operation of a pneumatic pulse powder conveyor. The main components include the hopper or feed bin, which holds the material; the pipeline, which transports the material; the pulse valves, which generate the air pulses; the control unit, which regulates the pulse frequency and pressure; and the discharge device, which releases the material at the end of the pipeline. Each component plays a vital role in maintaining the system's performance. For example, the hopper design must prevent material bridging or clogging, while the pulse valves must be durable and able to handle the pressure and material characteristics. The control unit ensures that the pulses are timed correctly to maximize material movement and minimize air consumption.
Applications and Industries Where Pulse Conveyors Excel
Pneumatic pulse conveyors are widely used in various industries due to their versatility and ability to handle diverse materials. Some common applications include pharmaceutical manufacturing, where the system can transport sensitive powders without contamination; food processing, where it can handle ingredients like flour or sugar; and chemical processing, where it can move abrasive or corrosive materials. In addition, the system is used in mining and mineral processing to transport ore and other bulk materials from processing plants to storage facilities. The flexibility of the pulse conveyor allows it to adapt to different layouts and distances, making it a cost-effective solution for many industrial needs.
About HeadPowder: Your Trusted Partner in Powder Handling Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of advanced powder handling equipment, including pneumatic pulse conveyors. With years of experience in the industry, HeadPowder has developed a reputation for producing high-quality, reliable, and efficient equipment that meets the needs of its customers. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses in various industries. HeadPowder's products are designed to handle a wide range of materials and applications, ensuring that customers can find a solution that fits their specific requirements. The company's headquarters is located in Shandong, China, where it has a team of skilled engineers and technicians dedicated to developing and manufacturing top-tier powder handling solutions.