

What is a Calcium Carbonate Powder Pneumatic Conveying System? And What Are Its Design Principles?
Calcium carbonate powder, a widely used industrial material, often requires efficient and reliable transportation methods to move it from one location to another. The calcium carbonate powder pneumatic conveying system offers a solution to this challenge, leveraging air pressure to transport the fine powder through a network of pipes and components. This article explores the fundamental aspects of such systems, including their design principles and practical applications.
Introduction to Calcium Carbonate Powder Pneumatic Conveying Systems
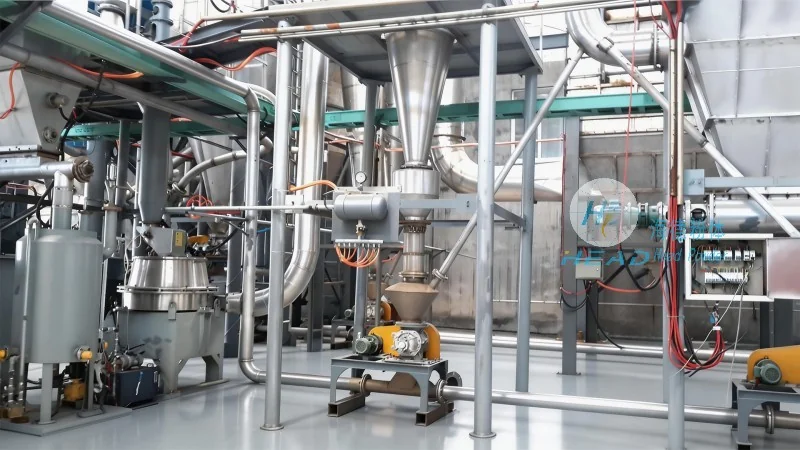
The calcium carbonate powder pneumatic conveying system is a specialized industrial equipment designed to transport calcium carbonate powder, which is commonly used in industries like paper, plastics, and construction. Unlike traditional methods like belt conveyors or bucket elevators, pneumatic conveying systems use compressed air to move the material, making them ideal for handling fine powders that are prone to dust and clogging. The system typically consists of a blower, a hopper for material storage, a pipeline network, and a receiver for the delivered material. This method not only ensures a dust-free operation but also allows for the safe and efficient transfer of the powder over long distances.
Key Components and Their Functions
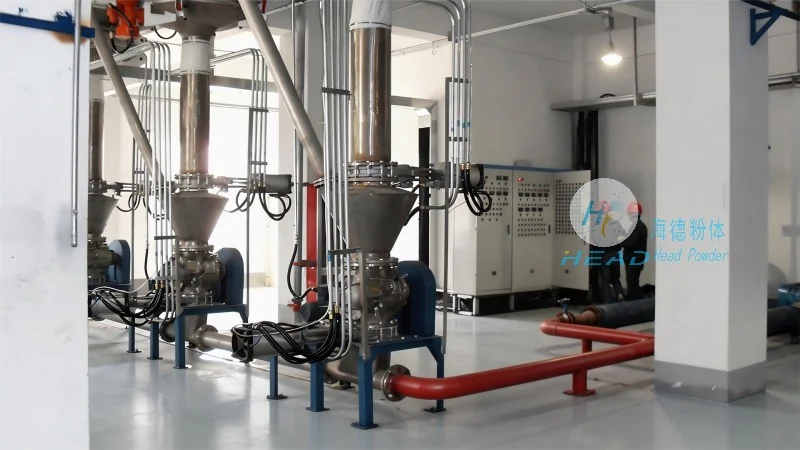
At the heart of a calcium carbonate powder pneumatic conveying system are several critical components that work in tandem to ensure smooth operation. The blower or air compressor provides the necessary air pressure to move the powder through the system. The hopper, often equipped with a feeder or a rotary valve, regulates the flow of calcium carbonate powder into the pipeline. The pipeline network, made of materials resistant to the powder's chemical properties, transports the material from the source to the destination. The receiver, usually a hopper or a storage tank, collects the delivered powder. Additionally, filters and cyclones may be included to separate any fine particles from the air, ensuring compliance with environmental regulations and maintaining system efficiency.
Design Principles for Efficient Material Handling
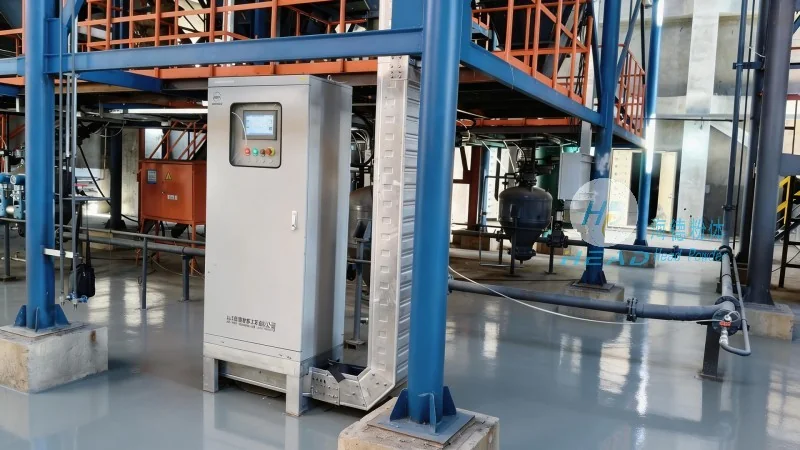
The design of a calcium carbonate powder pneumatic conveying system is guided by several key principles to maximize efficiency and minimize operational issues. One of the primary principles is maintaining consistent air velocity throughout the pipeline to prevent the powder from settling or clogging. The system's design must account for the specific properties of calcium carbonate powder, such as its particle size, density, and flowability. Proper sizing of the blower, pipeline diameter, and feeder is crucial to ensure that the air velocity remains within the optimal range for conveying the material. Another important principle is the use of appropriate materials for the pipeline and components to resist corrosion and abrasion caused by the powder. The system's layout should also minimize bends and changes in direction to reduce pressure losses and prevent particle degradation. Furthermore, the inclusion of safety features like pressure relief valves and dust collection systems is essential to protect the equipment and the environment.
Application Scenarios and Industry Benefits
Calcium carbonate powder pneumatic conveying systems are widely used in various industrial applications where the efficient handling of fine powders is critical. In the paper industry, these systems are used to transport calcium carbonate filler into paper machines, improving the paper's quality and brightness. In the plastics industry, they help in delivering calcium carbonate as a filler to extrusion lines, enhancing the mechanical properties of the final products. The construction industry also benefits from these systems when transporting calcium carbonate for use in cement and concrete production. The primary benefits of using pneumatic conveying systems include reduced labor costs, improved safety by eliminating manual handling of powders, and increased operational efficiency due to the continuous and automated nature of the process. Additionally, the systems help in maintaining a clean and dust-free environment, which is essential for both worker health and product quality.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
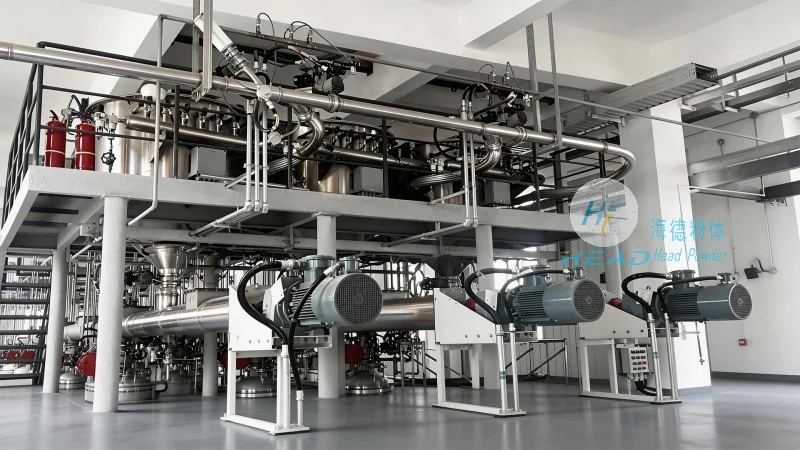
As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality calcium carbonate powder pneumatic conveying systems. With years of experience and a commitment to innovation, the company offers customized solutions tailored to the specific needs of its clients. The company's team of engineers and technicians works closely with clients to understand their operational requirements and develop systems that meet their efficiency and safety standards. HeadPowder's systems are known for their reliability, durability, and energy efficiency, making them a preferred choice for industries that demand consistent and high-performance material handling solutions. The company's headquarters is located in Shandong, China, where it continues to advance its technology and expand its market presence.